HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced conveying systems for sintered ash powder. This article provides an in-depth exploration of the working principles and operational characteristics of such systems, highlighting their relevance across various industrial applications.
Introduction to Sintered Ash Powder Conveying Systems
Sintered ash powder, a byproduct commonly generated in industrial processes like sintering, steel production, and power generation, requires efficient and reliable transportation to facilitate recycling or disposal. The sintered ash powder conveying system is engineered to handle these fine, often abrasive materials with precision, ensuring minimal loss and optimal performance. HeadPowder's expertise lies in developing customized solutions that address the unique challenges posed by sintered ash, such as high temperature exposure, variable particle size, and the need for dust control.
Working Principle of the Sintered Ash Powder Conveying System
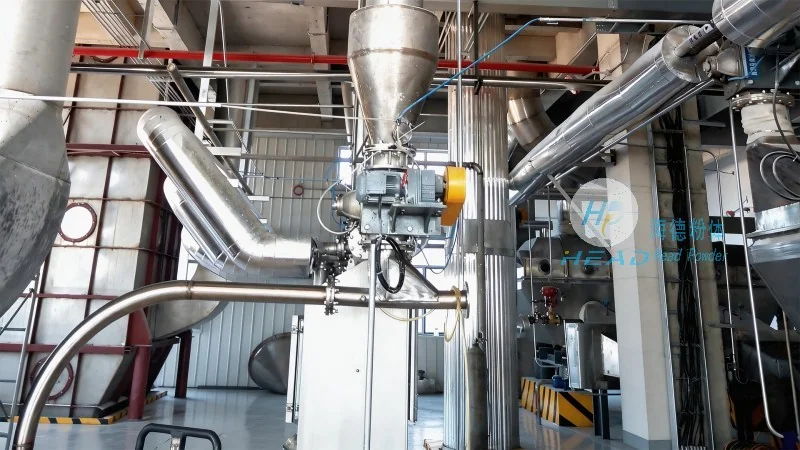
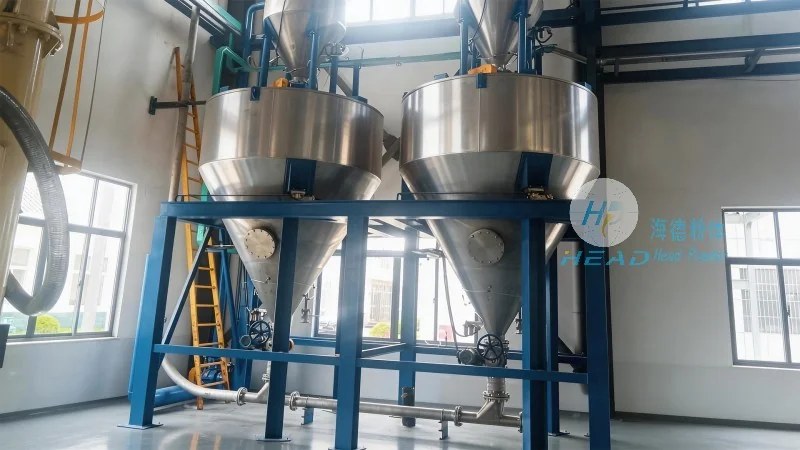
The core of the sintered ash powder conveying system is its ability to transport dry, fine powders through a network of pipes or channels. Typically, these systems employ a combination of mechanical and pneumatic technologies to achieve efficient material movement. For instance, a common configuration involves a hopper that collects the sintered ash, followed by a rotary valve or feeder that controls the flow rate. The material is then conveyed through a pipeline using either a positive displacement blower or a vacuum pump, depending on the system design. The system may also incorporate components like cyclones or filters to separate any entrained dust from the main flow, ensuring compliance with environmental regulations. HeadPowder's systems are designed with robust materials, such as stainless steel or high-grade alloys, to withstand the corrosive and abrasive nature of sintered ash, extending the equipment's service life.
Key Working Scene Characteristics
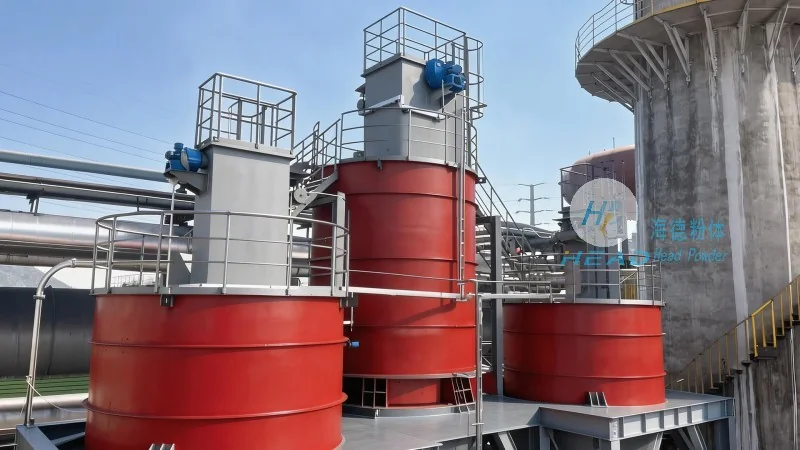
The operational characteristics of sintered ash powder conveying systems are tailored to meet the demands of diverse industrial environments. In steel mills, for example, the system must handle large volumes of ash from sintering machines, often at elevated temperatures. The design incorporates heat-resistant components and efficient cooling mechanisms to prevent equipment failure. In power plants, the system may need to manage ash from coal combustion, requiring high dust collection efficiency and low energy consumption. HeadPowder's systems are adaptable to these varying conditions, offering adjustable flow rates, pressure control, and automated monitoring to optimize performance. Additionally, the systems are engineered for minimal maintenance, with easy access to components for routine checks and repairs, reducing downtime and operational costs.
Application Scenarios and Operational Advantages
HeadPowder's sintered ash powder conveying systems are widely used in several key industries. In the metallurgical sector, they are essential for transporting ash from sintering processes, which is often recycled as a raw material in subsequent production stages. The systems enhance material recovery rates and reduce waste disposal costs. In the power generation industry, the equipment facilitates the efficient removal of fly ash, improving plant efficiency and reducing environmental impact. The systems also find applications in cement and chemical manufacturing, where fine powders need to be transported between processing units. The operational advantages of these systems include high conveying efficiency, low energy consumption, and compliance with stringent environmental standards. HeadPowder's commitment to quality and innovation ensures that their systems deliver consistent performance, meeting the specific needs of each client while adhering to industry best practices.
Technical Features and Performance Specifications
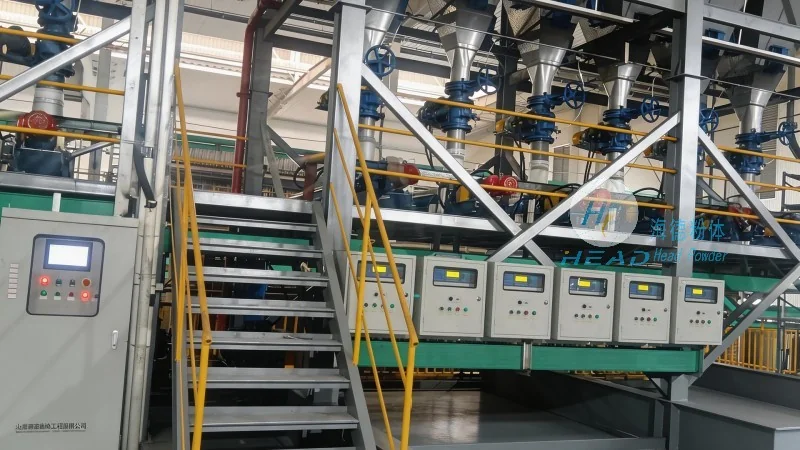
HeadPowder's sintered ash powder conveying systems are equipped with several technical features that enhance their functionality and reliability. These include variable speed drives for precise flow control, pressure sensors to monitor system performance, and automatic shut-off valves to prevent backflow or overpressure. The systems are designed with dust-tight seals and filtration systems to minimize emissions and protect the environment. The use of high-quality materials, such as wear-resistant liners and corrosion-resistant coatings, ensures that the equipment can handle the abrasive nature of sintered ash without degradation. Performance specifications typically include a conveying capacity ranging from several tons per hour to over 100 tons per hour, depending on the system configuration. The systems are also scalable, allowing for expansion as production needs grow. HeadPowder's engineering team works closely with clients to customize the system parameters, ensuring optimal performance and cost-effectiveness.
In conclusion, HeadPowder's sintered ash powder conveying systems represent a sophisticated solution for the efficient handling of industrial powders. By combining advanced engineering, robust materials, and tailored design, these systems address the unique challenges of sintered ash transportation while delivering reliable performance across various industrial applications. With a strong presence in Shandong, China, HeadPowder continues to provide high-quality, customized solutions that meet the evolving needs of the industry.




