Small bag powder conveyors are specialized equipment designed for the efficient handling and transportation of bulk powders from sealed bags. As a critical component in material processing industries, these systems play a vital role in ensuring smooth material flow and operational efficiency. The technology behind small bag powder conveyors combines mechanical, pneumatic, and sometimes hydraulic systems to automate the process of unloading, conveying, and transferring powders from bag to storage or processing units. This equipment is particularly valuable in sectors where handling fine or abrasive powders requires precision and minimal product loss.
The Working Principle of Small Bag Powder Conveyors
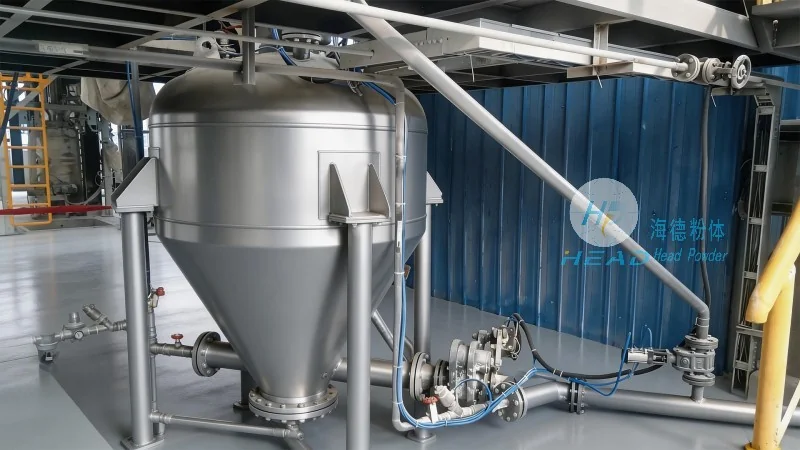
The core principle of small bag powder conveyors revolves around the controlled extraction of material from sealed bags using a combination of vacuum or pressure differentials. The system typically includes a hopper or receiving chamber that is connected to the bag via a discharge valve or opening mechanism. When the bag is positioned over the hopper, the conveyor activates, creating a vacuum or pressure gradient that draws the powder from the bag into the hopper. This process is often assisted by a rotary valve or screw conveyor that moves the material through the system. The design ensures that the powder is transferred without breaking the bag, maintaining product integrity and preventing contamination. The control system, which may include sensors and programmable logic controllers (PLCs), regulates the flow rate and ensures consistent operation, adapting to variations in bag size or material density.
Key Working Scene Characteristics and Applications
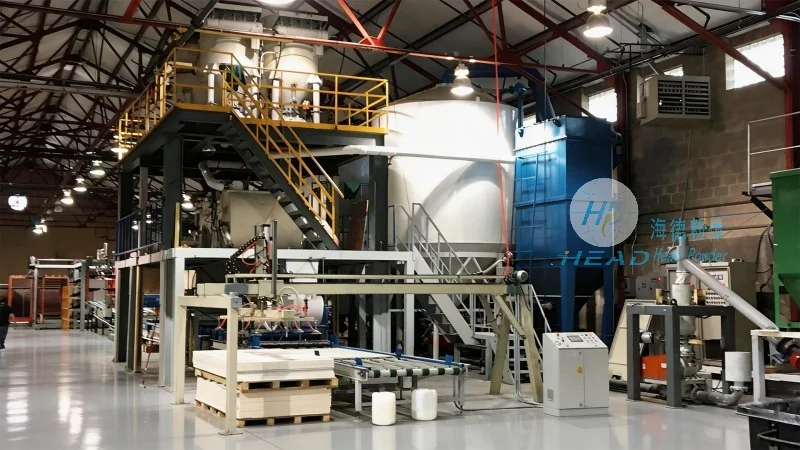
Small bag powder conveyors are widely utilized across various industries due to their adaptability and efficiency. In the pharmaceutical sector, these systems are essential for handling sensitive powders, where contamination and product degradation must be minimized. The enclosed design and sterile operation capabilities of such conveyors meet the stringent regulatory requirements of the pharmaceutical industry. Similarly, in the food processing industry, small bag powder conveyors are used to transport ingredients like flour, sugar, and spices, ensuring hygienic handling and maintaining product quality. The equipment is also prevalent in the chemical and agricultural sectors, where it facilitates the transfer of bulk chemicals, fertilizers, and agricultural powders. The working scene characteristics include high throughput, low maintenance, and the ability to handle a wide range of powder types, from fine powders to coarse granules. Additionally, these conveyors are designed for easy integration into existing production lines, reducing downtime and enhancing overall operational flexibility.
Advantages and Operational Benefits
Implementing small bag powder conveyors offers several advantages that contribute to improved productivity and cost savings. One of the primary benefits is the reduction in manual labor, as the system automates the entire unloading and conveying process. This not only increases efficiency but also minimizes the risk of human error and product exposure to contaminants. The enclosed design of the equipment ensures that powders are handled in a controlled environment, preventing dust dispersion and maintaining a clean workspace. Furthermore, the systems are designed for low energy consumption, making them environmentally friendly and cost-effective in the long run. The modular construction allows for easy maintenance and replacement of components, reducing downtime and extending the equipment's service life. The adaptability of small bag powder conveyors to different bag sizes and material types makes them a versatile solution for various industrial applications.
Conclusion and Company Information
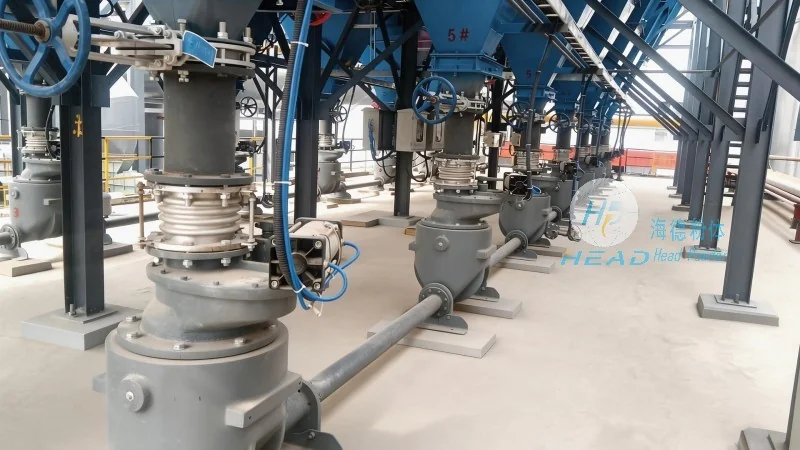
Small bag powder conveyors represent a sophisticated solution for the efficient handling of bulk powders, offering significant advantages in terms of operational efficiency, product integrity, and cost-effectiveness. The technology, as exemplified by the products from Shandong HeadPowder Engineering Co., Ltd., based in China, combines advanced engineering with practical design to meet the diverse needs of modern industries. By automating the material handling process, these systems enhance productivity while maintaining the highest standards of safety and hygiene. As industries continue to demand more efficient and reliable material handling solutions, small bag powder conveyors remain a critical component in ensuring smooth and sustainable operations.




