Working Principle and Features of Pneumatic Conveying Equipment for Cement Particle Materials
Release time:2026-09-18 09:38:48
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of pneumatic conveying equipment tailored for cement particle materials. This equipment is crucial for efficient material handling in cement production lines, ensuring smooth and reliable transport of cement powders from storage to processing units. The company's products are engineered to meet the specific demands of the cement industry, offering solutions that enhance productivity and operational efficiency.
Working Principle of Pneumatic Conveying Equipment for Cement Particles
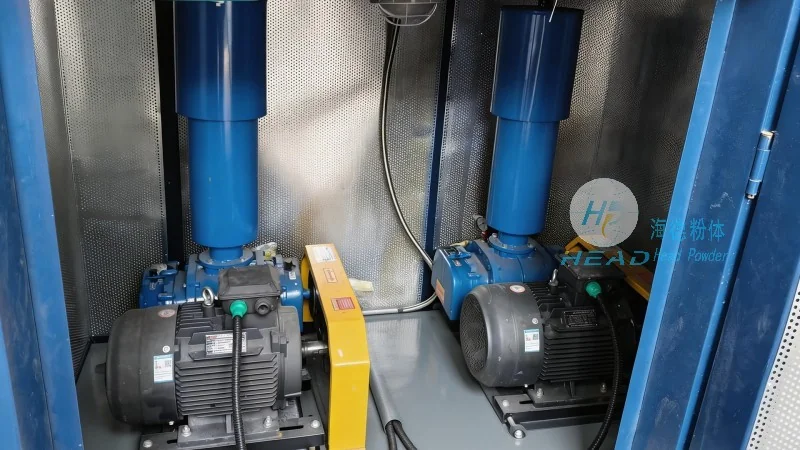
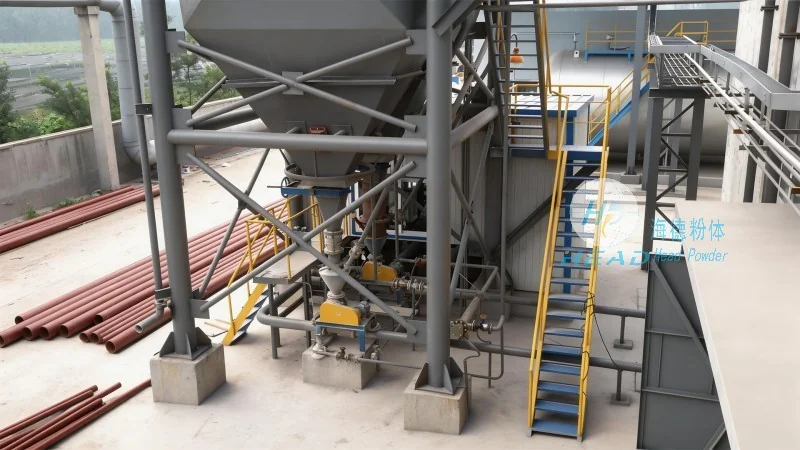
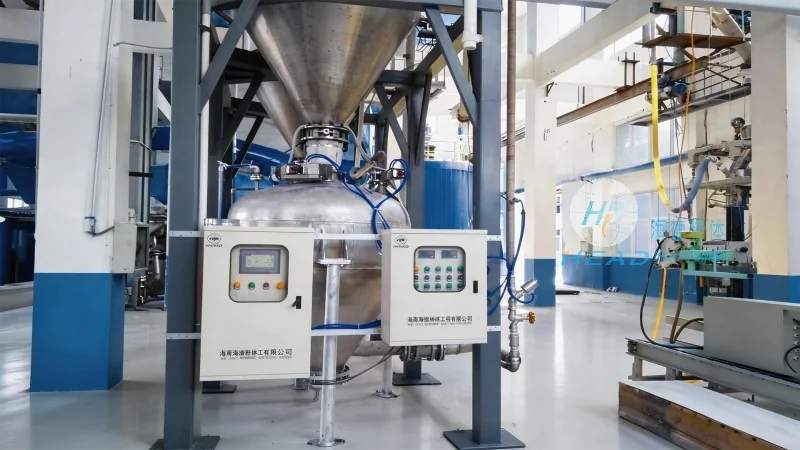
The pneumatic conveying system for cement particles operates by utilizing air as the medium to transport bulk materials. The process typically involves a series of components, including a hopper, a rotary valve, a conveying line, and a receiver. The cement particles are first fed into the hopper, where they are then discharged into the conveying line through the rotary valve. Compressed air is introduced into the line, creating a flow that propels the cement particles forward. The air and cement mixture travels through the pipeline until it reaches the receiver, where the cement is separated from the air and collected. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational efficiency. The system can be configured as either a suction-type or pressure-type setup, depending on the specific application requirements. In suction systems, air is drawn from the receiver to create a negative pressure that pulls the material through the line. In pressure systems, compressed air is supplied from a blower to push the material forward. Both configurations are effective for cement particle transport, with the choice depending on factors such as distance, elevation, and material characteristics.
Key Features of the Equipment
HeadPowder's pneumatic conveying equipment for cement particles offers several distinct advantages that enhance performance and reliability. First, the system provides a dust-free and hygienic transport environment, which is essential for maintaining product quality and compliance with industry standards. The enclosed design prevents dust contamination, making it suitable for applications where product purity is critical. Second, the equipment is highly flexible in terms of layout and can be customized to fit various plant configurations. This adaptability allows for easy integration into existing production lines without significant modifications. Third, the system operates with low energy consumption compared to traditional mechanical conveying methods. By using compressed air efficiently, the equipment reduces operational costs while maintaining high throughput rates. Additionally, the equipment is designed for durability and long service life, with robust materials and components that can withstand the abrasive nature of cement particles. This reduces downtime and maintenance expenses over the equipment's lifespan. The equipment also features advanced control systems that allow for precise regulation of air flow and material feed, ensuring consistent performance and minimizing the risk of blockages or overloading.




