HeadPowder, a leading provider in the field, specializes in the design and manufacturing of efficient pneumatic conveying systems for various powder materials, including rice bran. This article will delve into the working principle and key features of the rice bran powder pneumatic conveying line, highlighting how such systems enhance operational efficiency and product quality in industrial applications.
Working Principle of the Rice Bran Powder Pneumatic Conveying Line
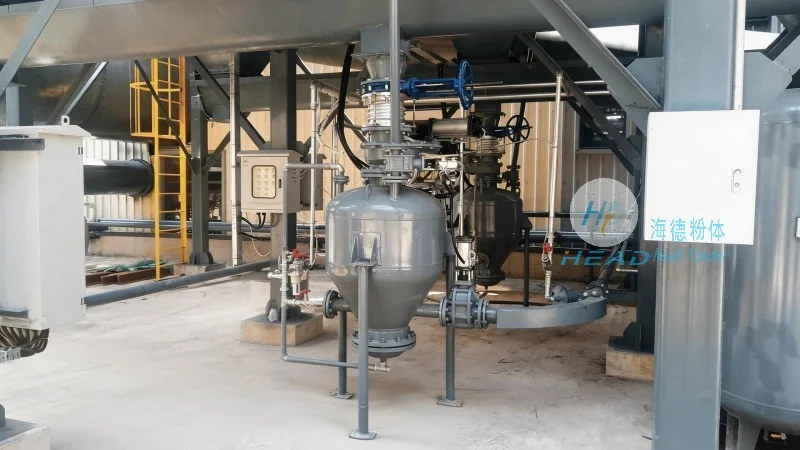
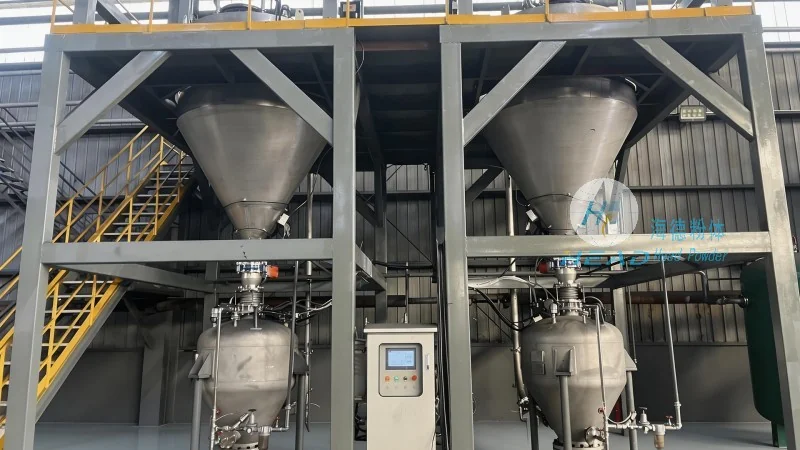
The rice bran powder pneumatic conveying system operates on the principle of air flow to transport bulk powders. In this system, a fan or blower generates a high-pressure air stream that pulls or pushes the rice bran particles through a pipeline. The system typically consists of several components, including a hopper for material storage, a feeder to control the flow rate, a pipeline network, and a receiver for the discharged material. The air flow creates a negative pressure (suction) or positive pressure (blowing) environment, depending on the system design, to move the rice bran from the source to the destination. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing safety. The system's efficiency is determined by factors such as air velocity, particle size, and moisture content of the rice bran, all of which are optimized to ensure smooth and continuous transport.
Key Features of the Rice Bran Powder Pneumatic Conveying System
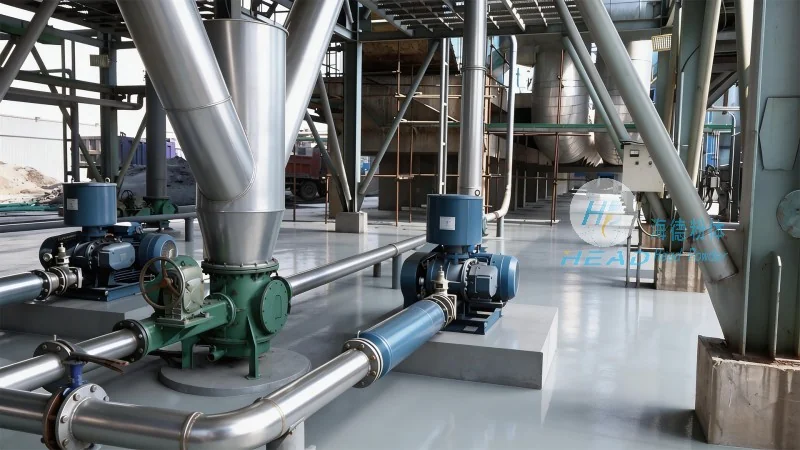
HeadPowder's rice bran powder pneumatic conveying line offers several advantages that make it an ideal choice for industrial applications. Firstly, it provides a dust-free and hygienic environment, which is crucial for food processing industries where rice bran is used. The enclosed system prevents contamination and maintains product purity, meeting stringent quality standards. Secondly, the system is highly flexible and can be easily integrated into existing production lines. It allows for the transport of rice bran over long distances and through multiple stages of processing without the need for intermediate storage. Thirdly, the pneumatic conveying system is energy-efficient compared to traditional methods like bucket elevators or screw conveyors. By optimizing air flow and pressure, the system minimizes energy consumption while maximizing throughput. Additionally, the system is low-maintenance, as it has fewer moving parts, reducing downtime and operational costs. The design also allows for easy cleaning and sanitation, which is essential for maintaining compliance with food safety regulations. Finally, the system's scalability enables it to handle varying production volumes, making it suitable for both small-scale and large-scale operations.
About HeadPowder Engineering Co., Ltd.
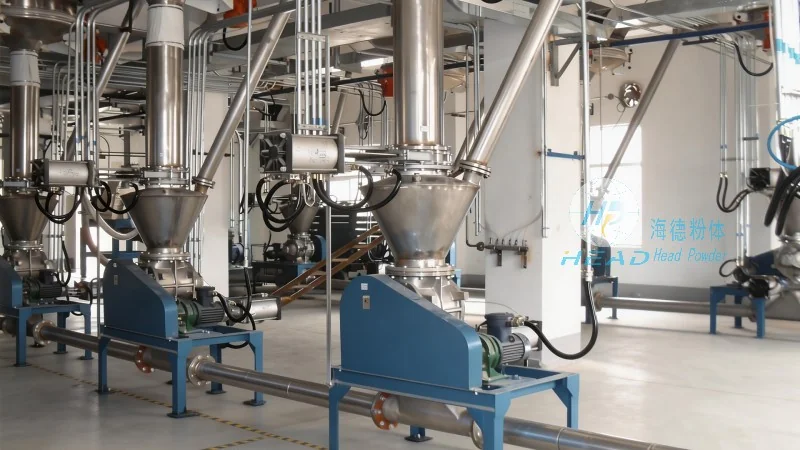
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer and supplier based in Shandong, China. With years of experience in the industry, the company specializes in the development of customized pneumatic conveying solutions tailored to the specific needs of clients. The company's commitment to quality and innovation has earned it a reputation for delivering reliable and efficient systems that meet international standards. HeadPowder's team of engineers and technicians work closely with clients to understand their operational requirements and design systems that enhance productivity and reduce costs. The company's products are widely used in food processing, pharmaceuticals, and chemical industries, among others, where the transport of powders is critical to the production process.




