For businesses involved in rice processing and handling, an efficient material handling system is crucial for maintaining productivity and ensuring product quality. The rice material handling system developed by Shandong HeadPowder Engineering Co., Ltd. is designed to address the specific challenges of transporting and managing rice grains. This article will explore the working principle and key features of this system, providing insights into how it enhances operational efficiency in rice processing facilities.
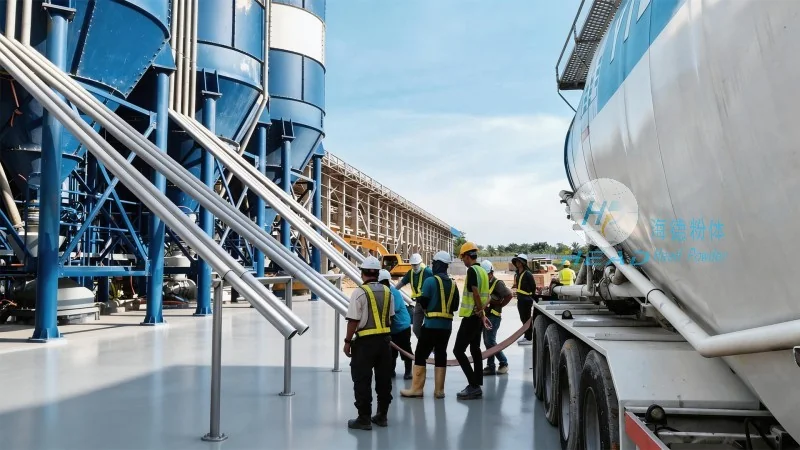
Working Principle of the Rice Material Handling System
The rice material handling system operates on a combination of mechanical and automated processes to ensure seamless movement of rice from storage to processing stages. At its core, the system utilizes a series of conveyor belts, elevators, and storage bins to manage the flow of rice. The process begins with the intake of raw rice from storage silos or bulk containers. A feeding mechanism then transfers the rice onto a primary conveyor belt, which transports it to a cleaning and sorting unit. This unit removes impurities such as stones, dust, and foreign materials, ensuring that only high-quality rice proceeds to the next stage. After cleaning, the rice is conveyed to a storage hopper or directly to the milling machine. The system also incorporates a control panel that monitors the entire process, allowing operators to adjust speed, flow rate, and other parameters in real-time. This automated control ensures consistent performance and minimizes human error, contributing to a stable and reliable operation.
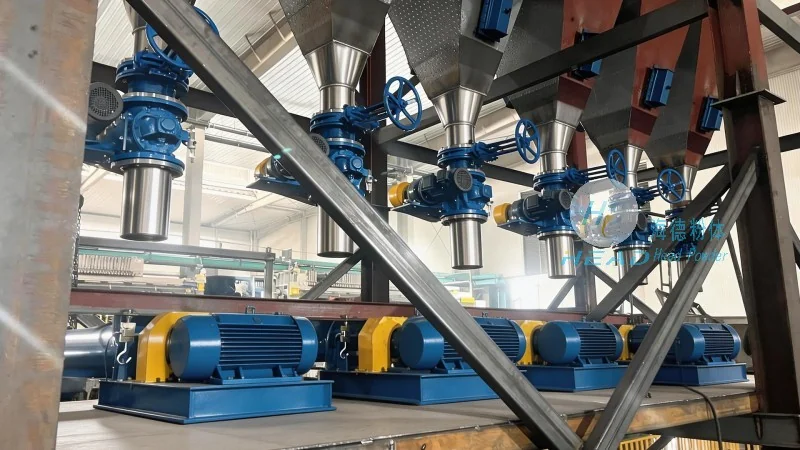
Key Features of the Rice Material Handling System
Shandong HeadPowder Engineering Co., Ltd. has integrated several advanced features into their rice material handling system to meet the demands of modern rice processing. One of the standout features is the use of high-capacity, low-friction conveyor belts that can handle large volumes of rice without causing damage to the grains. The system is also equipped with adjustable speed controls, enabling operators to match the processing speed to the production requirements. Additionally, the system includes a dust collection and filtration system, which helps maintain a clean working environment and prevents product contamination. The modular design of the system allows for easy integration with existing processing lines, making it a flexible solution for both new and retrofit installations. Another important feature is the integration of sensors and monitoring tools that provide real-time data on system performance, including flow rates, temperature, and material levels. This data is crucial for predictive maintenance, allowing for timely repairs and reducing downtime. The system also features a safety interlock mechanism that automatically stops the conveyor in case of blockages or other hazards, enhancing workplace safety.
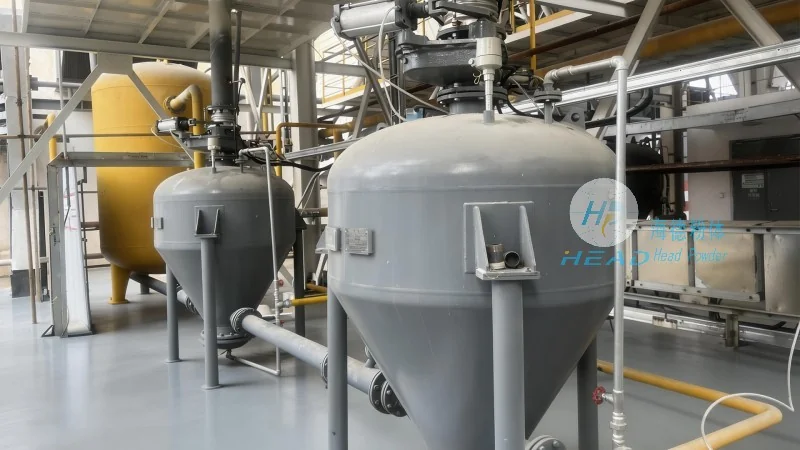
Application and Benefits in Rice Processing
The rice material handling system is widely used in rice mills, food processing plants, and agricultural cooperatives. Its primary benefits include increased throughput, reduced labor costs, and improved product quality. By automating the material handling process, the system minimizes the need for manual labor, which not only reduces operational costs but also improves workplace safety. The system's ability to handle large volumes of rice efficiently ensures that processing lines can operate at optimal capacity, meeting production targets without bottlenecks. Furthermore, the system's design minimizes product loss and damage during transport, which is critical for maintaining the quality of the final rice product. The integration of cleaning and sorting units also ensures that only the best-quality rice is processed, enhancing the overall value of the end product. In addition, the system's modular and scalable design allows it to be customized to fit the specific needs of different processing facilities, whether they are small-scale operations or large industrial plants.
Conclusion and Company Overview
Shandong HeadPowder Engineering Co., Ltd. has established itself as a leading provider of specialized material handling solutions for the rice industry. The rice material handling system, with its robust working principle and advanced features, offers a reliable and efficient solution for businesses looking to enhance their processing capabilities. By leveraging the expertise of HeadPowder, rice processing facilities can achieve higher productivity, better product quality, and reduced operational costs. The company's commitment to innovation and customer satisfaction has made it a trusted partner in the industry, with a reputation for delivering high-quality, durable equipment that meets the evolving needs of rice processing. With its headquarters in Shandong, China, HeadPowder continues to serve clients globally, providing tailored solutions that drive success in the rice processing sector.




