Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer specializing in powder handling solutions. Based in Shandong, China, the company has established itself as a trusted provider of advanced equipment for transporting and managing potassium carbonate powder. This article explores the working principle and key features of their powder conveying systems, highlighting how they enhance efficiency and reliability in industrial applications.
The Working Principle of the Potassium Carbonate Powder Conveying System
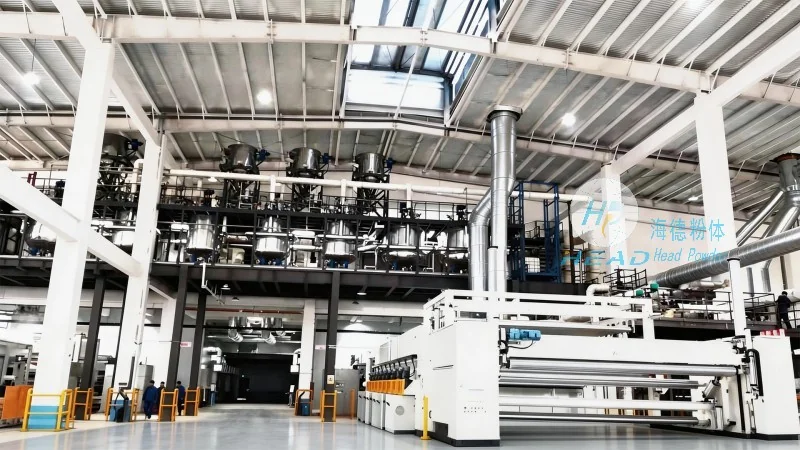
The potassium carbonate powder conveying system developed by headpowder is designed to efficiently transport bulk potassium carbonate powder from storage to processing or packaging areas. The system typically operates on the principle of pneumatic or mechanical conveying, depending on the specific requirements of the application. Pneumatic conveying uses compressed air to move the powder through a network of pipes, while mechanical systems employ screw conveyors, belt conveyors, or bucket elevators. In the case of headpowder's systems, a combination of these methods is often employed to ensure optimal performance. The process begins with the powder being fed into a hopper, where it is then transported through a series of sealed pipes or conveyor sections. The system is equipped with sensors and control mechanisms to monitor flow rates, pressure, and other critical parameters, ensuring consistent and safe operation. This integrated approach allows for precise control over the conveying process, minimizing material loss and preventing contamination.
Key Features of the Potassium Carbonate Powder Conveying System
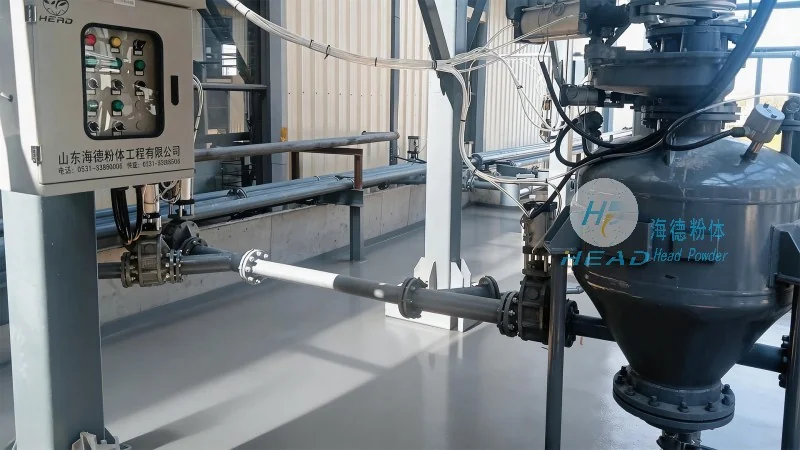
headpowder's potassium carbonate powder conveying systems are characterized by several advanced features that set them apart in the industry. Firstly, the systems are designed with high durability and corrosion resistance, making them suitable for handling potassium carbonate, which can be abrasive and reactive under certain conditions. The equipment is constructed from high-quality materials, such as stainless steel, to withstand the chemical properties of the powder and ensure long-term reliability. Secondly, the systems offer excellent sealing capabilities, which is crucial for preventing dust emissions and maintaining a clean working environment. Advanced sealing technologies, including double-flap valves and airlocks, are integrated into the design to minimize leakage and comply with environmental regulations. Thirdly, the conveying systems are equipped with intelligent control systems that enable real-time monitoring and adjustment of operational parameters. This allows operators to optimize the system's performance based on production demands, reducing energy consumption and improving overall efficiency. Additionally, the systems are designed for easy maintenance and cleaning, with accessible components that can be quickly disassembled and sanitized. This feature is particularly important in industries where hygiene and product purity are paramount, such as food and pharmaceutical processing.
Benefits and Applications
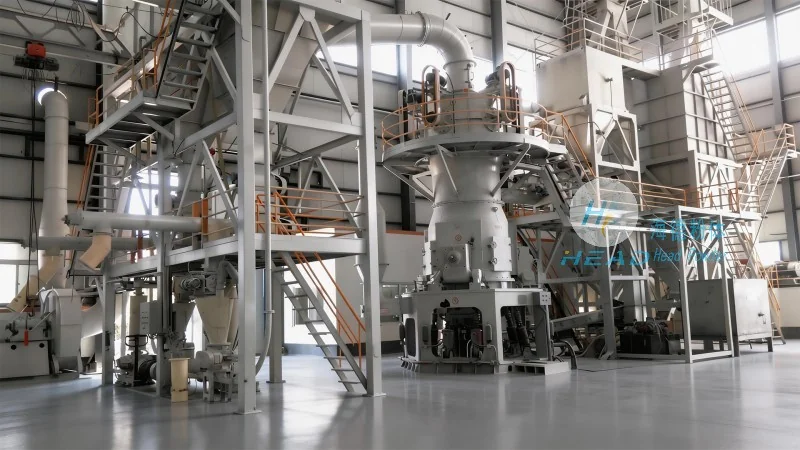
The efficient and reliable operation of headpowder's potassium carbonate powder conveying systems brings numerous benefits to industrial processes. By ensuring consistent and controlled powder flow, the systems help maintain product quality and reduce downtime caused by material blockages or spills. The advanced sealing and control features also contribute to a safer working environment, reducing the risk of dust explosions and improving workplace safety. These systems are widely used in various industries, including chemical manufacturing, food processing, and pharmaceutical production, where the handling of potassium carbonate is essential. Whether for large-scale production or small-scale processing, headpowder's conveying solutions provide a versatile and effective means of managing potassium carbonate powder, meeting the demands of modern industrial operations.




