At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design and manufacturing of advanced powder handling equipment tailored for the sugar industry. Our sugar powder conveyors are engineered to efficiently transport granular and powdered sugar, ensuring optimal performance and reliability in various industrial applications.
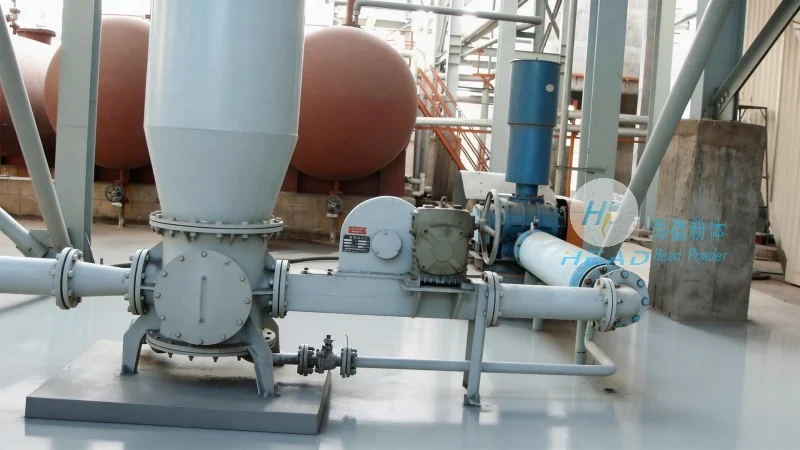
Working Principle of Sugar Powder Conveyors
The core mechanism of a sugar powder conveyor involves the use of a rotating drum or screw to move material through a sealed system. As the conveyor rotates, it lifts and transports the sugar powder from the inlet to the outlet. This process is typically driven by an electric motor, which provides the necessary torque to operate the conveyor. The sealed design prevents dust and moisture from contaminating the product, maintaining its quality and purity. The conveyor's speed and capacity can be adjusted to meet specific production requirements, allowing for flexible operation in different processing stages.
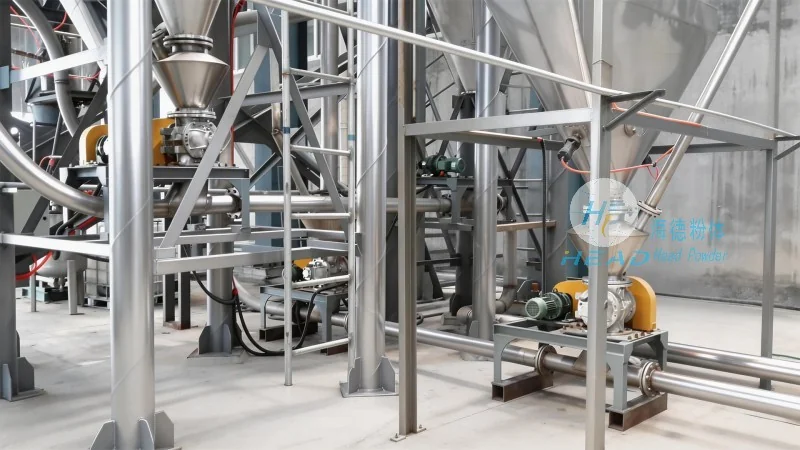
Key Features of Sugar Powder Conveyors
Our sugar powder conveyors are equipped with several advanced features that enhance their performance and durability. One of the primary features is the robust construction, which includes high-quality materials such as stainless steel and corrosion-resistant components, ensuring long-term use in harsh environments. The sealed housing design minimizes dust emissions, promoting a cleaner working environment and compliance with industrial safety standards. Additionally, the conveyors are designed with easy maintenance in mind, featuring accessible components and simple cleaning procedures. This reduces downtime and maintenance costs, making them a cost-effective solution for sugar processing facilities. Another notable feature is the adjustable speed control, which allows operators to regulate the flow rate of sugar powder based on production needs. This flexibility is crucial for maintaining consistent product quality and preventing overloading or underloading of the conveyor system.
Application in Sugar Processing
Sugar powder conveyors are widely used in the sugar industry for various applications, including the transportation of raw sugar, refined sugar, and other sugar derivatives. They are commonly employed in sugar mills, refineries, and food processing plants to move sugar from storage silos to processing lines or packaging areas. The efficient and reliable operation of these conveyors ensures smooth workflow and minimizes the risk of product loss or contamination. By integrating our sugar powder conveyors into your processing system, you can improve operational efficiency and maintain high standards of product quality.
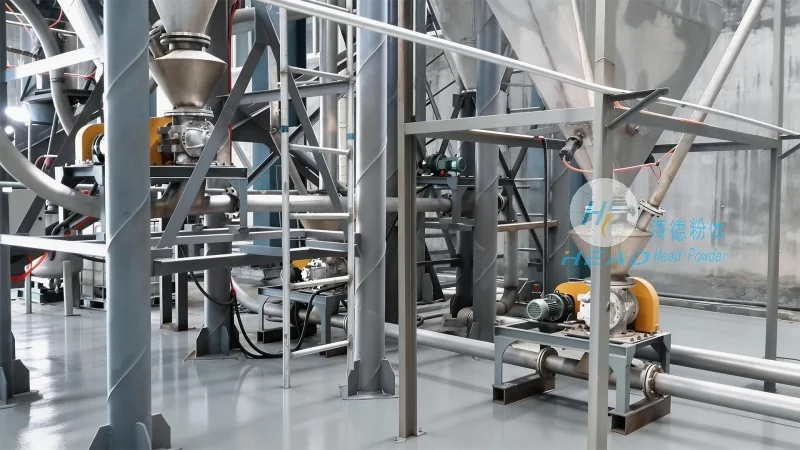
Advantages of Choosing HeadPowder Conveyors
When selecting a sugar powder conveyor, it is essential to consider factors such as efficiency, durability, and ease of maintenance. Shandong HeadPowder Engineering Co., Ltd. offers a range of conveyors that meet these criteria, providing several advantages over traditional methods. Our conveyors are designed to handle high volumes of sugar powder with minimal energy consumption, reducing operational costs. The robust construction and corrosion-resistant materials ensure that the equipment can withstand the harsh conditions often encountered in sugar processing environments. Furthermore, our conveyors are easy to install and maintain, with accessible components that allow for quick repairs and cleaning. This reduces downtime and ensures continuous operation. The adjustable speed control feature also allows for precise control over the flow rate, preventing issues such as clogging or uneven distribution of sugar powder. By choosing our sugar powder conveyors, you can enhance the overall performance of your sugar processing facility and achieve better results in terms of productivity and product quality.




