

Working Principle and Features of Intelligent Centralized Pneumatic Conveying Systems
Intelligent centralized pneumatic conveying systems represent a sophisticated solution for material handling in various industrial applications. These systems are designed to efficiently transport bulk materials over long distances with minimal human intervention, leveraging advanced technology to optimize performance and reliability. As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in developing and supplying such systems, catering to diverse industry needs from food processing to chemical manufacturing.
Working Principle of Intelligent Centralized Pneumatic Conveying Systems
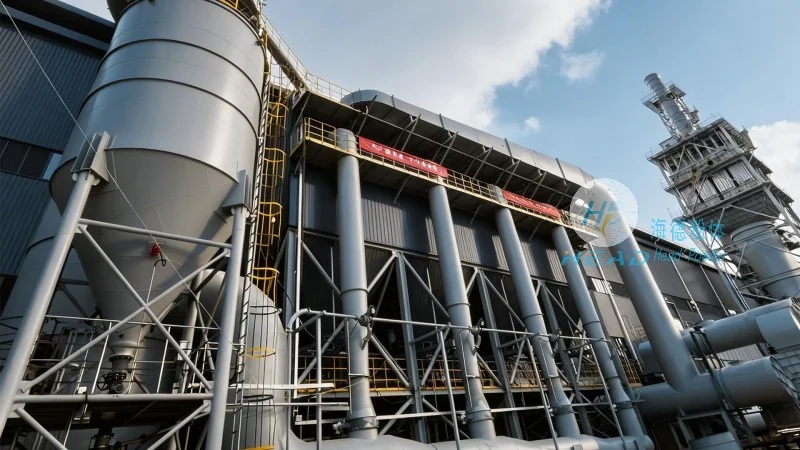
The core mechanism of intelligent centralized pneumatic conveying systems involves the use of compressed air to transport dry bulk materials through a network of pipes. The process typically begins with material loading into a hopper or silo, where it is then drawn into the conveying line by a vacuum or pressure source. The system utilizes a combination of positive and negative pressure zones to control the flow of material, ensuring smooth and consistent transport. Advanced control systems, often integrated with sensors and automation, monitor parameters such as pressure, flow rate, and material level in real-time, allowing for dynamic adjustments to maintain optimal operation. This intelligent control not only enhances efficiency but also reduces downtime and operational costs.
Key Features of Intelligent Centralized Pneumatic Conveying Systems
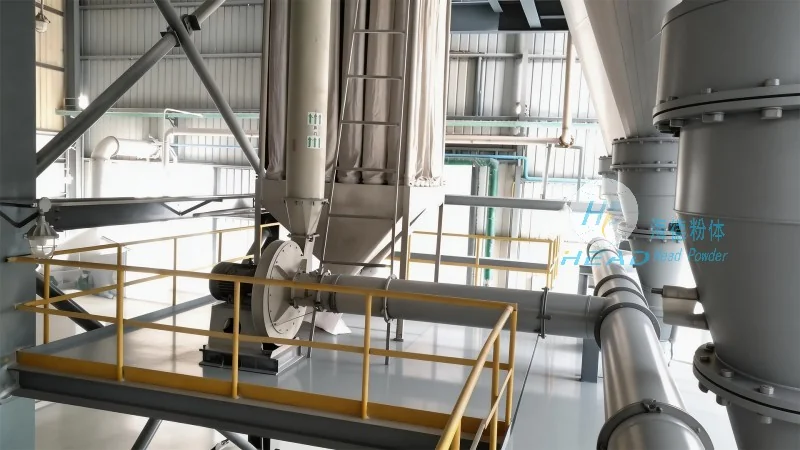
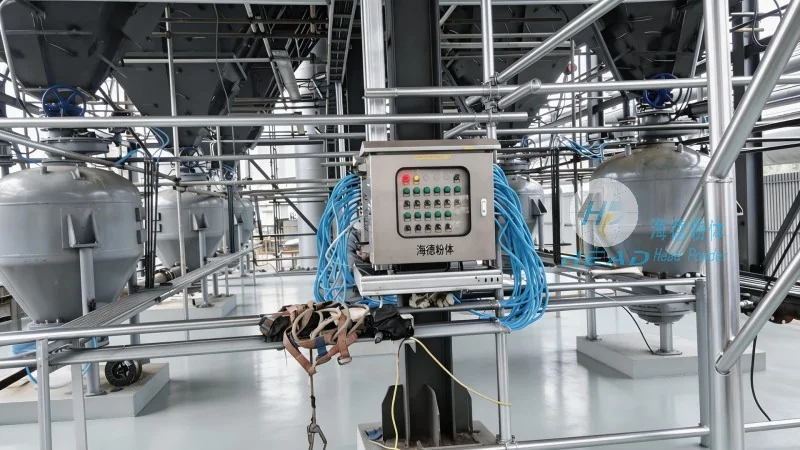
Intelligent centralized pneumatic conveying systems are equipped with several distinctive features that set them apart from traditional conveying methods. One of the primary advantages is their centralized control, which allows for the management of multiple conveying lines from a single interface. This centralized approach simplifies maintenance and troubleshooting, as operators can monitor and adjust all connected lines simultaneously. Additionally, these systems often incorporate energy-efficient designs, utilizing variable frequency drives (VFDs) to regulate air flow and pressure, thereby reducing energy consumption and operational expenses. The integration of sensors and real-time data analytics provides valuable insights into system performance, enabling predictive maintenance and proactive problem resolution. Furthermore, the modular construction of these systems facilitates easy expansion or modification, adapting to changing production requirements without significant reconfiguration.
Applications and Benefits in Industrial Settings
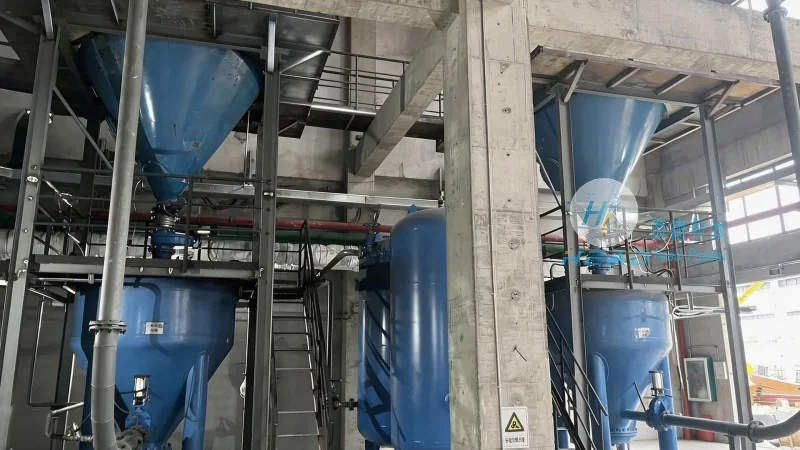
Intelligent centralized pneumatic conveying systems find extensive applications across a wide range of industries, including pharmaceuticals, food processing, chemicals, and mining. In the pharmaceutical industry, for instance, these systems are employed to transport sensitive powders with strict contamination control measures, ensuring compliance with regulatory standards. In food processing, they enable hygienic and dust-free handling of ingredients, maintaining product quality and safety. The benefits of such systems extend beyond efficiency, as they also contribute to improved workplace safety by eliminating manual handling of bulk materials and reducing the risk of dust-related health issues. Moreover, the compact design of these systems allows for installation in limited spaces, making them suitable for retrofitting into existing facilities or new construction projects.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a reputable manufacturer specializing in the design, development, and supply of intelligent centralized pneumatic conveying systems. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for industries seeking reliable material handling solutions. HeadPowder's headquarters is located in Shandong, China, where the company leverages advanced manufacturing capabilities and technical expertise to produce high-performance systems tailored to customer specifications. The company's product line includes a variety of conveying equipment, from basic pneumatic systems to fully automated, intelligent solutions, catering to diverse industrial needs. By adhering to stringent quality standards and providing comprehensive after-sales support, HeadPowder ensures customer satisfaction and long-term partnerships.