

What is a Nitrate Ammonium Material Handling System Equipment? What Are Its Design Principles?
Understanding the design and functionality of a nitrate ammonium material handling system equipment is crucial for industries dealing with this specific chemical compound. As a key component in material transport and processing, these systems are engineered to handle the unique properties of nitrate ammonium efficiently and safely. This article explores the core aspects of such equipment, including its design principles and operational considerations.
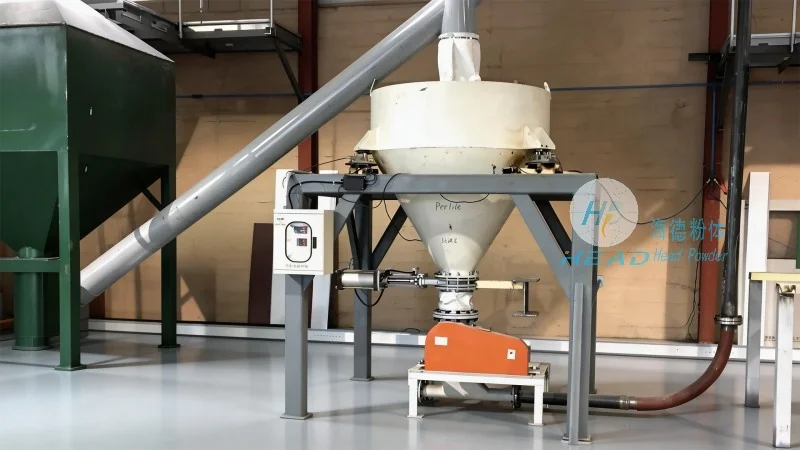
Introduction to Nitrate Ammonium Material Handling Systems
A nitrate ammonium material handling system equipment is a specialized setup designed to transport, store, and process nitrate ammonium, a widely used chemical in agricultural and industrial applications. The system integrates various components like conveyors, storage silos, and handling mechanisms to ensure the safe and efficient movement of this material. The design of these systems must account for the chemical's properties, such as its reactivity and potential for dust generation, to maintain operational safety and compliance with industry standards.
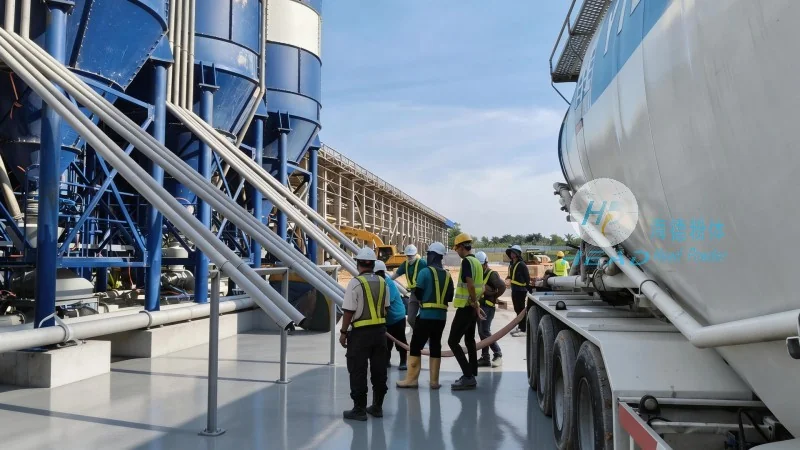
Key Components of the Nitrate Ammonium Material Handling System
The core components of a nitrate ammonium material handling system equipment typically include bulk material handling equipment like screw conveyors, bucket elevators, and pneumatic conveying systems. These components are selected based on the material's characteristics and the specific requirements of the application. For instance, screw conveyors are often used for horizontal or slight incline transport due to their ability to handle dry, free-flowing materials without the need for additional power sources. Bucket elevators, on the other hand, are ideal for vertical transport, providing a reliable means to move nitrate ammonium from lower to higher levels in a facility. Pneumatic conveying systems may be employed for long-distance or complex routing, utilizing air pressure to transport the material through pipelines.
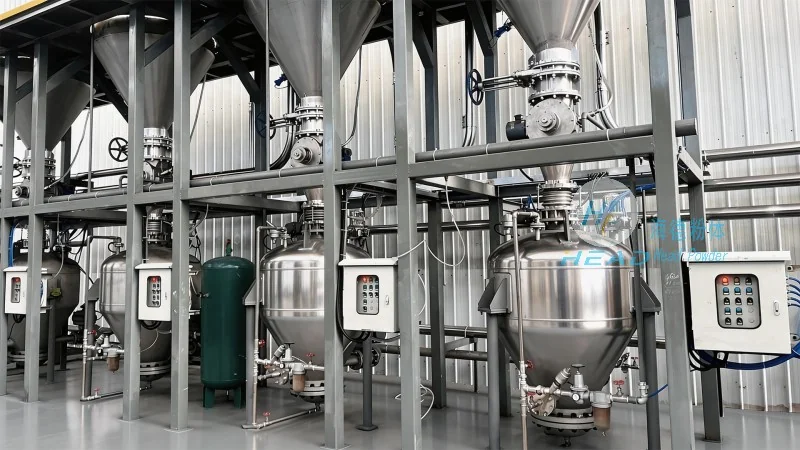
Design Principles for Safety and Efficiency
The design of a nitrate ammonium material handling system equipment is guided by several critical principles aimed at ensuring both safety and operational efficiency. First, the system must prioritize safety measures to prevent accidents, such as dust explosions or chemical reactions. This includes the use of explosion-proof components, proper ventilation systems, and material handling equipment designed to minimize dust generation. Second, efficiency is achieved through optimized material flow, reduced downtime, and energy conservation. Engineers often employ computational fluid dynamics (CFD) and other simulation tools to model the material's behavior within the system, ensuring that the design minimizes friction losses and maximizes throughput. Additionally, the system's modular design allows for easy maintenance and scalability, adapting to changing production needs over time.
Operational Considerations and Maintenance
Operational considerations for a nitrate ammonium material handling system equipment extend beyond initial design. Regular maintenance is essential to ensure the system's longevity and performance. This includes routine checks of conveyor belts, motor systems, and storage silos for signs of wear or damage. The use of corrosion-resistant materials, such as stainless steel or specialized coatings, is common in these systems to withstand the chemical properties of nitrate ammonium and prevent degradation over time. Furthermore, the system's integration with other industrial processes, such as blending or packaging, requires careful coordination to maintain consistent material quality and flow rates. By adhering to these operational guidelines, industries can maximize the reliability and effectiveness of their nitrate ammonium material handling systems.
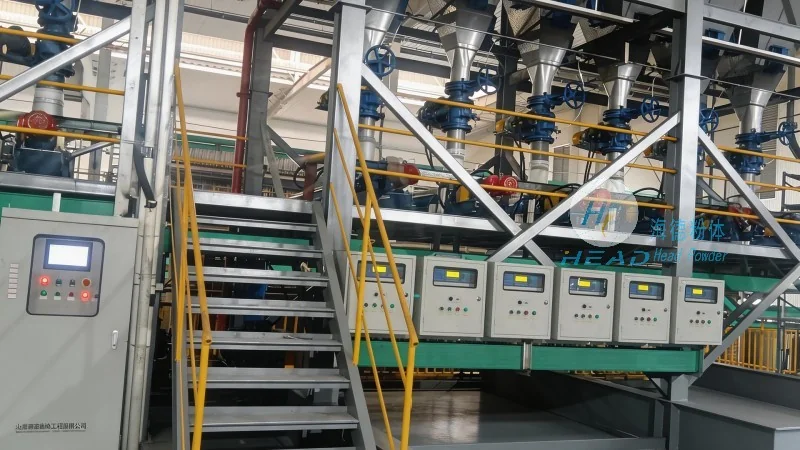
Conclusion: The Importance of Specialized Equipment
In conclusion, a nitrate ammonium material handling system equipment is a sophisticated solution tailored to the unique demands of handling this chemical compound. The design principles, component selection, and operational strategies all work in concert to ensure safety, efficiency, and compliance with industry standards. As industries continue to rely on nitrate ammonium for various applications, the importance of investing in well-designed and maintained material handling systems cannot be overstated. The expertise of companies like Shandong HeadPowder Engineering Co., Ltd., based in China, plays a vital role in developing and implementing these systems, providing tailored solutions that meet the specific needs of their clients.