When it comes to industrial material handling, especially for chemical products like sulfamyl ammonium, specialized conveyor systems are essential for efficient and safe transportation. This article delves into the concept of a sulfamyl ammonium material handling conveyor, exploring its purpose and the underlying design principles that ensure optimal performance in industrial settings.
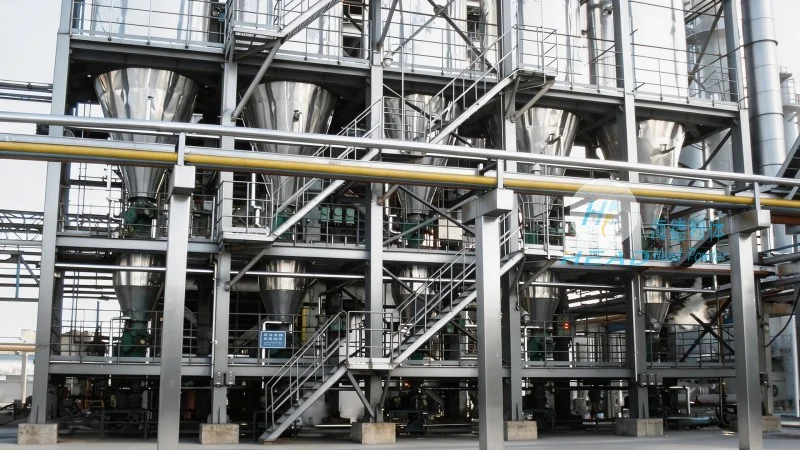
Understanding the Sulfamyl Ammonium Material Handling Conveyor
A sulfamyl ammonium material handling conveyor is a specialized piece of equipment designed to transport sulfamyl ammonium, a common chemical compound used in various industrial applications such as fertilizers, pharmaceuticals, and chemical manufacturing. The primary function of this conveyor is to move the material from one point to another within a production facility or processing plant with precision and efficiency. These systems are engineered to handle the specific physical and chemical properties of sulfamyl ammonium, ensuring that the material is transported without degradation or contamination.
Key Design Principles for Sulfamyl Ammonium Conveyors
The design of a sulfamyl ammonium material handling conveyor is guided by several critical principles to ensure reliability and effectiveness. First, the material of construction is a key consideration. Since sulfamyl ammonium can be corrosive or reactive under certain conditions, the conveyor components, such as the belt, rollers, and frame, are typically made from materials that are resistant to chemical exposure, such as stainless steel or specialized polymers. This prevents degradation and maintains the integrity of the conveyor over time.
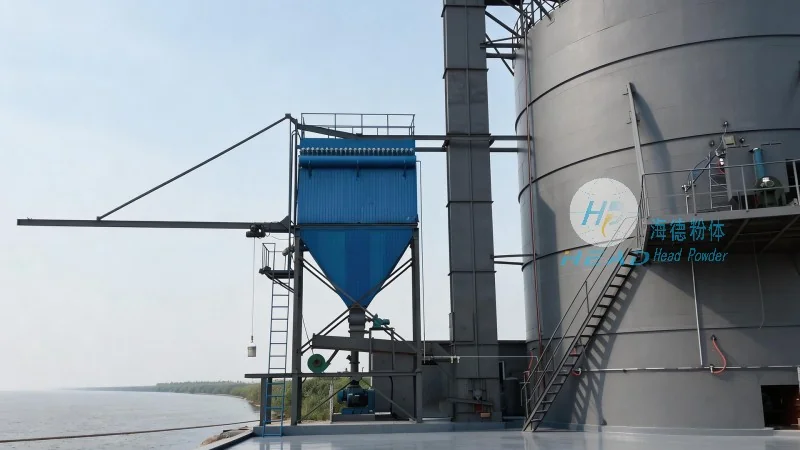
Second, the conveyor's capacity and speed are tailored to the production requirements. The system is designed to handle the specific volume of sulfamyl ammonium that needs to be moved, ensuring that the conveyor operates at an optimal speed without causing material buildup or spillage. This is crucial for maintaining a smooth production flow and minimizing downtime.
Third, the system incorporates features for safety and maintenance. For instance, the conveyor may include sensors to detect blockages or overloads, which can trigger an automatic stop to prevent damage. Additionally, the design allows for easy access to components for cleaning and maintenance, ensuring that the system remains in good working condition and reduces the risk of operational issues.
Components and Functionalities of the Conveyor System
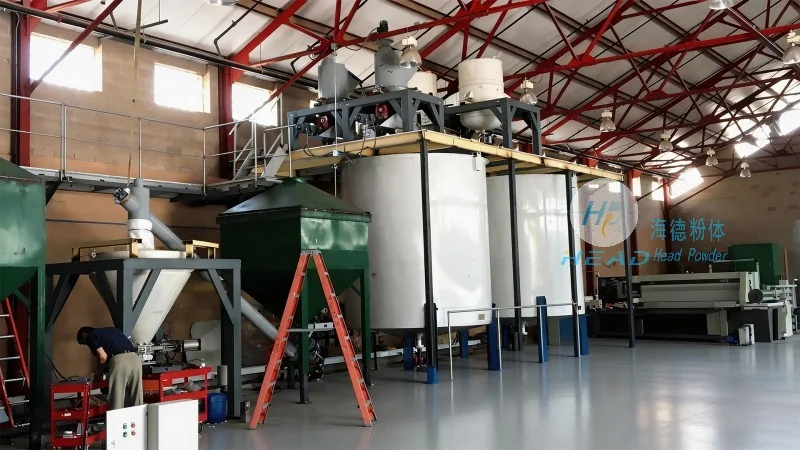
The sulfamyl ammonium material handling conveyor consists of several key components that work together to achieve its purpose. The main components include the conveyor belt, which carries the material, the drive system that powers the belt, the idlers that support the belt, and the frame that houses all the components. The conveyor may also include additional features such as feeders or chutes to direct the material onto the belt and discharge mechanisms to release the material at the end of the line.
The drive system is typically powered by an electric motor, which can be adjusted to control the speed of the conveyor. The idlers are strategically placed along the length of the conveyor to support the belt and maintain its tension, ensuring that the material is transported smoothly without slipping or stretching. The frame provides structural support and stability to the entire system, ensuring that it can withstand the weight and movement of the material being transported.
Applications and Benefits in Industrial Settings
Sulfamyl ammonium material handling conveyors are widely used in various industrial applications where the efficient transportation of this chemical is critical. For example, in fertilizer production, these conveyors are used to move sulfamyl ammonium from storage to processing units, ensuring a continuous supply of raw material. In pharmaceutical manufacturing, the conveyors help transport the chemical to mixing and packaging lines, maintaining the quality and purity of the final product.
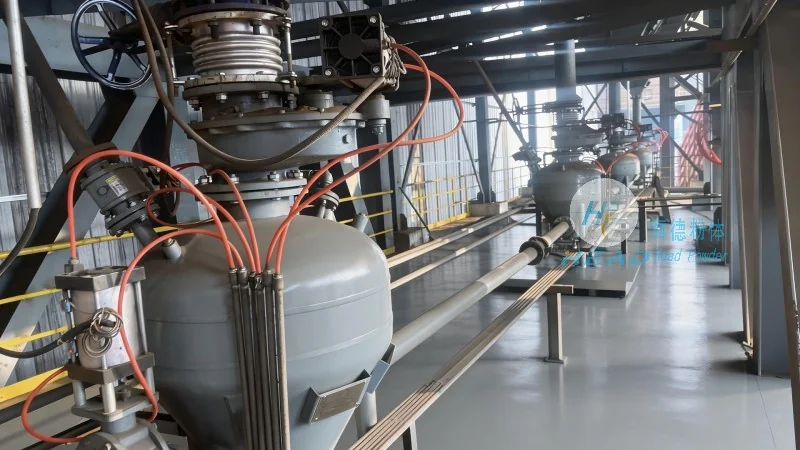
The benefits of using a specialized sulfamyl ammonium conveyor system include improved efficiency, reduced labor costs, and enhanced safety. By automating the material handling process, the system minimizes the need for manual labor, which can be dangerous when handling chemicals. Additionally, the specialized design of the conveyor ensures that the material is transported without contamination, which is essential for maintaining product quality and compliance with industry standards.
Conclusion
In conclusion, a sulfamyl ammonium material handling conveyor is a vital piece of equipment in industrial settings, designed to efficiently and safely transport this chemical compound. The design principles, components, and applications of these conveyors are tailored to meet the specific needs of the industry, ensuring optimal performance and reliability. As a leading provider of industrial equipment, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such conveyor systems, leveraging years of experience to deliver high-quality solutions for clients worldwide.




