When it comes to handling limestone powder in industrial applications, the limestone powder conveyor plays a crucial role in ensuring efficient and reliable material transport. As a key component in many processing plants, understanding what this equipment is and how it operates is essential for optimizing production processes. This article will explore the fundamentals of limestone powder conveyors, focusing on their design principles and the technology behind their operation.
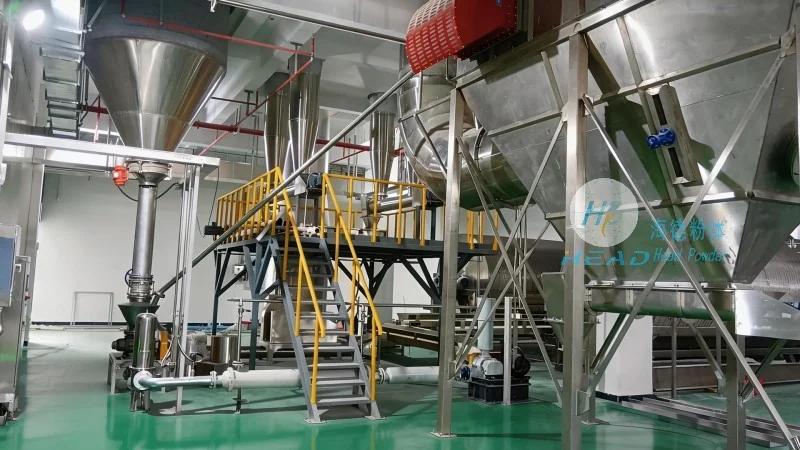
Understanding Limestone Powder Conveyors
A limestone powder conveyor, also known as a limestone powder handling system, is a specialized piece of equipment designed to transport fine limestone powder from one location to another within a processing facility. These systems are commonly used in industries such as mining, cement production, and chemical processing, where limestone is a primary raw material. The primary function of a limestone powder conveyor is to move limestone powder in a controlled manner, minimizing dust generation and ensuring consistent material flow. The design of these conveyors is tailored to handle the unique properties of limestone powder, including its fine particle size and potential for dust formation.
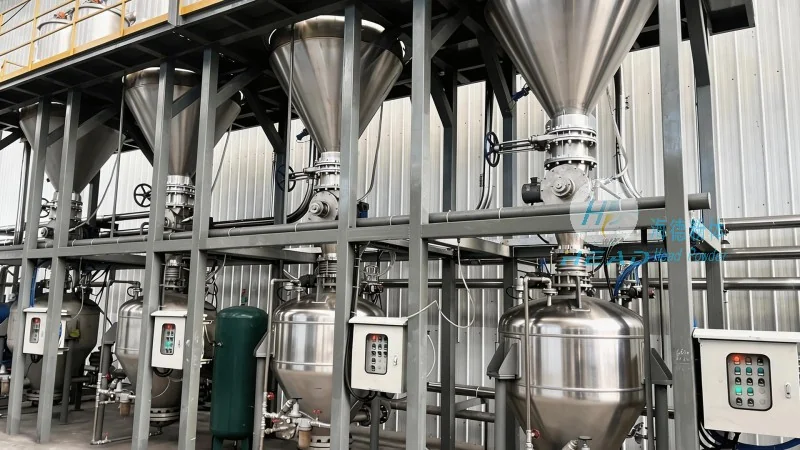
Key Design Principles of Limestone Powder Conveyors
The design of a limestone powder conveyor is based on several critical principles that ensure its effectiveness and reliability. One of the most important principles is the use of enclosed systems to contain dust and prevent environmental contamination. This is achieved through the use of sealed conveyor belts, housing, and feeding mechanisms that keep the limestone powder contained within the system. Another key principle is the selection of appropriate materials for the conveyor components. Since limestone powder can be abrasive and corrosive, components such as belts, pulleys, and hoppers are typically made from durable materials like rubber, stainless steel, or specialized alloys to withstand wear and tear. The design also emphasizes the need for smooth and consistent material flow, which is facilitated by the use of inclined or horizontal conveyor sections, depending on the layout of the processing plant.
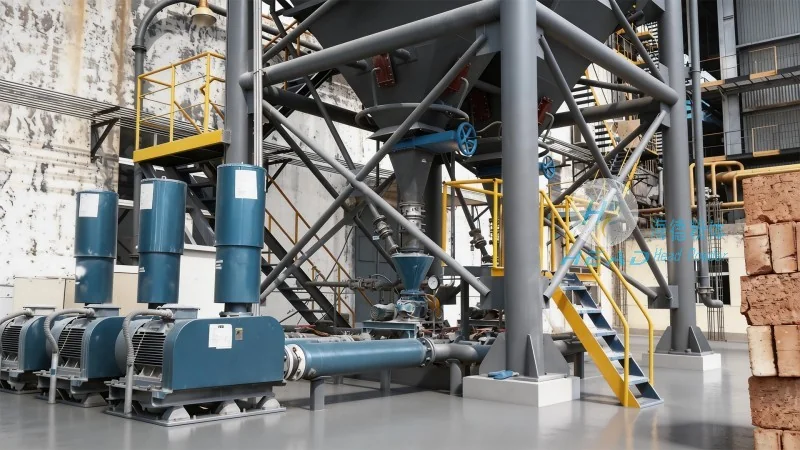
Components and Operational Mechanisms
At the core of a limestone powder conveyor are several key components that work together to ensure efficient operation. The feeding mechanism, often a hopper or a rotary valve, is responsible for introducing limestone powder into the conveyor system. This component must be designed to handle the fine particle size of limestone powder and prevent blockages or clogging. The conveyor belt or screw mechanism then transports the powder along the desired path. In many systems, the conveyor is equipped with a drive system, such as a motor and gearbox, that provides the necessary power to move the material. Additionally, the system may include a dust collection system to capture any airborne particles and maintain a clean working environment. The design of these components is critical to the overall performance of the limestone powder conveyor, as any inefficiencies can lead to reduced productivity or increased maintenance costs.
Applications and Benefits
Limestone powder conveyors are widely used in various industrial applications due to their ability to handle fine materials efficiently. In the cement industry, for example, limestone powder is a key raw material used to produce cement. The conveyor system ensures that limestone powder is delivered to the cement production line in a consistent and controlled manner, which is essential for maintaining the quality of the final product. Similarly, in chemical processing plants, limestone powder is used as a filler or raw material in the production of various chemicals. The benefits of using a limestone powder conveyor include improved safety by reducing dust exposure, increased efficiency through consistent material flow, and reduced maintenance costs due to the use of durable components. These systems also contribute to environmental sustainability by minimizing the release of dust into the atmosphere and ensuring proper material handling practices.
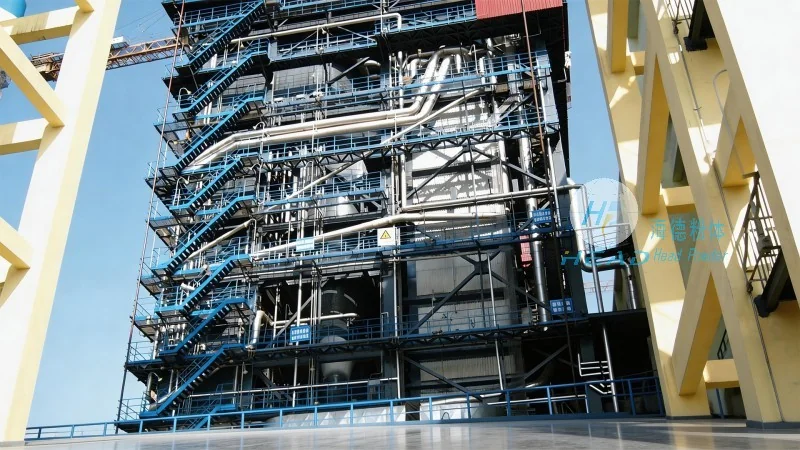
Conclusion
In conclusion, a limestone powder conveyor is a vital piece of equipment in industries that rely on limestone powder as a raw material. The design principles behind these systems focus on efficiency, safety, and durability, ensuring that they can handle the unique challenges of transporting fine limestone powder. By understanding the components and operational mechanisms of these conveyors, industrial facilities can optimize their material handling processes and improve overall productivity. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality limestone powder conveyors that meet the specific needs of various industrial applications. With their expertise in material handling technology, HeadPowder offers reliable and efficient solutions for transporting limestone powder, helping businesses enhance their operational performance and maintain a competitive edge in their respective industries.




