Urea granule material handling equipment plays a crucial role in the efficient and safe transportation of urea granules, a vital fertilizer in modern agriculture. These specialized systems are engineered to handle the unique characteristics of urea granules, such as their size, density, and flow properties, ensuring optimal performance in various industrial and agricultural settings. Understanding the design principles behind these equipment is essential for selecting the right solution for specific applications.
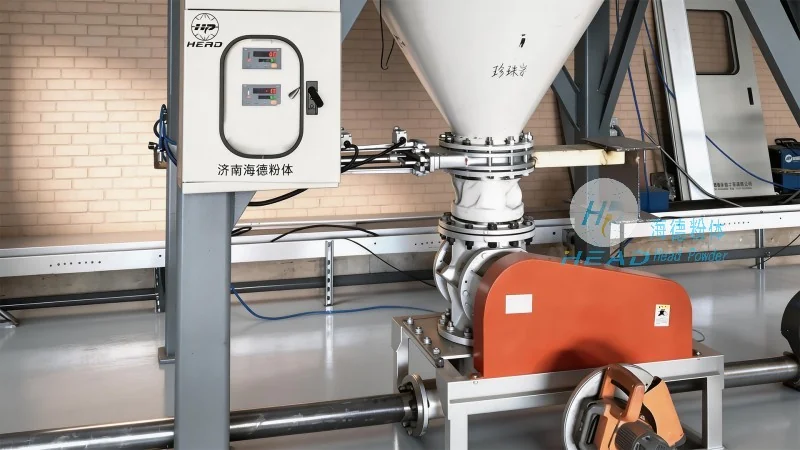
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, manufacturing, and supply of high-quality urea granule material handling equipment. With years of experience in the industry, HeadPowder has developed advanced solutions tailored to meet the diverse needs of clients in the agricultural and chemical sectors. The company's commitment to innovation and quality ensures that their equipment delivers reliable performance and long-term durability.
Design Principles of Urea Granule Material Handling Equipment
The design of urea granule material handling equipment is guided by several key principles to ensure efficient operation and safety. One of the primary considerations is the material's flow characteristics. Urea granules have a relatively uniform size and shape, but their flowability can be influenced by factors like moisture content and particle size distribution. Equipment designers must account for these variables to prevent issues such as bridging, arching, or segregation during transport. To address this, many systems incorporate features like agitators, vibrators, or air knives to maintain consistent flow.
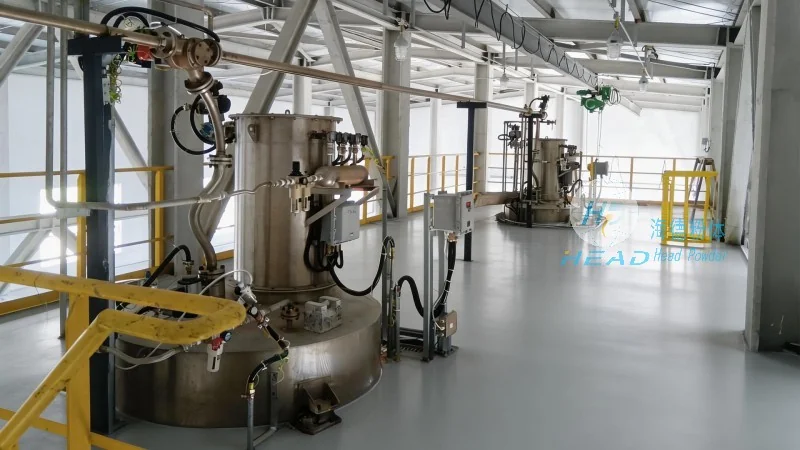
Another critical design principle is the equipment's ability to handle the mechanical properties of urea granules. These particles are relatively hard and can cause wear on equipment components if not managed properly. Therefore, materials of construction, such as stainless steel or specialized alloys, are often used for components that come into direct contact with the granules. Additionally, the design may include features like wear-resistant liners or replaceable parts to minimize maintenance costs and extend the equipment's service life.
Energy efficiency is also a key design consideration. Modern urea granule material handling equipment is designed to minimize energy consumption while maintaining high throughput. This is achieved through optimized drive systems, efficient conveyor designs, and the use of variable frequency drives (VFDs) to adjust motor speed based on the load. By reducing energy usage, these systems not only lower operational costs but also contribute to environmental sustainability.
Applications and Benefits of Urea Granule Material Handling Equipment
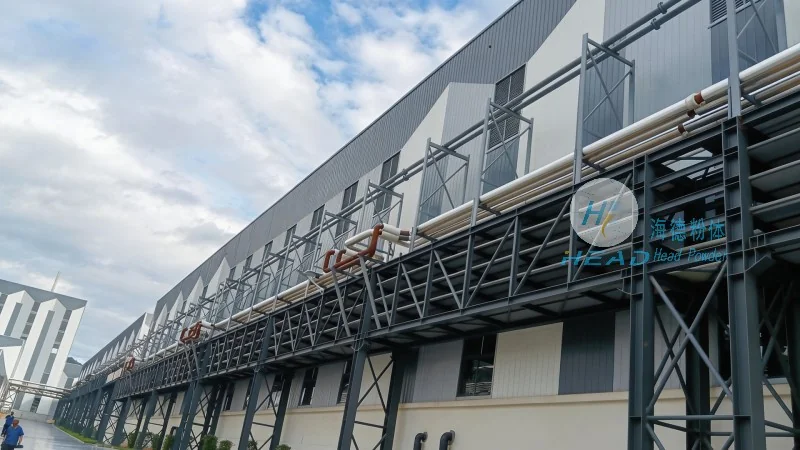
Urea granule material handling equipment is widely used in various stages of the urea production and distribution process. From the granulation plant to storage silos and loading facilities, these systems ensure the smooth and safe movement of urea granules. In the granulation plant, equipment such as screw conveyors or bucket elevators transport the freshly produced granules from the granulation tower to storage silos. During storage, the equipment maintains the granules in a uniform state, preventing caking or segregation. When it's time for distribution, the equipment loads urea granules into trucks or ships, ensuring accurate and efficient loading operations.
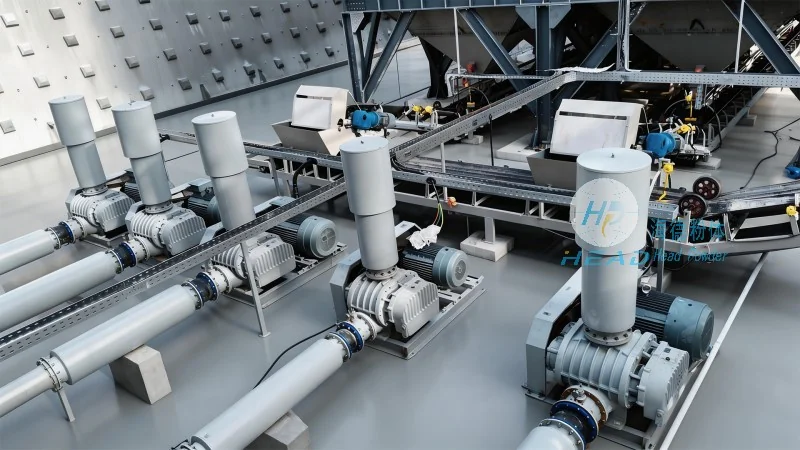
The benefits of using specialized urea granule material handling equipment are numerous. First, these systems improve operational efficiency by reducing downtime and increasing throughput. By minimizing material handling issues like bridging or blockages, the equipment ensures a continuous flow of urea granules, which is critical for meeting production and delivery schedules. Second, the equipment enhances safety by preventing accidents related to material handling, such as spills or equipment failures. This is particularly important in industrial settings where large quantities of urea granules are handled. Third, the equipment contributes to cost savings by reducing maintenance and repair costs through the use of durable materials and efficient design. Finally, the equipment supports environmental sustainability by minimizing energy consumption and reducing the risk of environmental contamination from spills or leaks.
Conclusion
Urea granule material handling equipment is a vital component of the modern fertilizer industry, enabling the efficient and safe transportation of urea granules. The design principles behind these systems, including considerations for material flow, mechanical properties, energy efficiency, and safety, ensure that they meet the demanding requirements of industrial and agricultural applications. HeadPowder, with its expertise and commitment to quality, provides reliable and innovative solutions that help clients optimize their urea granule handling processes. By understanding the design principles and benefits of these equipment, businesses can make informed decisions to enhance their operational efficiency and sustainability.




