Desulfurization and denitrification are critical processes in modern industrial applications, particularly in power generation and chemical manufacturing. The efficient handling of powders used in these processes is essential for maintaining operational efficiency and environmental compliance. This article explores the powder conveying equipment designed specifically for desulfurization and denitrification agents, detailing its design principles and operational aspects.
Understanding the Role of Powder Conveying Equipment in Desulfurization and Denitrification
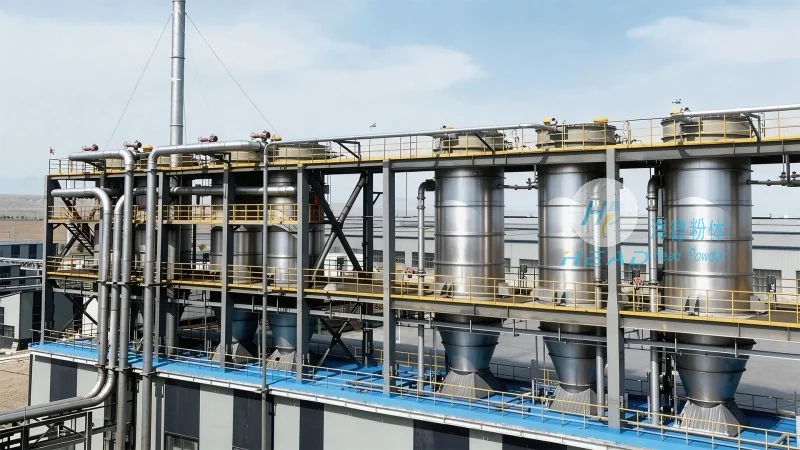
In industrial settings, the transport of fine powders such as those used in flue gas desulfurization (FGD) and selective catalytic reduction (SCR) systems requires specialized equipment to ensure consistent flow, minimize dust emissions, and maintain process stability. The conveying equipment for desulfurization and denitrification agents must address challenges like particle size, moisture content, and the corrosive nature of the materials. These factors influence the choice of equipment, including pneumatic conveyors, screw conveyors, and bucket elevators, each with its own advantages and limitations.
Design Principles of Desulfurization and Denitrification Agent Powder Conveying Equipment
The design of powder conveying equipment for desulfurization and denitrification agents is guided by several key principles to ensure optimal performance. First, the equipment must be constructed from materials resistant to corrosion and abrasion, as the powders often contain acidic or alkaline components. Stainless steel, corrosion-resistant alloys, and specialized coatings are commonly used to protect against material degradation over time. Second, the system must maintain a consistent flow rate to prevent clogging and ensure uniform distribution of the agent in the treatment process. This is achieved through precise control of air pressure, screw speed, or motor power, depending on the conveyor type. Third, the equipment should minimize dust generation and emissions to comply with environmental regulations. Enclosed designs, dust collection systems, and proper sealing mechanisms are integral to achieving this objective.
Key Components and Operational Mechanisms
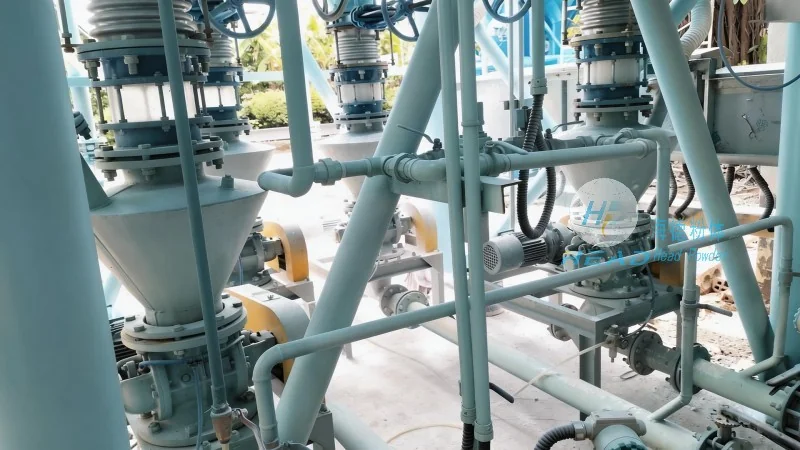
Various components contribute to the effective operation of desulfurization and denitrification agent powder conveying equipment. For example, pneumatic conveyors use compressed air to transport powders through a pipeline, while screw conveyors rely on rotating screws to move material along a trough. Bucket elevators, on the other hand, lift powders vertically using buckets attached to a chain or belt. Each component is designed to handle specific characteristics of the desulfurization and denitrification agents, such as particle size distribution, bulk density, and flowability. The selection of the appropriate conveyor type depends on factors like the volume of material to be conveyed, the distance between the source and destination, and the required flow rate.
Applications and Benefits in Industrial Processes
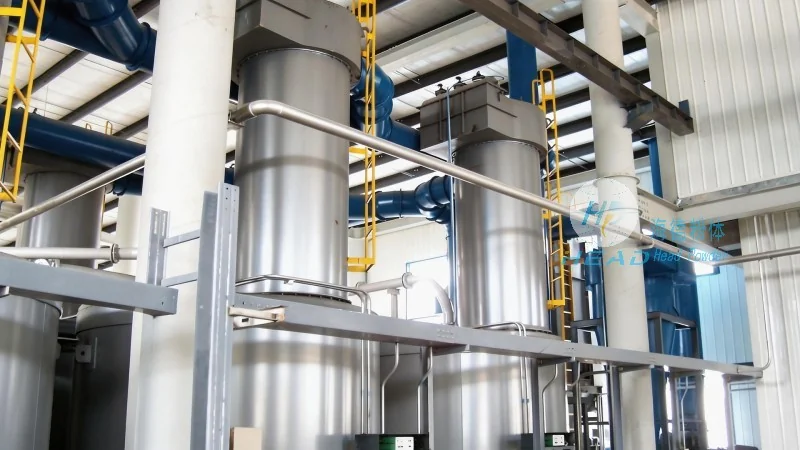
The desulfurization and denitrification agent powder conveying equipment is widely used in power plants, chemical factories, and other industrial facilities where air pollution control is mandatory. By efficiently transporting the necessary agents to the treatment points, these systems enhance the effectiveness of desulfurization and denitrification processes, leading to reduced sulfur dioxide (SO₂) and nitrogen oxides (NOₓ) emissions. The benefits of using specialized conveying equipment include improved process control, reduced downtime due to equipment failure, and lower maintenance costs compared to traditional methods. Additionally, the equipment helps maintain a safe working environment by minimizing exposure to harmful powders and preventing dust explosions.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in providing high-quality powder conveying solutions tailored to the needs of desulfurization and denitrification applications. With a focus on innovation and customer satisfaction, the company has developed advanced equipment that meets the stringent requirements of modern industrial processes. The company’s products are designed to enhance operational efficiency, ensure environmental compliance, and reduce overall costs for clients. HeadPowder Engineering’s commitment to quality and reliability has made it a trusted partner for industries worldwide.




