HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced material handling solutions. The company's expertise lies in optimizing bulk material transport systems, particularly for industrial applications like the handling of borax. This article explores the application of pneumatic conveying systems in the efficient and reliable transportation of borax, a critical chemical used in various industries.
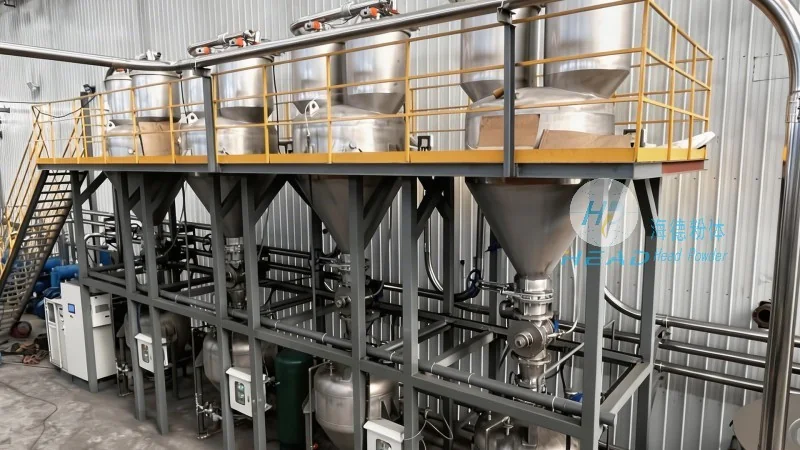
Understanding Pneumatic Conveying Systems
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials through a pipeline using pressurized or vacuum air. This technology offers a flexible and efficient solution for moving dry powders and granules, such as borax, from one location to another within a production facility. Unlike traditional mechanical conveying systems, pneumatic conveyors eliminate the need for moving parts in the material path, reducing maintenance requirements and enhancing operational safety.
Advantages of Pneumatic Conveying for Borax Handling
When it comes to handling borax, a fine white powder with moderate dust generation characteristics, pneumatic conveying systems provide several key advantages. First, they offer a dust-free environment, which is crucial for maintaining product purity and ensuring compliance with industrial hygiene standards. The enclosed pipeline system prevents contamination from external sources and minimizes the risk of product degradation due to exposure to air or moisture.
Second, pneumatic conveyors enable high-velocity transport, allowing for rapid movement of borax between processing stages. This improves overall production throughput and reduces downtime associated with material handling. Additionally, the system's flexibility allows for multiple pickup and discharge points, making it suitable for complex production layouts where materials need to be routed to different destinations.
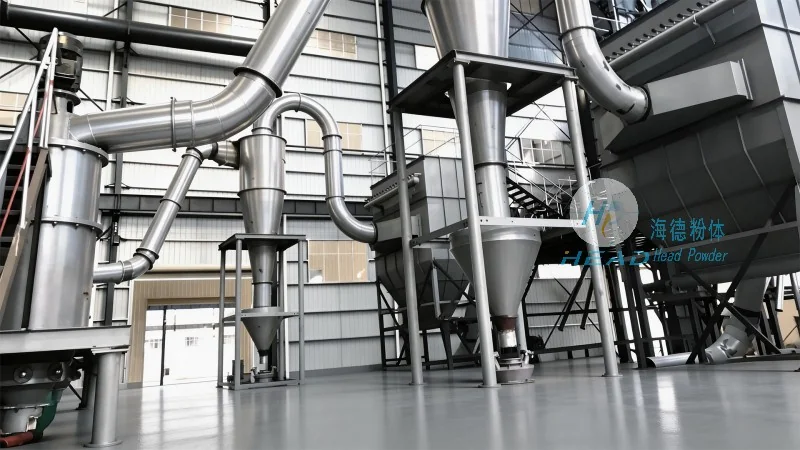
Application in Borax Production and Processing
In the borax production process, pneumatic conveying is commonly used to transport raw borax from storage silos to processing equipment, such as grinding mills or reactors. The system can handle both bulk and bagged materials, providing a seamless transition from storage to production. For example, in a typical borax processing plant, the material is first stored in a silo, then conveyed pneumatically to a grinding unit where it is reduced to a finer powder. The conveyed powder is then directed to a reactor for further chemical processing.
During the conveying process, the system maintains consistent material flow rates, ensuring that the processing equipment operates at optimal efficiency. The use of positive pressure systems, where air is forced through the pipeline, allows for reliable transport even over long distances or with multiple bends and changes in elevation. This capability is essential for large-scale borax production facilities that require extensive material movement across the plant floor.
Technical Considerations and System Design
The successful implementation of a pneumatic conveying system for borax handling requires careful consideration of several technical factors. Material properties, such as particle size, density, and moisture content, play a significant role in determining the most suitable conveying method. For borax, which has a relatively low bulk density and fine particle size, a positive pressure system with high air velocity is often preferred to prevent clogging and ensure smooth flow.
System design also involves selecting appropriate pipeline materials and components. Borax is a mildly corrosive material, so the conveying system must be constructed from materials that resist chemical attack, such as stainless steel or specialized coatings. The selection of air compressors and control valves is critical to maintaining consistent pressure and flow rates, which directly impact the efficiency of the conveying process.
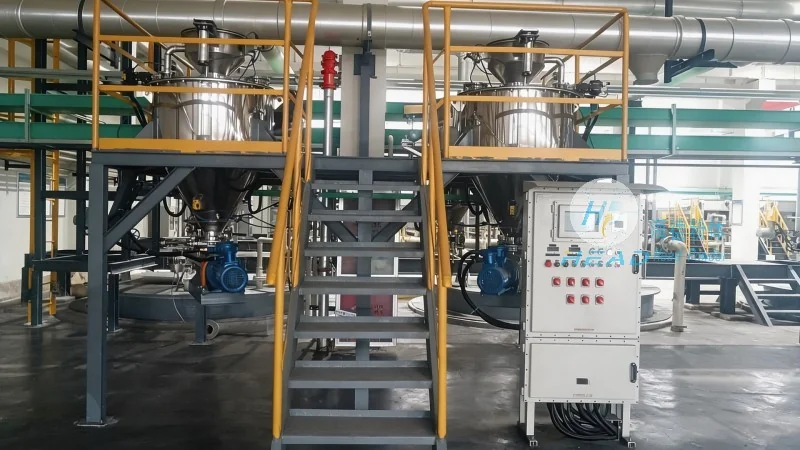
Operational Benefits and Cost Efficiency
Implementing a pneumatic conveying system for borax handling offers several operational benefits. The enclosed system reduces dust emissions, improving workplace safety and environmental compliance. It also minimizes product loss and contamination, leading to higher product quality and reduced waste. From a cost perspective, the elimination of mechanical components reduces maintenance costs and extends the lifespan of the equipment.
Furthermore, the flexibility of pneumatic conveying allows for easy integration with existing production lines, minimizing disruption during system upgrades or expansions. This adaptability is particularly valuable for borax manufacturers who may need to adjust their production capacity or product specifications over time.
Conclusion
HeadPowder Engineering Co., Ltd., based in Shandong, China, provides comprehensive solutions for pneumatic conveying systems tailored to the specific needs of borax handling applications. By leveraging advanced engineering and material handling expertise, the company helps borax producers optimize their operations, enhance product quality, and improve overall efficiency. The application of pneumatic conveying technology in bulk handling of borax demonstrates its effectiveness as a reliable and efficient solution for modern industrial processing needs.




