Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in the design and implementation of advanced pneumatic conveying solutions tailored for handling dusty bulk materials. With a focus on industrial applications involving fine powders and particulate matter, the company's expertise lies in optimizing material transport processes while ensuring efficiency, safety, and environmental compliance. This article explores the practical applications and technical advantages of pneumatic conveying systems in managing dusty bulk materials, highlighting how such systems enhance operational productivity and reduce handling risks.
Understanding Pneumatic Conveying Technology
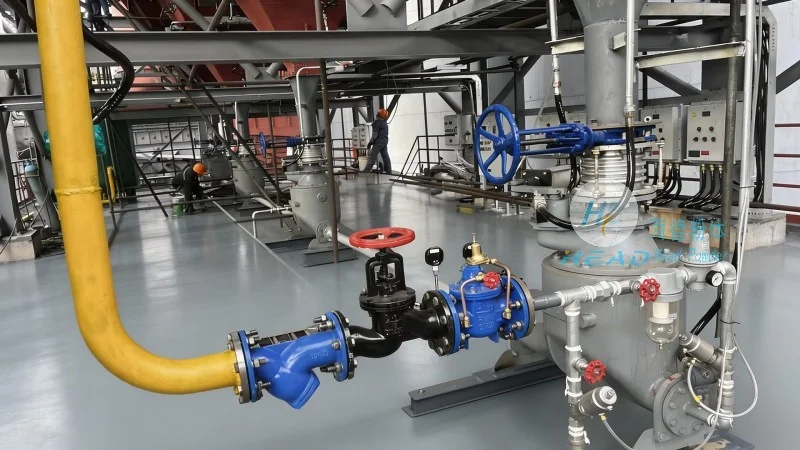
Pneumatic conveying, also known as air-pneumatic transport, is a method of transporting bulk materials through a pipeline using pressurized or vacuum air. In the context of dusty materials, this technology is particularly effective due to its ability to handle fine powders and particulates that are prone to dust generation and dispersion. The system typically consists of a hopper, a conveyor line, and a receiver, with air being introduced to create a flow that moves the material through the pipeline. For dusty applications, specialized equipment such as cyclone separators and dust collectors are integrated to maintain air quality and prevent material loss.
Key Benefits of Pneumatic Conveying for Dusty Bulk Materials
Implementing pneumatic conveying systems for dusty bulk materials offers several critical advantages. Firstly, it significantly reduces the risk of dust exposure and related health hazards, as the material is contained within the pipeline rather than being released into the environment. This not only improves workplace safety but also complies with environmental regulations regarding particulate emissions. Secondly, the technology enhances material handling efficiency by minimizing downtime and labor costs associated with manual or mechanical handling. The continuous flow of material through the system ensures a steady supply to processing units, such as reactors or mixers, without interruptions. Additionally, pneumatic conveying systems are highly adaptable, allowing for the transport of various materials, including powders, granules, and pellets, with minimal modifications to the equipment.
Applications in Industrial Settings
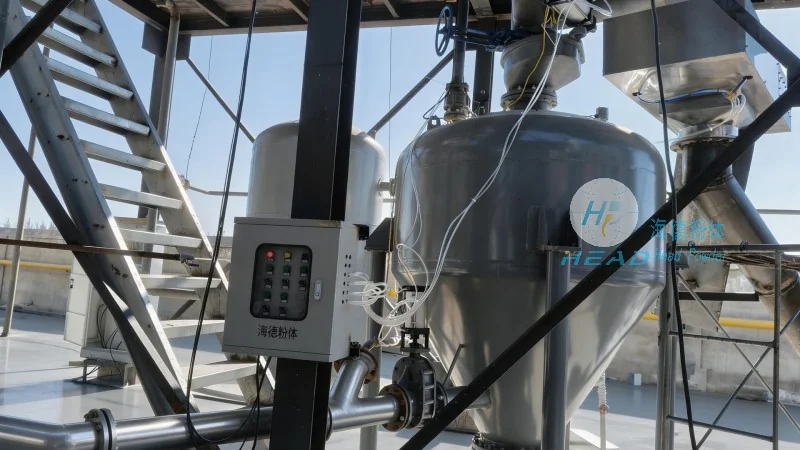
In industrial settings, pneumatic conveying is widely used in sectors that deal with dusty bulk materials, such as chemical manufacturing, food processing, and pharmaceuticals. For example, in chemical plants, the system is employed to transport raw materials like limestone or coal dust to reactors, ensuring a consistent feed rate that optimizes production yields. In food processing facilities, pneumatic conveying is used to handle ingredients like flour or sugar, maintaining hygiene standards and preventing contamination. The technology is also beneficial in pharmaceutical industries, where dust control is paramount to ensure product purity and regulatory compliance. Furthermore, in mining operations, pneumatic conveying systems are utilized to transport ore dust from processing plants to storage or transportation facilities, reducing the need for heavy machinery and manual labor.
Technical Considerations for Dusty Material Handling
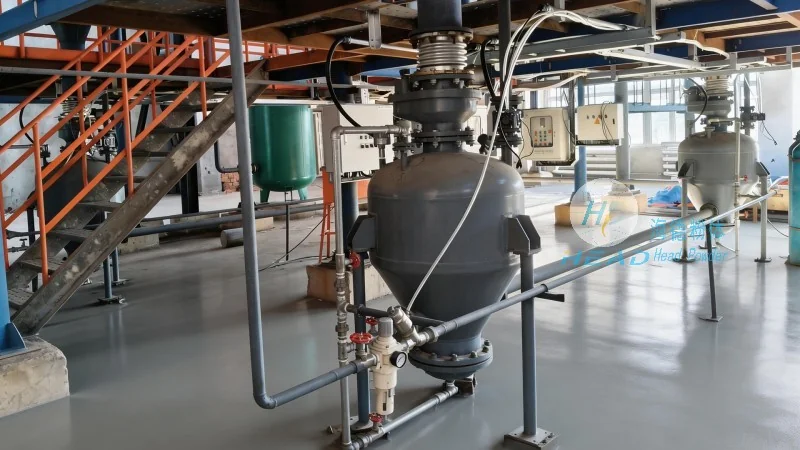
When designing pneumatic conveying systems for dusty bulk materials, several technical factors must be considered to ensure optimal performance. The first is the material's properties, including its density, flowability, and dustiness. Materials with high dust content require higher air velocities and more robust filtration systems to prevent clogging and maintain air quality. The second consideration is the system's pressure and vacuum levels, which must be adjusted based on the material's characteristics and the distance to be transported. For longer distances or higher material loads, positive pressure systems are preferred, while vacuum systems are suitable for shorter distances or when material is being collected from multiple sources. Additionally, the design of the pipeline, including the diameter and bends, plays a crucial role in minimizing pressure losses and preventing material buildup. Proper maintenance, such as regular cleaning of cyclone separators and filters, is essential to ensure the system operates efficiently over time.
Case Study: Enhancing Efficiency in a Chemical Plant
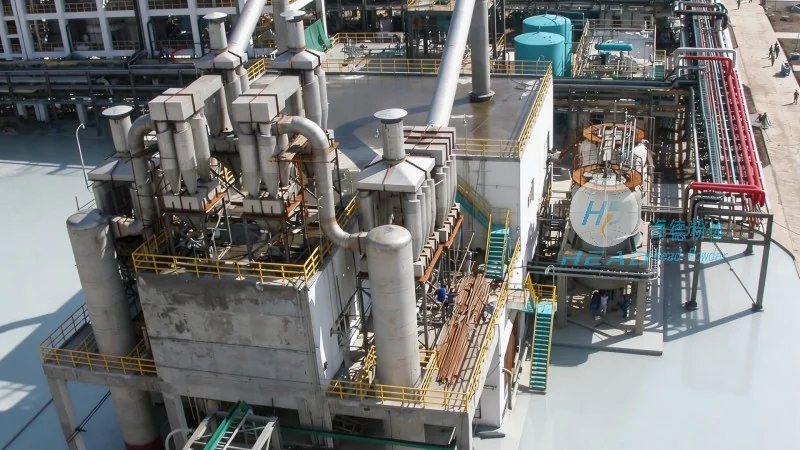
One of the notable applications of pneumatic conveying in dusty bulk material handling is demonstrated in a chemical manufacturing plant in China. The plant processes raw materials like calcium carbonate, which is a fine powder with high dust generation potential. Prior to implementing a pneumatic conveying system, the plant relied on manual handling and bucket elevators, leading to frequent dust exposure and material loss. After installing a headpowder-designed system, the plant experienced a 40% reduction in material handling time and a 30% decrease in dust emissions. The system's positive pressure design ensured a consistent flow of material to the reactors, improving production efficiency by 25%. The plant also reported a significant reduction in labor costs and improved workplace safety, as the material was contained within the pipeline and the risk of dust inhalation was minimized.
Conclusion and Company Overview
Shandong HeadPowder Engineering Co., Ltd. continues to lead in the development of advanced pneumatic conveying solutions for dusty bulk materials, leveraging its expertise to meet the evolving needs of industrial sectors. By focusing on efficient, safe, and environmentally friendly material transport, the company's systems enhance operational productivity while adhering to industry standards. With a strong presence in China, headpowder's commitment to quality and innovation ensures that its customers receive reliable and effective solutions for their dusty material handling challenges. The company's address in Shandong, China, serves as a base for providing localized support and tailored solutions to meet the specific requirements of each industrial application.




