HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and development of advanced negative pressure pneumatic conveying systems tailored for corn processing applications. This article provides an in-depth look at the design principles, operational advantages, and practical applications of such equipment, highlighting how it enhances efficiency and reliability in corn handling operations.
Introduction to Negative Pressure Pneumatic Conveying for Corn
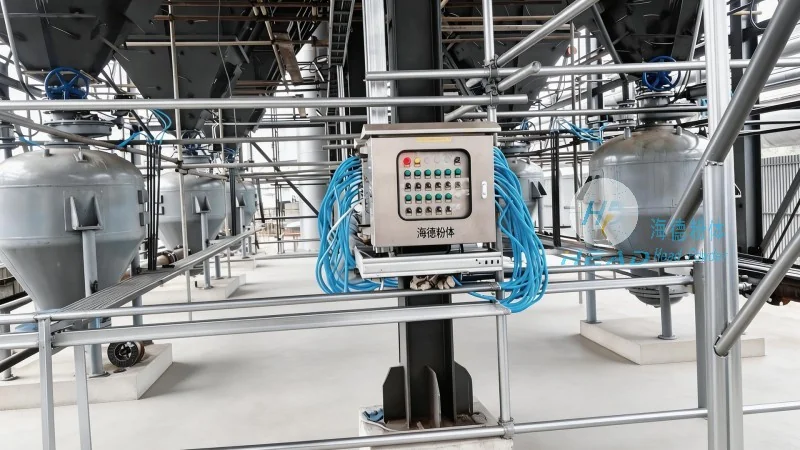
Negative pressure pneumatic conveying is a sophisticated method for transporting bulk materials like corn from one location to another using air as the conveying medium. Unlike positive pressure systems that force air and material through a pipeline, negative pressure systems draw material into the system using a vacuum or reduced pressure at the receiving end. This approach offers several key benefits for corn handling, including reduced dust generation, lower energy consumption, and improved material containment. The design of a corn negative pressure pneumatic conveying system must consider factors such as corn grain size, moisture content, and the distance to be covered, ensuring optimal performance and minimal material degradation.
HeadPowder's Expertise in Corn Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. leverages years of experience in bulk material handling to deliver customized corn negative pressure pneumatic conveying equipment. The company's engineering team works closely with clients to understand their specific operational requirements, from small-scale farm operations to large industrial corn processing facilities. By integrating advanced design software and material testing protocols, HeadPowder ensures that each system is optimized for the unique characteristics of corn, such as its density, flowability, and susceptibility to breakage during transport.
Key Design Features of the Corn Negative Pressure Pneumatic Conveying System
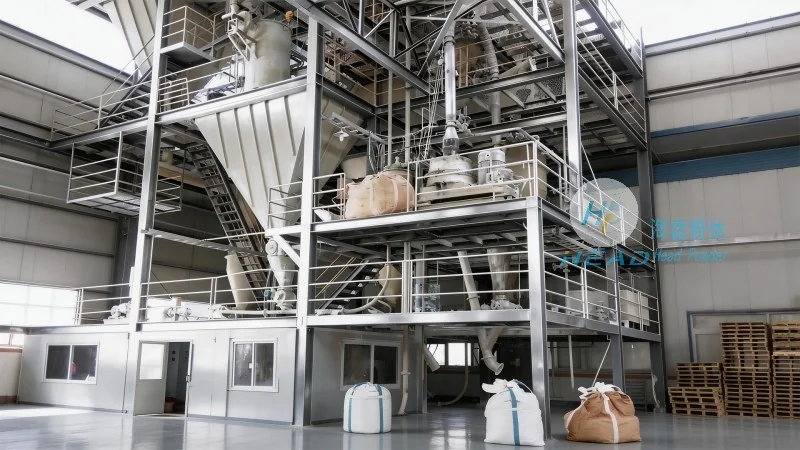
The core components of a corn negative pressure pneumatic conveying system include a vacuum pump, a material feed hopper, a conveying pipeline, and a receiving hopper. The vacuum pump creates a pressure differential that draws corn from the feed hopper into the pipeline. The system is designed with smooth, corrosion-resistant pipelines to prevent material buildup and ensure consistent flow. HeadPowder’s designs incorporate features like adjustable feed valves and pressure sensors to maintain optimal conveying rates and prevent overloading. Additionally, the system is equipped with dust collection and filtration units to comply with environmental regulations and maintain a clean working environment.
Operational Advantages and Efficiency
Implementing a negative pressure pneumatic conveying system for corn processing offers significant operational advantages. The reduced energy consumption compared to positive pressure systems translates to lower operational costs over time. The system’s ability to handle corn with minimal breakage preserves grain quality, which is critical for both animal feed and human consumption. Furthermore, the enclosed design minimizes dust exposure, improving workplace safety and reducing the risk of fire hazards in grain storage areas. These benefits make the negative pressure system an attractive choice for corn producers and processors seeking to enhance their productivity while maintaining high standards of material integrity.
Application Scenarios and Scalability
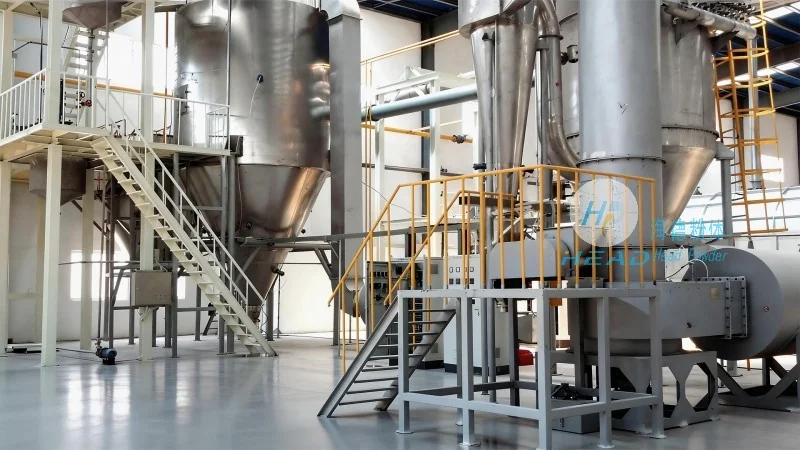
The corn negative pressure pneumatic conveying equipment from HeadPowder is versatile and can be adapted to various application scenarios. For example, it can be used to transport corn from storage silos to processing lines, or to move finished products from the processing plant to packaging areas. The system’s modular design allows for easy expansion as production scales up, ensuring that the equipment can grow with the business. Whether for a small-scale farm operation or a large industrial facility, HeadPowder’s solutions are designed to meet the specific needs of each client, providing reliable and efficient corn handling solutions.
Quality Assurance and After-Sales Support
HeadPowder is committed to delivering high-quality corn negative pressure pneumatic conveying systems that meet or exceed industry standards. The company adheres to rigorous quality control processes, including material testing, system testing, and performance validation, to ensure that each unit operates as intended. After the equipment is installed and commissioned, HeadPowder provides comprehensive after-sales support, including training for operators, routine maintenance services, and technical assistance. This commitment to customer satisfaction ensures that clients can rely on their corn conveying systems for long-term, trouble-free operation.




