Efficient material handling is a critical concern in industries dealing with powders and particulate materials, such as activated carbon. Traditional methods like manual handling or mechanical conveyors often face challenges related to dust, contamination, and operational inefficiencies. Pneumatic conveying offers a modern solution to these issues, enabling the safe and effective transport of bulk materials through the use of air pressure. This article explores the principles and applications of pneumatic conveying for activated carbon, highlighting how specialized systems can optimize material movement in industrial settings.
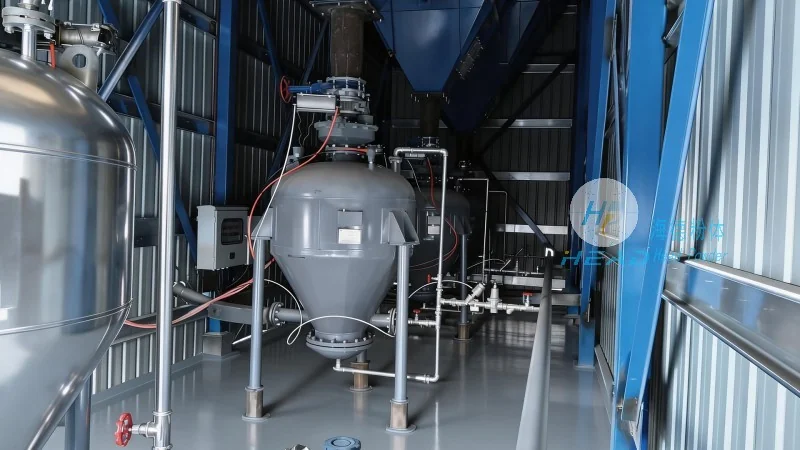
Pneumatic Conveying Technology: The Core of Efficient Material Transport
Pneumatic conveying systems utilize air flow to move powders and granular materials from one location to another. Unlike traditional methods, this technology eliminates the need for mechanical components that can cause wear and tear or introduce contaminants. The process involves creating a pressure differential, either by using positive pressure (where air is forced into the system) or negative pressure (where air is drawn out), to propel the material through a pipeline. For activated carbon, which is often used in filtration and adsorption processes, maintaining purity and preventing dust dispersion is paramount. Pneumatic conveying systems are designed to achieve this by controlling air velocity and pressure, ensuring that the material remains intact and free from contamination.
Key Benefits of Pneumatic Conveying for Activated Carbon Handling
Implementing pneumatic conveying for activated carbon offers several advantages that enhance operational efficiency and product quality. First, it significantly reduces the risk of dust exposure, which is a major health and safety concern in industrial environments. By containing the material within a sealed system, the risk of airborne particles is minimized, leading to a safer working environment. Second, pneumatic conveying systems can handle a wide range of material characteristics, including varying particle sizes and moisture content, without compromising performance. This flexibility makes them suitable for diverse applications, from small-scale laboratory use to large-scale industrial production. Third, the technology can improve overall process efficiency by reducing downtime and maintenance costs. Unlike mechanical conveyors that require regular cleaning and lubrication, pneumatic systems operate with minimal moving parts, leading to lower operational expenses over time.
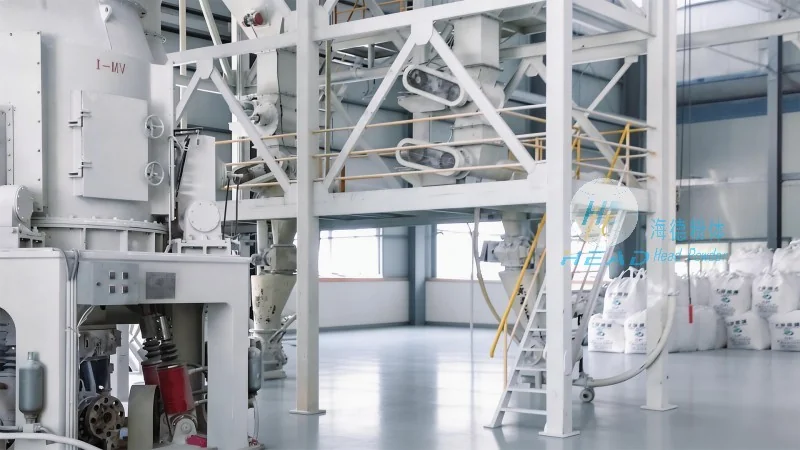
HeadPowder: A Leader in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a prominent player in the material handling industry, specializes in providing customized pneumatic conveying solutions tailored to the needs of activated carbon and other powders. With a strong focus on innovation and quality, HeadPowder has developed advanced systems that address the unique challenges of transporting activated carbon. The company’s expertise lies in designing and manufacturing equipment that ensures optimal material flow, minimal degradation, and compliance with industry standards. By leveraging years of experience and cutting-edge technology, HeadPowder delivers reliable and efficient pneumatic conveying systems that enhance productivity and safety for its clients.
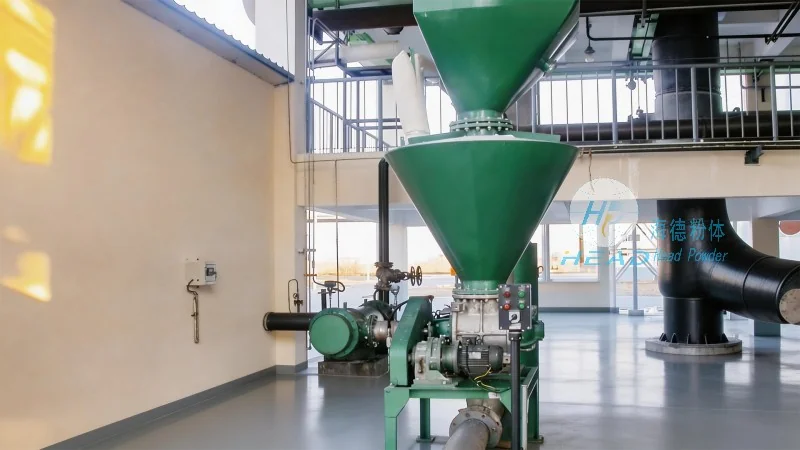
Customization and Application Flexibility
HeadPowder understands that each industrial application has distinct requirements. Therefore, the company offers customized pneumatic conveying solutions that can be tailored to specific operational needs. Whether it involves short-distance transport within a facility or long-distance transfer between production sites, HeadPowder’s systems are designed to meet these demands. The company’s engineers work closely with clients to assess their material characteristics, processing requirements, and environmental considerations to develop a solution that maximizes efficiency and minimizes costs. This approach ensures that the final system is not only effective but also scalable, allowing for future expansion as business needs evolve.
Ensuring Quality and Compliance
Quality is a top priority at HeadPowder. The company adheres to strict manufacturing standards and quality control measures to ensure that its pneumatic conveying systems meet or exceed industry expectations. All components are rigorously tested to ensure durability and performance under various operating conditions. Additionally, HeadPowder’s systems are designed to comply with relevant safety and environmental regulations, providing clients with peace of mind regarding regulatory compliance. By using high-quality materials and advanced manufacturing techniques, the company ensures that its products deliver consistent performance and longevity, contributing to the overall reliability of the material handling process.




