Stearic acid sodium, a key chemical component utilized across diverse industrial sectors including cosmetics, pharmaceuticals, and food processing, requires efficient and reliable handling systems to preserve its quality and performance. The pneumatic conveying system engineered by Shandong HeadPowder Engineering Co., Ltd. (HeadPowder) addresses these critical needs by delivering a sophisticated solution for transporting stearic acid sodium with precision, minimal loss, and enhanced safety. This system leverages advanced engineering principles and material handling expertise to provide a high-performance solution tailored to the specific demands of modern industrial processes.
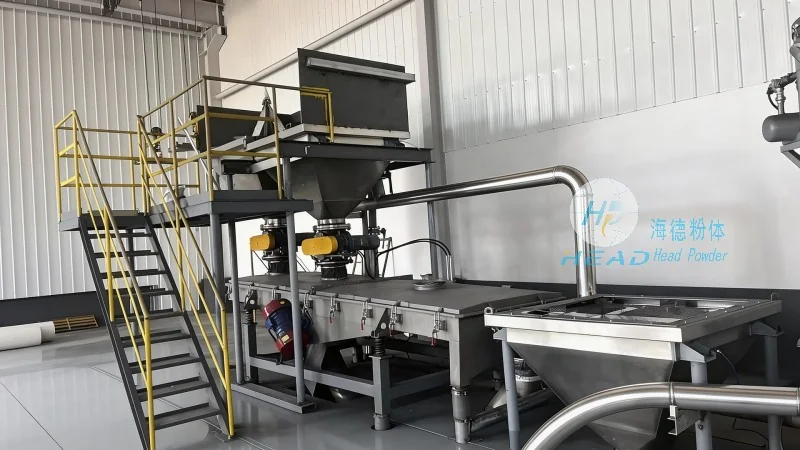
Company Overview: HeadPowder Engineering
HeadPowder Engineering, a prominent engineering firm headquartered in Shandong, China, specializes in the design, development, and implementation of advanced material handling systems. With a strong focus on innovation and quality, the company has established itself as a trusted partner for industries seeking efficient and reliable solutions for chemical and powder transport. The firm’s expertise in pneumatic conveying technology, combined with its deep understanding of material properties and process requirements, enables it to develop customized systems that meet the unique demands of clients across various sectors, including manufacturing, pharmaceuticals, and food processing.
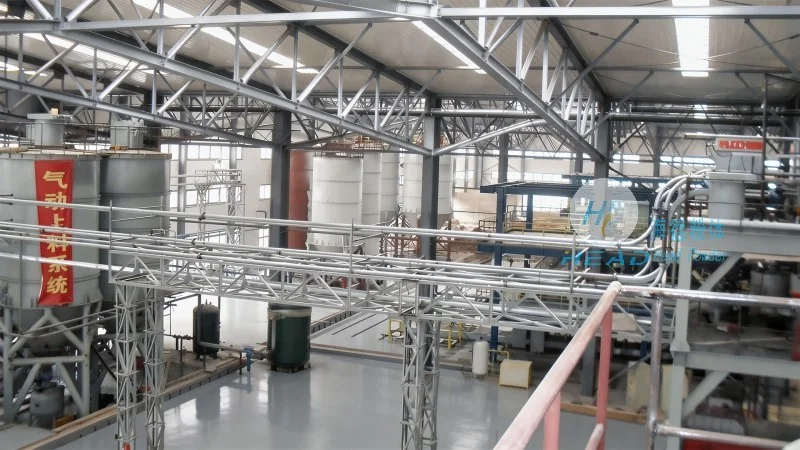
System Design Principles and Core Components
The pneumatic conveying system for stearic acid sodium is engineered based on robust design principles that prioritize efficiency, reliability, and safety. Key components of the system include a large-capacity hopper for material storage, a rotary airlock valve for controlled and continuous discharge, a high-quality conveying line with appropriate ductwork and air distribution, and a receiving hopper or silo for product collection. The system operates using either positive or negative pressure, depending on the specific application and material characteristics, ensuring smooth and unidirectional transport of the stearic acid sodium. The design incorporates advanced air filtration and moisture control mechanisms to prevent product degradation and maintain its purity during transit. Additionally, the system is equipped with real-time monitoring and control interfaces, allowing operators to adjust parameters such as air pressure, flow rate, and material feed rate to optimize performance and address any operational challenges.
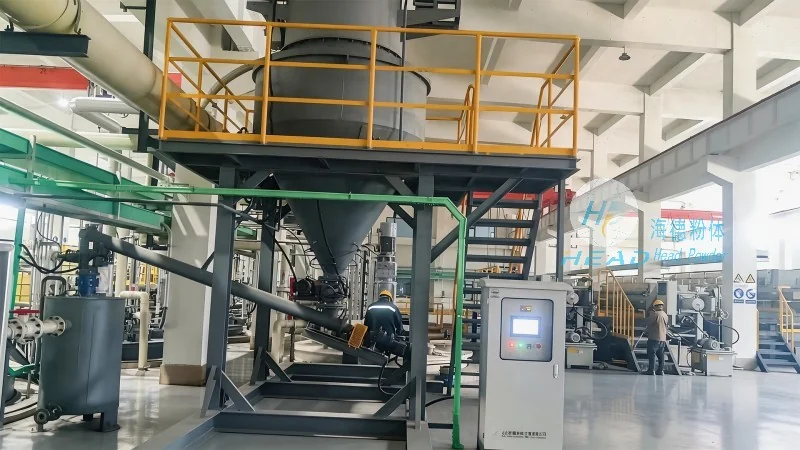
Advantages of the Pneumatic Conveying System
Adopting a pneumatic conveying system for stearic acid sodium offers numerous advantages over traditional methods such as bucket elevators or belt conveyors. Firstly, the enclosed system minimizes the risk of product contamination from external sources, ensuring the purity of the stearic acid sodium, which is critical for applications in pharmaceuticals and food industries. Secondly, the system provides a continuous and controlled flow of material, significantly improving production throughput and reducing downtime associated with manual handling or equipment maintenance. Thirdly, the system’s flexibility allows for easy integration with existing production lines, enabling seamless upgrades or expansions without disrupting ongoing operations. Furthermore, the system’s ability to handle fine powders without clogging or degradation enhances operational efficiency and reduces the need for frequent maintenance.
Application Examples and Industry Impact
The stearic acid sodium pneumatic conveying system is particularly valuable in industries where the integrity and purity of the material are paramount. In the pharmaceutical sector, for instance, the system helps maintain the sterility of the stearic acid sodium, which is essential for meeting stringent regulatory standards and ensuring the safety of end products. Similarly, in the cosmetics industry, the system’s ability to handle powders without cross-contamination supports the production of high-quality formulations. In the food processing industry, the system contributes to food safety by preventing contamination and maintaining the quality of ingredients used in various products. The system’s adaptability also makes it suitable for different production scales, from small-scale batch production to large-scale manufacturing, providing a versatile solution that can grow with the client’s business needs.
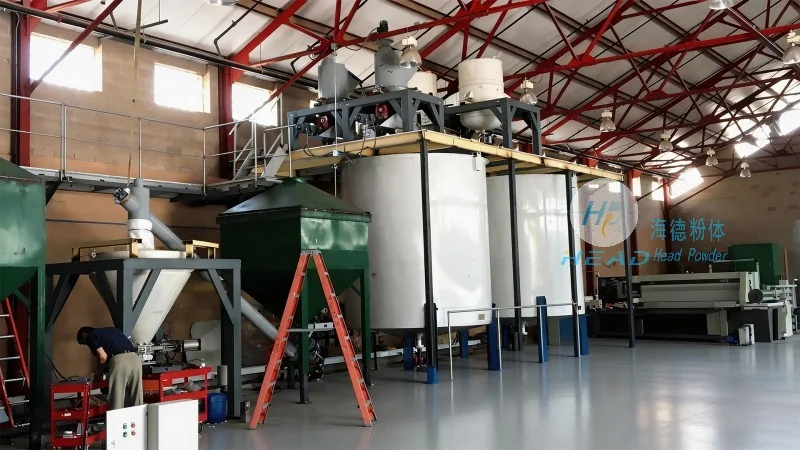
Customization and After-Sales Support
HeadPowder Engineering recognizes that each client’s operational environment and material handling requirements are unique, and therefore, offers comprehensive customization services to tailor the pneumatic conveying system to specific needs. The company’s engineering team works closely with clients to conduct thorough assessments of their processes, identify challenges, and design a system that optimizes performance, reduces costs, and enhances overall efficiency. Additionally, HeadPowder provides a full range of after-sales support services, including professional installation, commissioning, and ongoing maintenance. This ensures that the system operates at peak efficiency throughout its lifecycle, minimizing downtime and maximizing the return on investment. The company’s commitment to customer satisfaction and technical excellence has established it as a reliable partner in the material handling industry, with a track record of delivering high-quality solutions that meet and exceed client expectations.




