HeadPowder, a leading enterprise in the field of material handling solutions, specializes in the design, manufacturing, and supply of advanced pneumatic conveying systems tailored for various industrial applications. This article provides an overview of red sugar pneumatic conveying equipment, detailing its structural components and operational principles to help users understand its functionality and benefits.
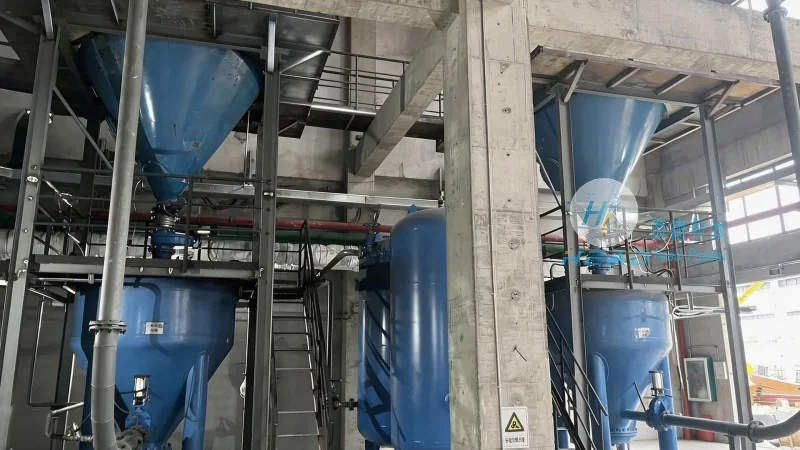
Company Profile and Background
HeadPowder, also known as Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. With years of experience in the engineering and manufacturing sector, the company has established itself as a reliable partner for industries requiring efficient and reliable material transport solutions. The company's commitment to quality, innovation, and customer satisfaction has enabled it to serve a wide range of clients across different sectors, including food processing, chemical manufacturing, and pharmaceutical industries.
Understanding Pneumatic Conveying Systems
Pneumatic conveying systems are mechanical devices that use air or other gases to transport bulk materials from one location to another. These systems are widely used in industries where traditional methods like belt conveyors or bucket elevators may not be suitable due to material characteristics such as dustiness, moisture content, or the need for enclosed transport to prevent contamination. For red sugar, a product that is often granular and can be prone to dust, pneumatic conveying offers a hygienic and efficient solution.
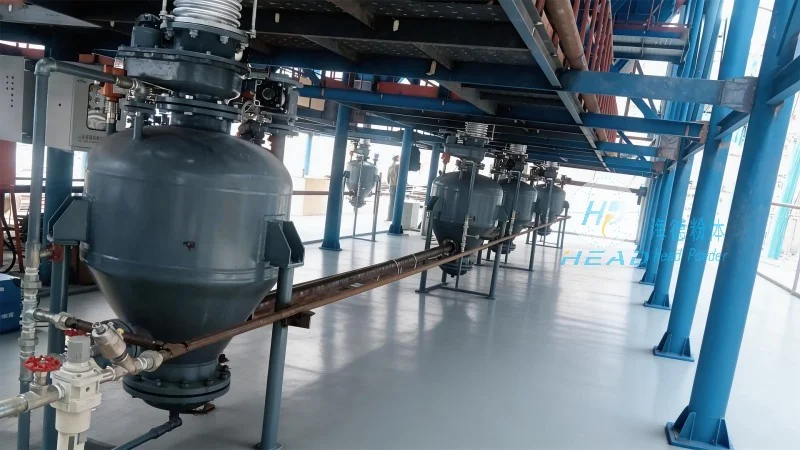
Key Components of Red Sugar Pneumatic Conveying Equipment
The red sugar pneumatic conveying system consists of several critical components that work in tandem to ensure smooth and effective material transport. These components include:
- Feeder: The feeder is responsible for feeding the red sugar into the conveying line at a controlled rate. It ensures a consistent flow of material, preventing blockages and maintaining system efficiency.
- Conveying Pipe: The main body of the system, the conveying pipe is where the red sugar is transported. It is typically made of materials such as stainless steel or food-grade plastic to ensure durability and hygiene. The pipe is designed to handle the specific characteristics of red sugar, including its granular size and potential for dust generation.
- Air Supply System: This component generates the necessary air pressure or vacuum to move the red sugar through the pipe. It includes a blower or compressor, filters, and regulators to maintain optimal air quality and pressure levels.
- Separation and Collection Units: These units are used to separate the conveyed material from the air and collect it in a designated container. For red sugar, this may include cyclones or filters to ensure that the product is collected without any contamination from the air.
- Control System: The control system monitors and regulates the operation of the entire conveying process. It includes sensors, valves, and a control panel to adjust parameters such as air pressure, material flow rate, and system speed, ensuring safe and efficient operation.
Working Principle of the Red Sugar Pneumatic Conveying System
The operation of the red sugar pneumatic conveying system is based on the principle of fluidization and suspension. The feeder introduces the red sugar into the conveying pipe, and the air supply system generates a flow of air that moves through the pipe. As the air flows, it creates a low-pressure zone that draws the red sugar particles into the air stream, causing them to become suspended and transported along the pipe. The separation units then remove the red sugar from the air stream, collecting it in a container. The control system continuously monitors the process, adjusting the air flow and material feed rate to maintain optimal performance.
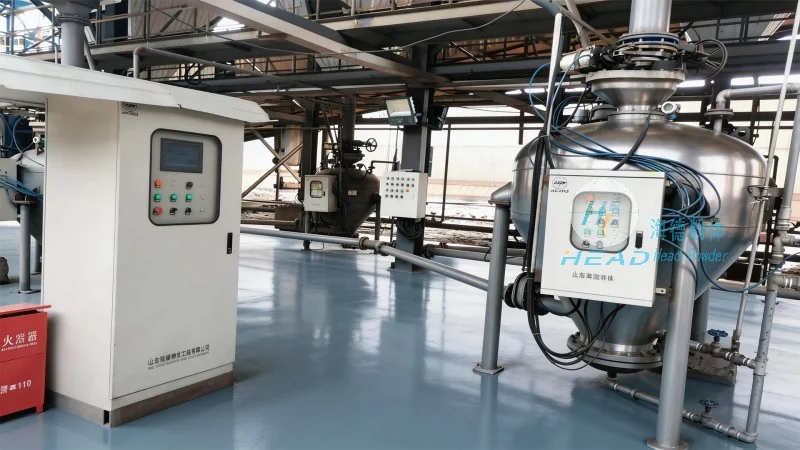
Advantages of Using Red Sugar Pneumatic Conveying Equipment
There are several advantages to using pneumatic conveying systems for red sugar transport. These include:
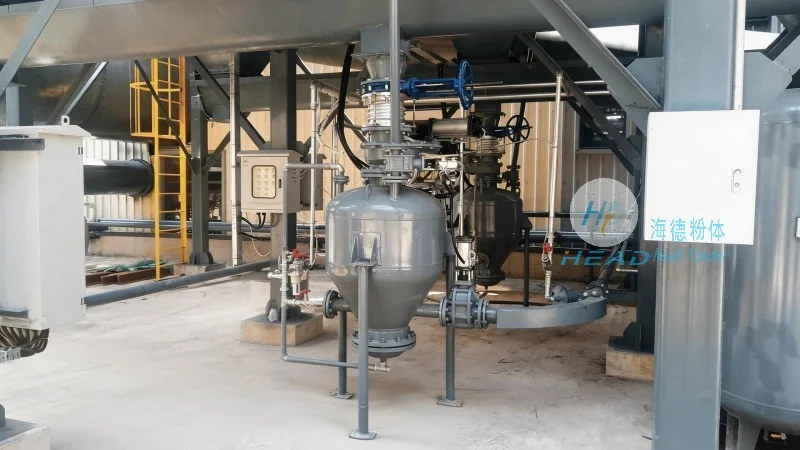
- Hygienic and Clean Operation: The enclosed system prevents contamination from the environment, ensuring that the red sugar remains clean and free from dust or other particles.
- Efficient and High Capacity: Pneumatic conveying can handle large volumes of material at high speeds, reducing the time and labor required for transport.
- Flexible and Versatile: The system can be easily adapted to different production requirements, including changes in material flow rates or destination points.
- Low Maintenance: Compared to traditional conveyor systems, pneumatic conveying systems have fewer moving parts, resulting in lower maintenance costs and longer service life.
- Energy Efficient: Modern pneumatic conveying systems are designed to be energy efficient, reducing operational costs and environmental impact.
Application Scenarios and Industry Use Cases
Red sugar pneumatic conveying equipment is widely used in various industries where red sugar is processed or transported. Some common applications include:
- Food Processing Plants: In food processing facilities, the system is used to transport red sugar from storage silos to production lines or packaging areas, ensuring a clean and efficient supply chain.
- Chemical Manufacturing: In chemical plants, the system can be used to transport red sugar as a raw material or intermediate product, maintaining the integrity of the material and preventing contamination.
- Pharmaceutical Industries: In pharmaceutical manufacturing, the system is used to transport red sugar as an excipient or ingredient, adhering to strict hygiene and quality standards.
- Storage and Distribution Centers: In storage and distribution centers, the system can be used to move red sugar from storage bins to loading areas, facilitating efficient inventory management and order fulfillment.
Conclusion and Company Commitment
Red sugar pneumatic conveying equipment is a highly effective and efficient solution for transporting red sugar in various industrial applications. With its advanced design and robust construction, the system offers numerous benefits, including hygienic operation, high capacity, and low maintenance. HeadPowder, with its expertise and commitment to quality, provides reliable and customized pneumatic conveying solutions that meet the specific needs of its clients. By leveraging the latest technology and engineering principles, HeadPowder ensures that its customers receive the best possible material handling solutions for their red sugar transport requirements.




