For industrial applications involving the efficient and reliable transport of fertilizer granules, pneumatic conveying systems offer a robust and flexible solution. This article explores the key aspects of fertilizer granule pneumatic conveying, highlighting the technology's benefits and the expertise of Shandong HeadPowder Engineering Co., Ltd. in delivering tailored solutions for bulk material handling.
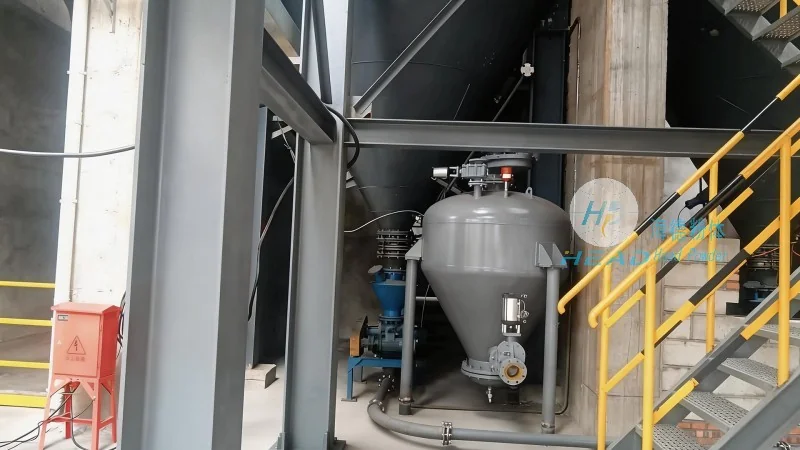
Understanding Pneumatic Conveying for Fertilizer Granules
Pneumatic conveying is a method of transporting bulk materials, such as fertilizer granules, through a pipeline using air or gas as the conveying medium. Unlike traditional mechanical systems, this technology eliminates the need for moving parts in the conveying line, reducing maintenance requirements and enhancing operational reliability. The process involves creating a pressure differential that propels the material through the system, making it suitable for both short and long-distance transport. Key advantages include high material throughput, minimal product degradation, and the ability to handle a wide range of granule sizes and densities.
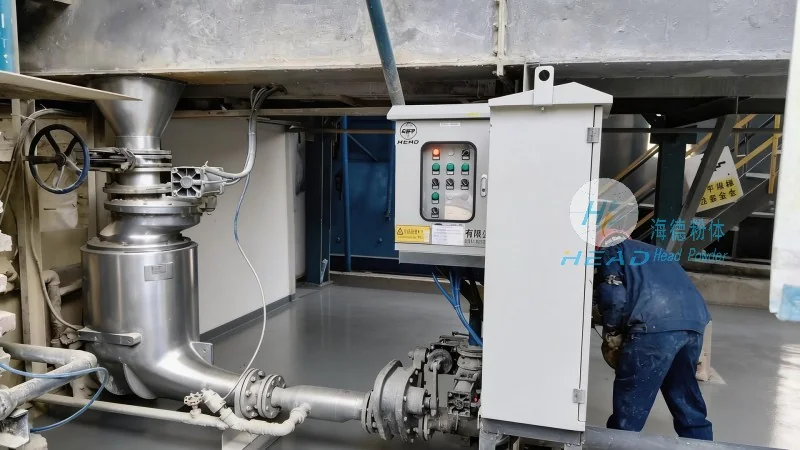
Key Components of Fertilizer Granule Pneumatic Conveying Systems
Effective fertilizer granule pneumatic conveying systems consist of several critical components that work in harmony to ensure optimal performance. These include the feed hopper, which stores and meters the granules; the conveyor line, typically made of durable materials like stainless steel or plastic to resist corrosion and abrasion; the air mover, which generates the necessary pressure or vacuum to transport the material; and the separation and collection equipment, such as cyclones or filters, that separate the conveyed material from the air and return it to the system. Each component is designed to handle the specific characteristics of fertilizer granules, ensuring efficient and clean operation.
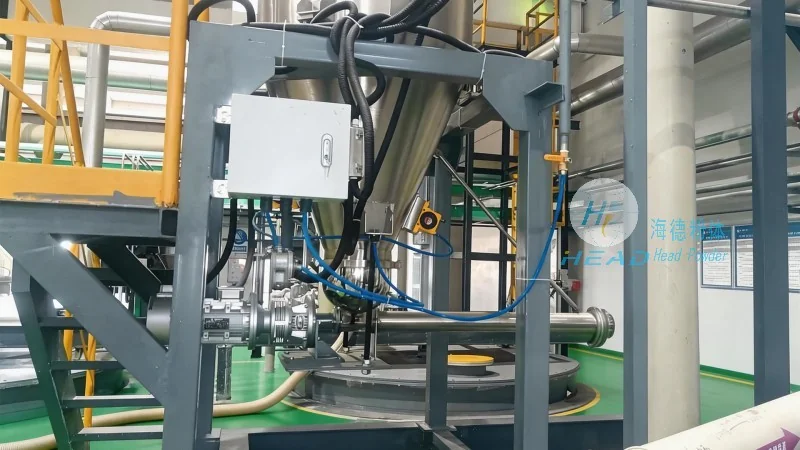
Tailored Solutions by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions, specializes in designing and manufacturing customized pneumatic conveying systems for fertilizer granules. With years of experience in the industry, the company understands the unique challenges associated with transporting fertilizer, including dust control, material flow consistency, and system scalability. By leveraging advanced engineering and material science, HeadPowder offers solutions that meet the specific requirements of clients, whether for small-scale operations or large industrial facilities. The company's commitment to quality and innovation ensures that each system is built to withstand the demands of continuous operation, providing long-term reliability and cost savings.
Benefits of Implementing Pneumatic Conveying for Fertilizer Granules
Adopting pneumatic conveying systems for fertilizer granules brings numerous benefits to industrial operations. First, it significantly improves material handling efficiency by reducing downtime and increasing throughput. The absence of mechanical components minimizes maintenance needs, lowering operational costs and enhancing system uptime. Additionally, the technology helps maintain product quality by preventing contamination and degradation during transport. For fertilizer manufacturers, this translates to better product integrity and customer satisfaction. Furthermore, pneumatic conveying systems are highly adaptable, allowing for easy integration with existing production lines and future expansion. The environmental benefits are also notable, as the closed system reduces dust emissions and improves workplace safety.
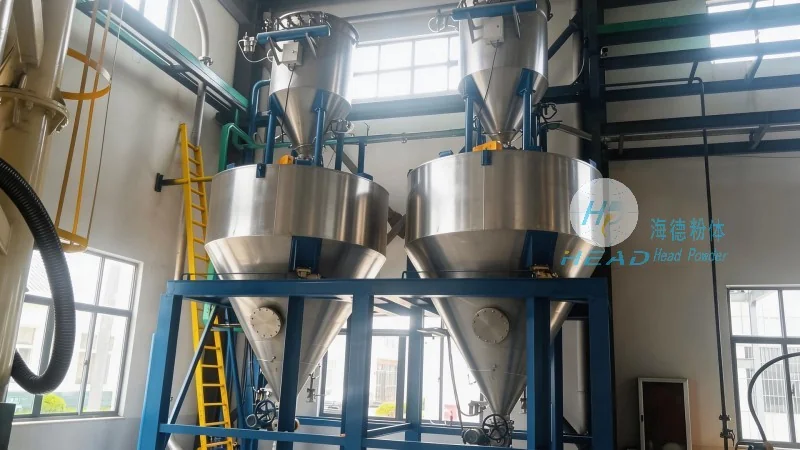
Conclusion and Contact Information
For businesses seeking reliable and efficient solutions for the pneumatic conveying of fertilizer granules, Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner. With a focus on innovation, quality, and customer satisfaction, the company delivers tailored systems that meet the unique needs of each client. By leveraging advanced technology and expert engineering, HeadPowder ensures that its solutions are not only effective but also sustainable and cost-efficient. To learn more about how HeadPowder can enhance your fertilizer handling operations, contact the company at their address in Shandong, China.




