Limestone is a vital industrial material utilized across various sectors, including construction, chemical manufacturing, and environmental treatment. The efficient and reliable transportation of limestone from its source to processing facilities is crucial for maintaining production efficiency and reducing operational costs. Traditional material handling methods, such as belt conveyors or manual handling, often encounter limitations in terms of distance, terrain, and material characteristics. This is where limestone pneumatic conveying systems offer a superior solution, enabling the transport of limestone over extended distances with minimal constraints.
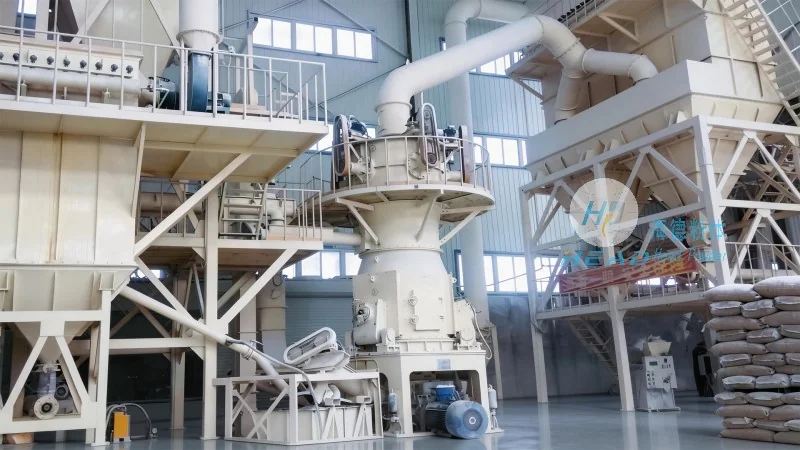
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading engineering company headquartered in Shandong, China, specializes in the design, manufacturing, and installation of advanced material handling systems. With a strong commitment to innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the industry, providing customized solutions tailored to the unique needs of clients. The company's expertise in pneumatic conveying technology, particularly for limestone, has enabled it to deliver high-performance systems that meet the most demanding operational requirements.
Key Features of Limestone Pneumatic Conveying Systems
HeadPowder's limestone pneumatic conveying systems are engineered to provide several key advantages that distinguish them from conventional methods. Firstly, these systems offer the ability to transport limestone over long distances, often exceeding 1000 meters, without the need for intermediate transfer points. This eliminates the need for additional infrastructure and reduces the overall footprint of the material handling process. Secondly, pneumatic conveying is highly efficient in terms of energy consumption, as it minimizes friction and material degradation compared to mechanical conveyors. The systems are also designed to handle a wide range of limestone particle sizes and moisture content, ensuring consistent performance even with varying material characteristics. Additionally, the enclosed nature of pneumatic conveying reduces dust emissions, contributing to a safer and more environmentally friendly operation.
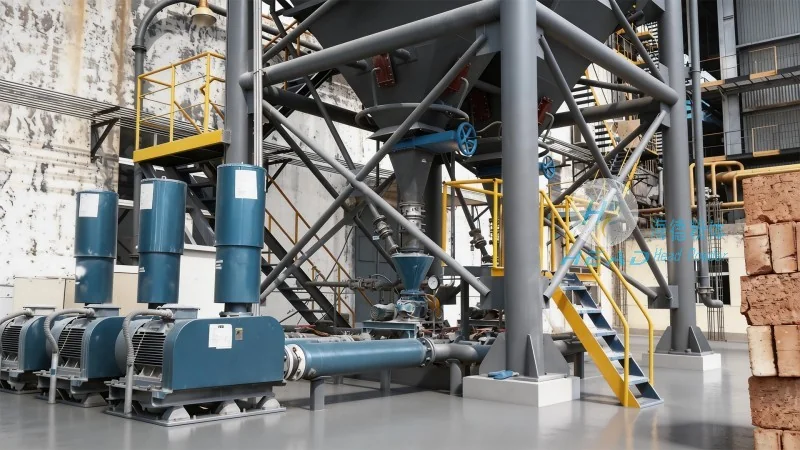
Applications in Industrial Settings
Limestone pneumatic conveying systems are widely used in various industrial applications where the transport of limestone is critical. In the construction industry, these systems are employed to supply limestone to cement plants and concrete mixing facilities, ensuring a steady flow of raw material for production. In the chemical industry, limestone is used as a raw material in the production of calcium carbonate and other chemical products, and pneumatic conveying facilitates the efficient transfer of these materials between processing stages. Environmental treatment facilities also benefit from these systems, as limestone is used in flue gas desulfurization processes to neutralize acidic emissions. The ability of HeadPowder's systems to handle large volumes of limestone at high speeds makes them ideal for these applications, supporting the continuous operation of industrial plants.
Advantages Over Traditional Conveying Methods
Compared to traditional belt conveyors or screw conveyors, limestone pneumatic conveying systems offer several distinct advantages. Belt conveyors are often limited by the distance they can cover and may require multiple segments for long-distance transport, increasing complexity and maintenance costs. Screw conveyors, while suitable for some materials, can cause material degradation and are less effective for handling limestone with high moisture content or abrasive particles. Pneumatic conveying, on the other hand, is not constrained by distance or terrain, as it uses air pressure to move material through a pipeline. This flexibility allows for the design of systems that can adapt to complex layouts, including vertical lifts and horizontal curves. Furthermore, the enclosed system reduces dust exposure for workers, improving workplace safety and compliance with environmental regulations. The reduced need for regular maintenance and lower energy consumption also contribute to long-term cost savings for industrial operations.
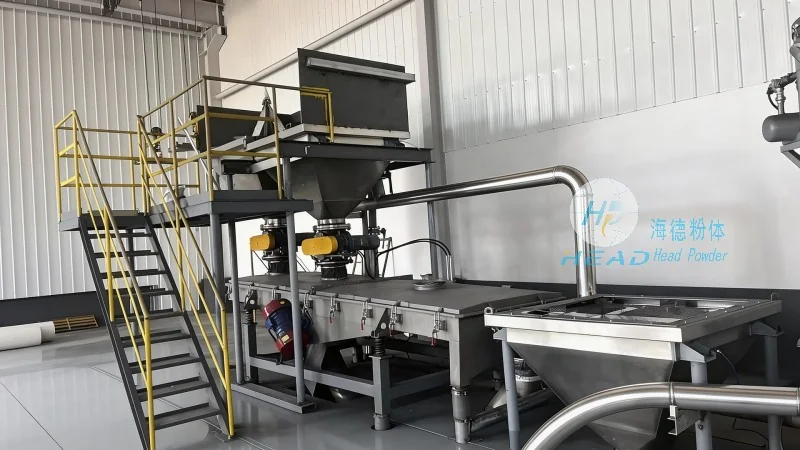
Technical Aspects of Pneumatic Conveying Systems
The effectiveness of limestone pneumatic conveying systems depends on several technical parameters that must be carefully considered during the design phase. The system's capacity is determined by factors such as the air flow rate, particle size distribution, and material density. HeadPowder's engineers use advanced computational fluid dynamics (CFD) simulations to optimize the system design, ensuring that the air velocity is sufficient to lift and transport the limestone particles without causing excessive wear on the pipeline or components. The choice of material for the conveying pipeline is also critical, as it must withstand the abrasive nature of limestone and resist corrosion from moisture or chemical residues. Typically, stainless steel or high-grade plastic materials are used for the pipeline, depending on the specific application requirements. The system also includes components such as air compressors, filters, and control valves that work together to regulate the air pressure and flow, ensuring consistent performance and preventing system failures.
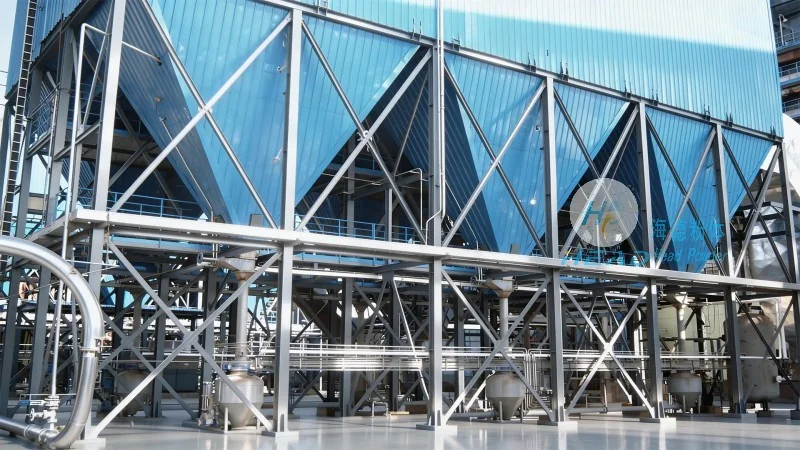
Customer Success Stories
HeadPowder has successfully implemented limestone pneumatic conveying systems for numerous clients across China and beyond. For example, a large cement manufacturer in Shandong reduced its material handling costs by 30% after installing a HeadPowder system that transported limestone from a quarry to the production plant over a distance of 800 meters. The system's reliability and low maintenance requirements allowed the client to maintain a consistent production schedule, improving overall operational efficiency. Another client, a chemical processing facility, reported a significant reduction in dust emissions and improved worker safety after upgrading to a HeadPowder pneumatic conveying system. The system's enclosed design and efficient filtration reduced airborne dust by 90%, meeting stringent environmental regulations and enhancing workplace conditions.
Conclusion
Limestone pneumatic conveying systems represent a cutting-edge solution for the efficient and reliable transport of limestone over long distances. With its ability to overcome the limitations of traditional material handling methods, these systems offer significant advantages in terms of cost-effectiveness, operational efficiency, and environmental compliance. HeadPowder, with its expertise in engineering and manufacturing, provides customized pneumatic conveying solutions that meet the unique needs of industrial clients. By leveraging advanced technology and a customer-centric approach, HeadPowder continues to deliver high-performance systems that enhance the productivity and sustainability of industrial operations worldwide.




