HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced pneumatic conveying solutions tailored for the handling of fine chemical materials. This article delves into the fundamental principles of such equipment and highlights key working scene characteristics that make it an indispensable asset in industrial applications.
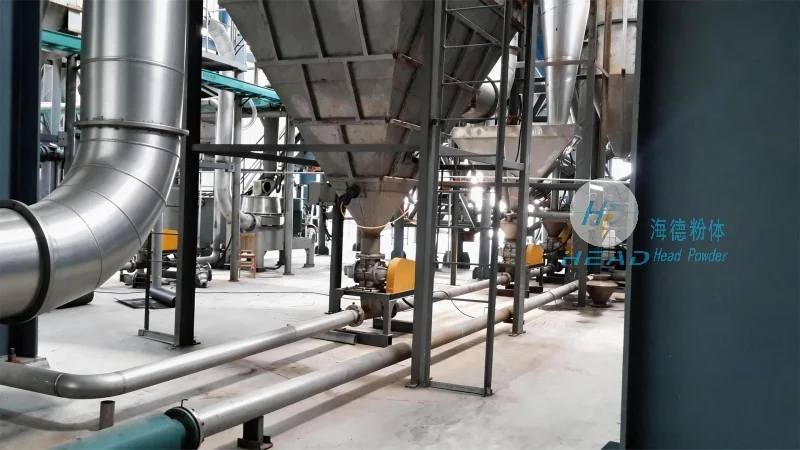
Company Overview: HeadPowder Engineering
HeadPowder Engineering Co., Ltd. is a reputable enterprise dedicated to the research, development, and production of high-quality pneumatic conveying systems. With a strong presence in Shandong, China, the company leverages its expertise to deliver reliable and efficient solutions for various industrial sectors. The company's commitment to innovation and customer satisfaction has established it as a trusted partner in the field of material handling technology.
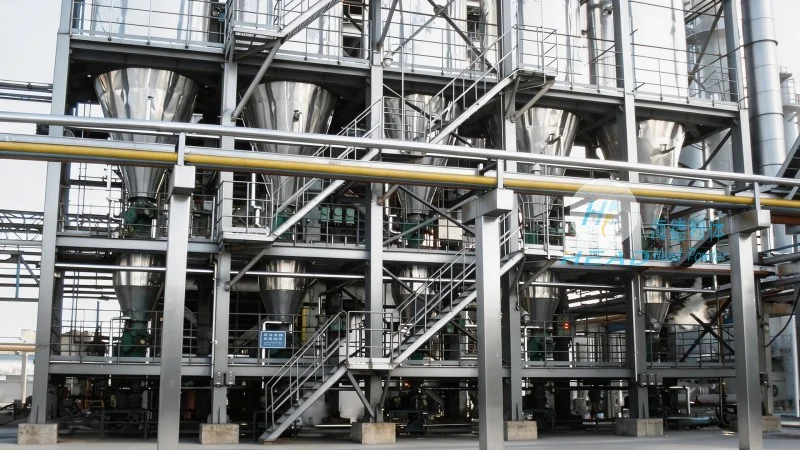
Principle of Pneumatic Conveying for Fine Chemical Materials
The core principle of pneumatic conveying equipment involves the use of air or gas to transport bulk materials through a pipeline system. For fine chemical materials, which often require gentle handling to prevent degradation or contamination, specialized designs are employed. The equipment typically operates by creating a pressure differential, either through positive pressure (where air is blown into the system) or negative pressure (where air is drawn out), to move the material from the source to the destination. Key components include the hopper, feeder, conveying line, and receiver, each playing a critical role in ensuring smooth and efficient material transport.
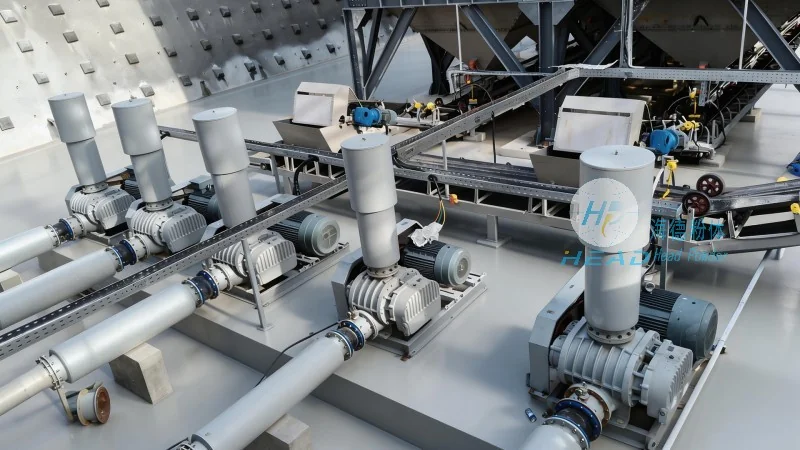
Working Scene Characteristics of Pneumatic Conveying Equipment
The application of pneumatic conveying equipment for fine chemical materials is characterized by several distinct features that cater to the unique demands of these materials. Firstly, the equipment is designed to minimize material degradation, ensuring that the chemical properties of the fine powders remain intact during transport. This is achieved through gentle handling mechanisms and optimized air flow rates. Secondly, the system offers high flexibility in terms of layout and integration with existing production lines, allowing for seamless incorporation into various industrial setups. Thirdly, the equipment provides excellent control over material flow, enabling precise dosing and regulation, which is crucial for processes that require consistent material delivery. Additionally, the system is capable of handling a wide range of fine chemical materials, from pharmaceutical powders to specialty chemicals, making it a versatile solution for diverse industrial needs.
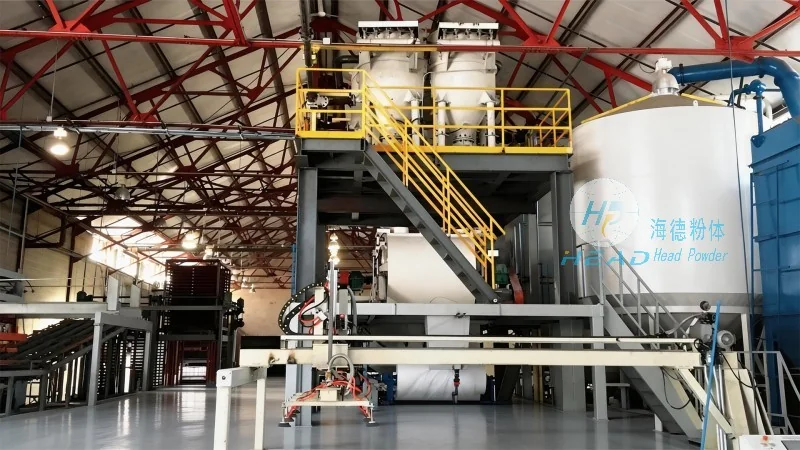
Key Advantages and Applications
Pneumatic conveying equipment for fine chemical materials offers numerous advantages that make it a preferred choice in industrial settings. One of the primary benefits is the ability to handle materials that are difficult to transport using traditional methods, such as those with high moisture content or abrasive properties. The system also provides a hygienic and enclosed environment, which is essential for pharmaceutical and food-grade applications where contamination control is paramount. Furthermore, the equipment reduces labor costs and improves safety by eliminating the need for manual handling of bulk materials. In terms of applications, these systems are widely used in pharmaceutical manufacturing, chemical processing, food processing, and other industries where fine powders need to be transported efficiently and safely.




