For industrial operations dealing with precipitated barium sulfate, efficient and reliable material handling is crucial. The air-driven pneumatic conveying equipment designed specifically for this application plays a vital role in ensuring smooth production processes. This article explores the underlying principles of such equipment and highlights the key characteristics of its working scenarios, providing insights into how it enhances operational efficiency in various industrial settings.
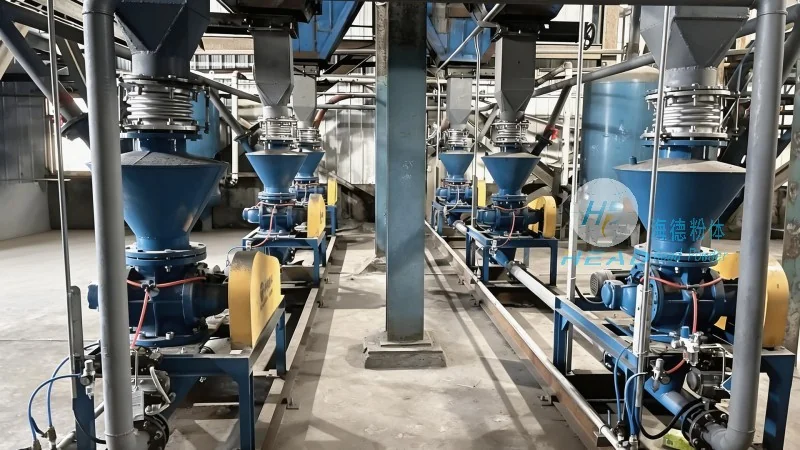
Introduction to Precipitated Barium Sulfate and Its Handling Needs
Precipitated barium sulfate, a fine powder commonly used in pharmaceuticals, coatings, and other industrial applications, requires specialized handling due to its particle size and physical properties. Traditional methods like manual conveying or mechanical systems may lead to dust issues, material degradation, or inefficiencies. The air-driven pneumatic conveying system addresses these challenges by utilizing compressed air to transport the material through a sealed pipeline, offering a clean, dust-free, and continuous transfer solution.
HeadPowder: A Leading Provider of Industrial Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., based in China, is a reputable manufacturer specializing in engineering solutions for material handling. With a focus on innovation and customer-centric design, HeadPowder has developed advanced pneumatic conveying equipment tailored to the unique requirements of industries dealing with fine powders like precipitated barium sulfate. The company's expertise in mechanical engineering and material science ensures that their products meet the highest standards of performance and reliability.
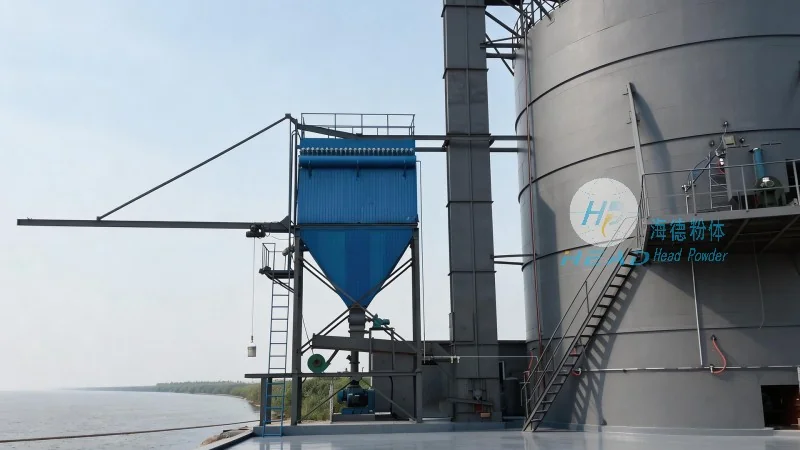
The Core Principle of Air-Driven Pneumatic Conveying
The fundamental principle behind air-driven pneumatic conveying is the use of air as the conveying medium to transport solid particles. In this system, compressed air is introduced into a pipeline, creating a flow that propels the material forward. There are two primary types of air-driven systems: positive pressure and negative pressure. Positive pressure systems generate air pressure at the material inlet, pushing the particles through the pipeline, while negative pressure systems create a vacuum at the discharge end, drawing the material into the system.
For precipitated barium sulfate, which is typically a fine, low-density powder, positive pressure systems are often preferred due to their ability to handle high material loads and maintain consistent flow rates. The equipment includes components such as a material hopper, air compressor, conveying line, and a receiver or discharge unit. The material is fed into the hopper, where it is mixed with the compressed air, and then transported through the pipeline to the destination point. The system is designed to minimize particle segregation and ensure uniform distribution of the material.
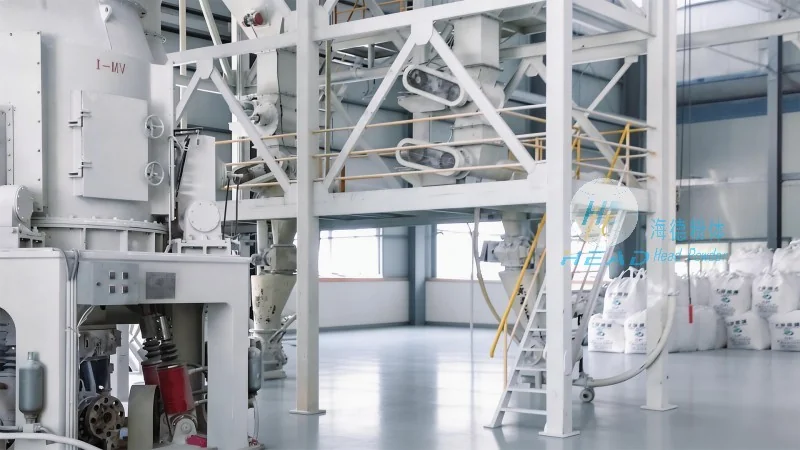
Key Working Scene Characteristics of the Equipment
The working scene characteristics of the air-driven pneumatic conveying equipment for precipitated barium sulfate are tailored to the specific demands of industrial applications. These characteristics include:
- Efficiency and Throughput: The system is engineered to achieve high material throughput with minimal energy consumption. By optimizing the air flow and pipeline design, the equipment ensures consistent and reliable material transfer, even for large volumes of precipitated barium sulfate.
- Cleanliness and Hygiene: As the material is conveyed in a sealed pipeline, the system eliminates dust and contamination risks, which is critical in industries like pharmaceuticals and food processing where product purity is paramount.
- Flexibility and Scalability: The equipment can be configured to handle different material types and flow rates, making it adaptable to various production scales. This flexibility allows manufacturers to expand their operations without significant modifications to the conveying system.
- Low Maintenance and Durability: The components of the air-driven system are designed for long-term operation with minimal maintenance. High-quality materials and robust construction ensure that the equipment can withstand the abrasive nature of fine powders like precipitated barium sulfate, reducing downtime and operational costs.
Application Scenarios and Operational Benefits
The air-driven pneumatic conveying equipment is widely used in industrial settings where the handling of fine powders is essential. In the pharmaceutical industry, for example, the equipment is used to transport precipitated barium sulfate for use in drug formulations, ensuring that the material is delivered in a clean and controlled manner. In the coatings industry, the system helps in transferring the powder to mixing and application equipment, maintaining the quality and consistency of the final product.
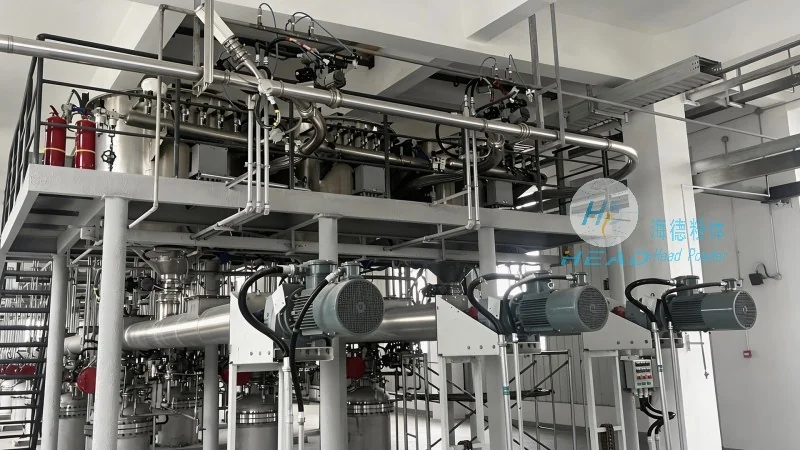
In the chemical manufacturing sector, the equipment is employed to handle raw materials and intermediate products, facilitating smooth production workflows. The benefits of using this system include improved product quality, reduced labor costs, and enhanced safety by minimizing exposure to dust and airborne particles. Additionally, the sealed system prevents environmental contamination, aligning with modern industrial standards for sustainability and compliance.
Conclusion: Enhancing Operational Performance with Advanced Conveying Solutions
For industries dealing with precipitated barium sulfate, the air-driven pneumatic conveying equipment from HeadPowder offers a reliable and efficient solution to material handling challenges. By leveraging the principles of air-based transport and advanced engineering, the system ensures consistent performance, high throughput, and minimal maintenance. The working scene characteristics, including cleanliness, flexibility, and durability, make it an ideal choice for various industrial applications. As a leading provider of material handling solutions, HeadPowder continues to innovate and provide tailored equipment that meets the evolving needs of modern industries, ensuring that production processes remain efficient, safe, and environmentally responsible.




