For industries dealing with limestone powder and similar fine particulate materials, efficient material handling is crucial for maintaining production efficiency and operational safety. This article explores the principle and working scene characteristics of pneumatic conveying equipment designed specifically for limestone powder, highlighting how such systems enhance material transport in industrial settings.
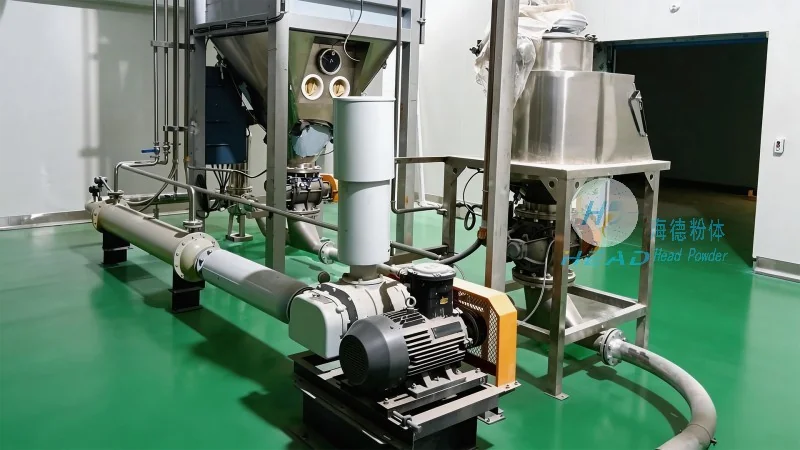
Understanding Pneumatic Conveying Technology for Limestone Powder
Pneumatic conveying systems utilize air or gas to transport bulk materials like limestone powder through a pipeline network. The core principle involves creating a pressure differential that propels the material along the conveying line. In a typical setup, a blower or compressor generates the necessary airflow, which draws the powder from a hopper or storage silo into the pipeline. The system can operate in either positive pressure (where air pushes the material) or negative pressure (where air pulls the material), with each mode suited to different application requirements and material characteristics.
The design of a limestone powder pneumatic conveying system is tailored to handle the specific properties of the material. Limestone powder is often fine and can be prone to dust generation, making the choice of equipment components critical. Key elements include high-efficiency cyclones for separation, filters to capture fine particles, and specialized valves that prevent material blockage. The system's capacity and pressure requirements are determined by factors such as the volume of material to be transported, the distance of the conveying line, and the desired flow rate. By optimizing these parameters, the equipment ensures reliable and continuous material transport, minimizing downtime and operational disruptions.
Working Scene Characteristics of Limestone Powder Pneumatic Conveying Equipment
The working scene characteristics of pneumatic conveying systems for limestone powder are defined by their adaptability to diverse industrial environments. These systems are commonly used in applications such as cement production, chemical processing, and mining operations, where limestone is a key raw material. In cement plants, for example, limestone powder is conveyed from storage silos to grinding mills or clinker production lines, ensuring a steady supply of raw material for the manufacturing process. The equipment's ability to handle large volumes of fine powder efficiently reduces the risk of material buildup and improves overall plant productivity.
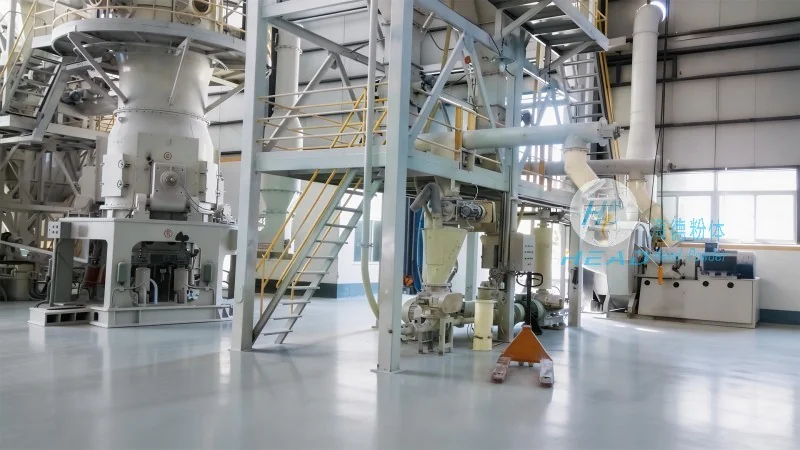
In chemical processing facilities, limestone powder is often used as a filler or reagent in various chemical reactions. Pneumatic conveying systems enable precise and controlled delivery of the powder to reactors, maintaining consistent material quality and process parameters. The systems are also employed in mining operations to transport limestone from extraction sites to processing plants, where it may be crushed or ground for further use. The working scene characteristics include the need for dust control measures, as limestone powder can be hazardous when inhaled, and the requirement for equipment that can handle abrasive materials without premature wear.
Another key characteristic is the flexibility of pneumatic conveying systems to integrate with existing industrial infrastructure. They can be retrofitted into existing plants or designed as new installations, adapting to the layout and space constraints of the facility. The systems are also capable of handling varying material flow rates, from low-volume, intermittent transport to high-volume, continuous operation. This adaptability makes them suitable for a wide range of applications, from small-scale laboratory use to large-scale industrial production.
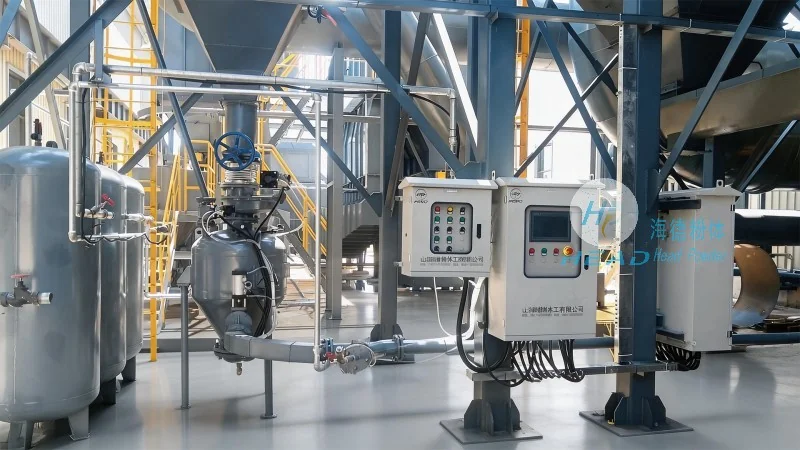
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of pneumatic conveying equipment tailored for limestone powder and other fine particulate materials. With a focus on innovation and quality, the company has established itself as a trusted provider of industrial material handling solutions. Headpowder's expertise lies in designing and manufacturing systems that meet the specific needs of clients in various industries, ensuring reliable and efficient material transport.
Headpowder's facilities are located in Shandong, China, where the company leverages advanced manufacturing technologies and a skilled workforce to produce high-performance pneumatic conveying equipment. The company adheres to strict quality control standards, ensuring that each system is tested and validated for performance and durability before delivery. Clients benefit from the company's commitment to customer service, with technical support and after-sales assistance available to address any operational challenges.
Headpowder's product line includes a range of pneumatic conveying systems, from simple low-capacity units to complex high-capacity networks. The company's engineers work closely with clients to understand their specific requirements, providing customized solutions that optimize material handling efficiency and reduce operational costs. By combining technical expertise with practical experience, Headpowder delivers equipment that enhances productivity and safety in industrial settings.




