For industries dealing with bulk powders, maintaining a clean and efficient material handling process is crucial. The dust-free bulk material loading station equipped with pneumatic conveying technology offers a solution that addresses both contamination control and operational efficiency. This equipment is designed specifically for handling small-bag materials, ensuring that the entire process remains free from dust and particulate contamination.
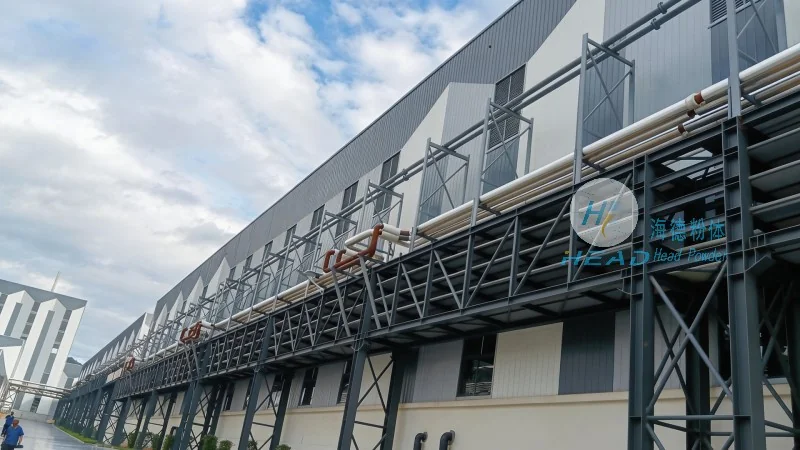
Working Principle of the Dust-Free Bulk Material Loading Station
The core of this system lies in its pneumatic conveying mechanism, which uses compressed air to transport bulk powders from the storage bags to the processing equipment. The station is engineered to open the small-bag, transfer the material into a sealed hopper, and then convey it through a dedicated air duct to the target location. This process eliminates the need for manual handling, reducing the risk of human error and exposure to hazardous powders. The system incorporates advanced filtration and sealing technologies to prevent dust leakage, ensuring compliance with industrial hygiene standards and environmental regulations.
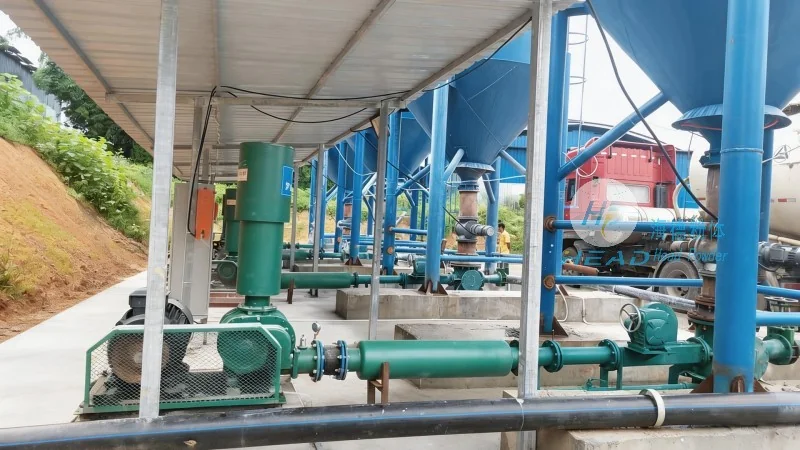
Key Features and Technical Advantages
One of the standout features of this loading station is its ability to handle a wide range of bulk materials, from fine powders to granules, without compromising on cleanliness. The integrated dust filtration system, typically featuring HEPA filters, captures 99.97% of particles as small as 0.3 microns, maintaining a clean working environment. Additionally, the station is designed for easy maintenance, with quick-release components and accessible filter cartridges that simplify routine upkeep. The pneumatic conveying technology also allows for precise control over material flow rates, enabling seamless integration with downstream processes such as mixing, packaging, or processing lines.
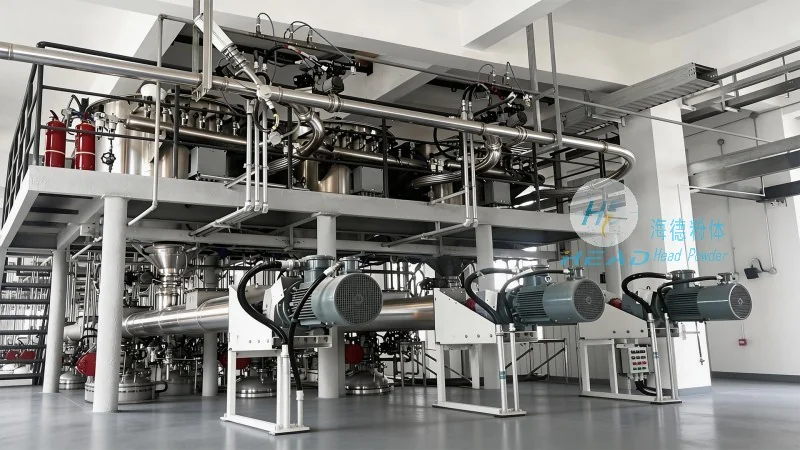
Typical Application Scenarios
These dust-free loading stations are widely used in industries where material purity is paramount, including pharmaceuticals, food processing, chemical manufacturing, and cosmetics. In pharmaceutical facilities, for example, the equipment ensures that raw materials are handled in a sterile environment, preventing cross-contamination and maintaining product quality. In food processing plants, it helps preserve the integrity of food powders, avoiding contamination from dust or foreign particles. Chemical manufacturers benefit from the system's ability to handle hazardous powders safely, with sealed systems that prevent exposure to operators. The versatility of the station also makes it suitable for small-bag handling in research and development labs, where precise material transfer is essential for experimental work.
Company Information and Service
HeadPowder, a leading provider of bulk material handling solutions, specializes in designing and manufacturing dust-free loading stations tailored to the needs of various industries. With a focus on innovation and quality, HeadPowder's products are engineered to meet the highest standards of performance and safety. The company, based in Shandong, China, leverages decades of experience in material handling technology to deliver reliable equipment that enhances operational efficiency and ensures product purity. HeadPowder's team of experts works closely with clients to understand their specific requirements, offering customized solutions that integrate seamlessly with existing production lines. The company's commitment to customer satisfaction and technical support ensures that clients receive not only high-quality equipment but also ongoing assistance to maximize the system's performance and longevity.




