Principle and Working Scene Characteristics of Bottom-Hopper Powder Pneumatic Conveying Equipment
Release time:2026-09-19 19:01:33
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Bottom-hopper powder pneumatic conveying equipment is a specialized system designed for the efficient handling and transportation of bulk powder materials from storage silos or hoppers to processing units. This technology is widely used in various industrial sectors, including chemical, food, pharmaceutical, and cement industries, where reliable and low-cost powder transfer is crucial for operational efficiency. The system operates by utilizing air as the conveying medium, creating a pressure differential to move powders through pipelines. Understanding its principle and working scene characteristics is essential for selecting the right equipment for specific industrial applications.
Principle of Operation
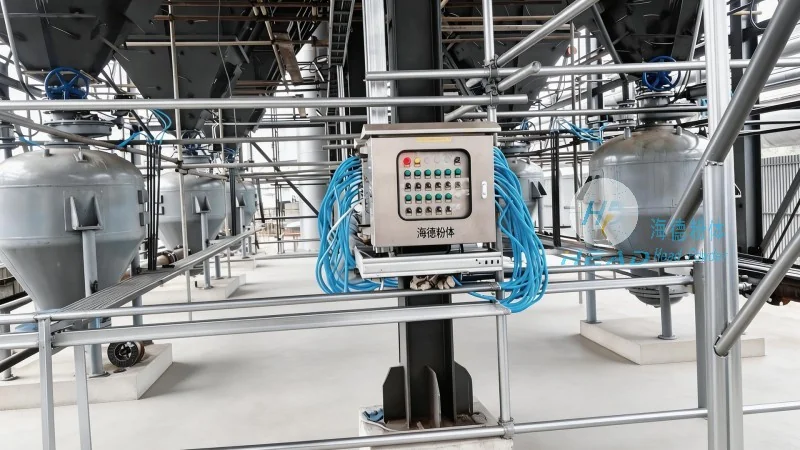
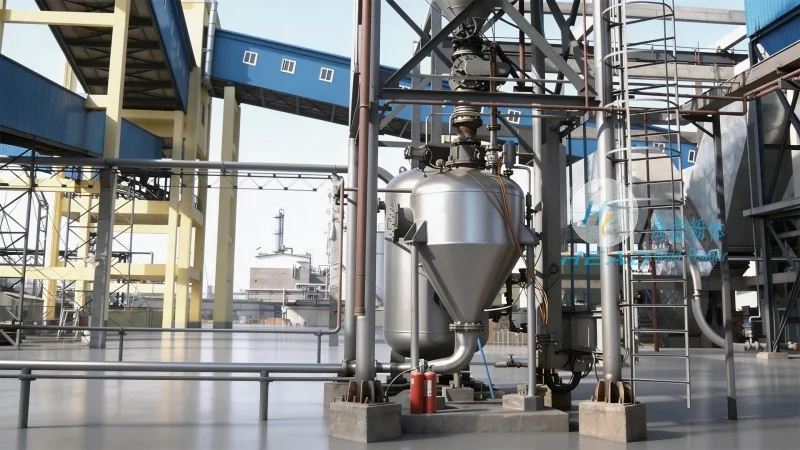
The core principle of bottom-hopper powder pneumatic conveying systems revolves around the use of air to create a suction or pressure difference that propels powder particles through a pipeline. In a typical bottom-hopper setup, a hopper is located at the bottom of a storage silo, equipped with a venturi or a rotary valve that controls the flow of air and powder. When the system is activated, compressed air is introduced into the hopper, creating a negative pressure that draws powder particles into the air stream. The air-powder mixture then travels through the pipeline to the destination point, where the powder is separated from the air using a cyclone or a filter. The air is then recycled back to the hopper, completing the cycle. This process ensures continuous and consistent powder transfer without the need for mechanical components like belts or buckets, reducing maintenance and operational costs.
Working Scene Characteristics
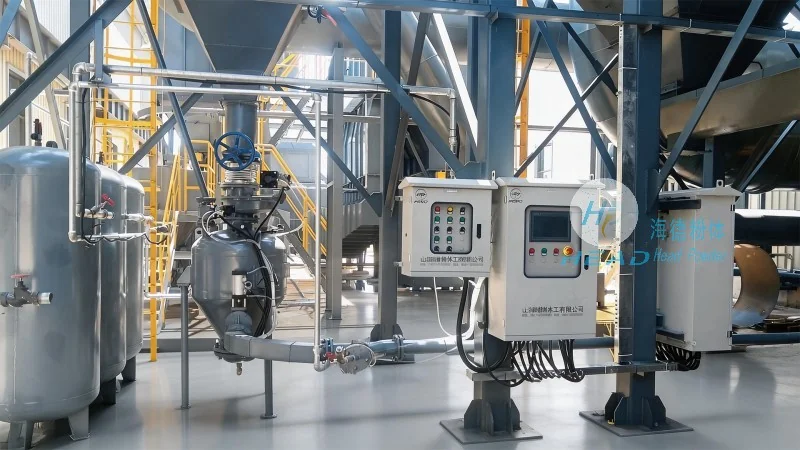
The working scene characteristics of bottom-hopper powder pneumatic conveying equipment are tailored to meet the demands of different industrial environments. One of the key advantages is its ability to handle a wide range of powder types, from fine powders like flour and cement to coarse powders like limestone and coal. The system is particularly suitable for applications where the powder needs to be transferred over long distances or at high elevations, as the air pressure can be adjusted to accommodate these requirements. Additionally, the equipment is designed to minimize dust emissions and maintain a clean working environment, which is critical in industries such as food and pharmaceuticals where product purity is paramount. The bottom-hopper design also allows for easy integration with existing storage systems, making it a cost-effective solution for upgrading or expanding powder handling capabilities.
Company Background and Expertise
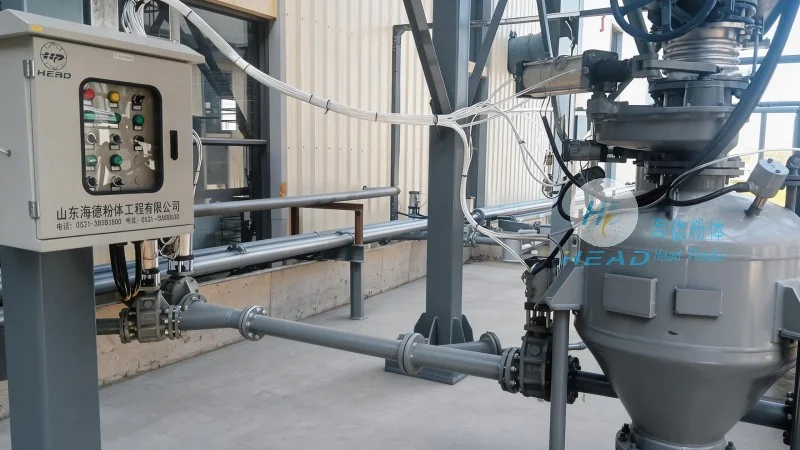
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of powder handling equipment in China. With a focus on innovation and quality, the company has established itself as a trusted partner for industries requiring reliable and efficient powder transfer solutions. HeadPowder specializes in the design, manufacturing, and installation of bottom-hopper pneumatic conveying systems, as well as other related equipment such as silos, hoppers, and dust collectors. The company's team of engineers and technicians brings extensive experience in the field, ensuring that each project is tailored to meet the specific needs of the client. HeadPowder's commitment to customer satisfaction and technical excellence has earned it a reputation for delivering high-performance equipment that meets international standards. The company's facilities are equipped with advanced manufacturing technology and quality control measures, ensuring that every product is built to last and perform optimally in various industrial applications.




