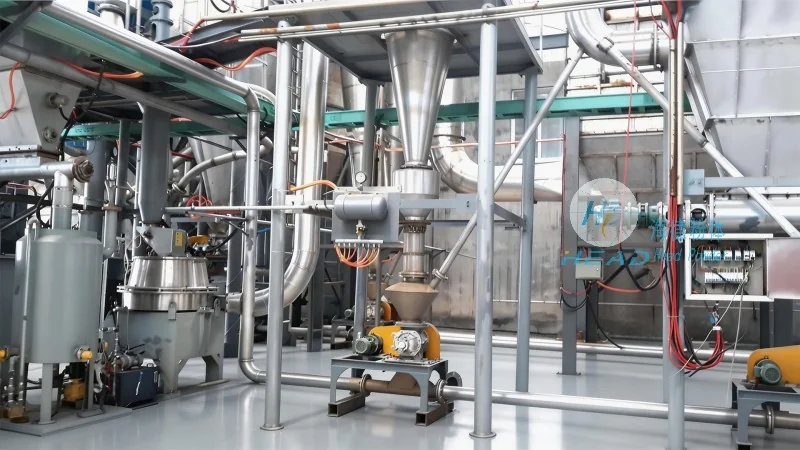
Stone powder, a critical raw material across multiple industrial sectors, requires efficient and reliable conveying solutions to maintain smooth production workflows. The stone powder granular material conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., addresses these needs through advanced engineering and robust design. This article examines the fundamental principles of such systems and highlights the key characteristics of their operational environments.
Introduction to Stone Powder Conveying Systems
HeadPowder, a leading manufacturer headquartered in Shandong, China, specializes in material handling solutions. The company’s expertise lies in designing and manufacturing conveying systems tailored to the unique properties of stone powder. These systems are essential for industries including construction, mining, and chemical processing, where consistent and efficient material transport directly impacts productivity and cost-effectiveness.
The Core Principle of Granular Material Conveying
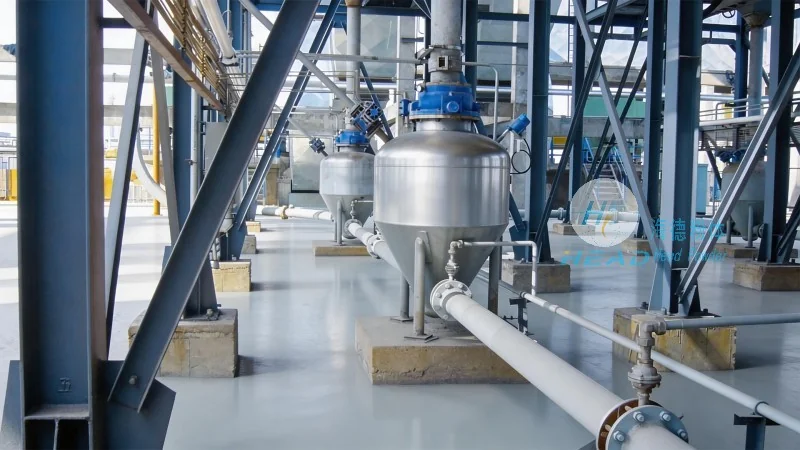
The stone powder granular material conveying system operates on the principle of transferring bulk materials through a controlled environment. Given stone powder’s fine and abrasive nature, specialized mechanisms are employed to prevent blockages and ensure consistent flow. Common technologies include pneumatic conveying, screw conveyors, and bucket elevators, each selected based on the material’s characteristics and the operational requirements of the application.
Working Scene Characteristics: Application in Diverse Industries
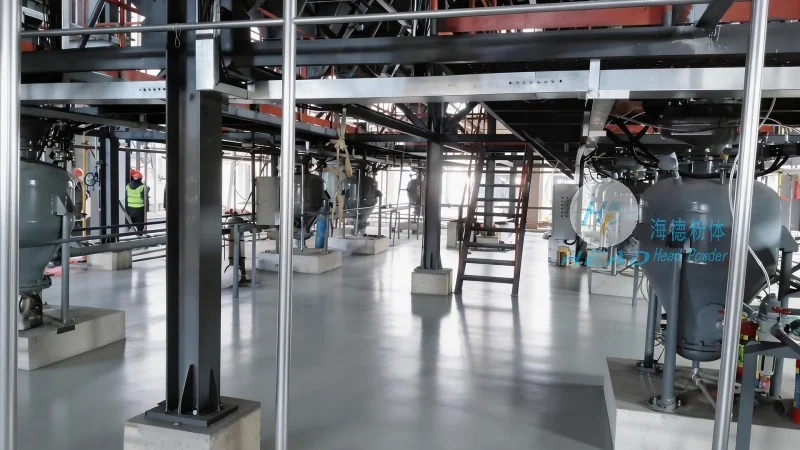
The operational environments of these conveying systems vary significantly across different industries. In the construction sector, they are used to transport raw stone powder to mixing plants, where it is combined with other materials to produce concrete and mortar. In mining operations, the systems help move processed stone powder from storage to processing units, optimizing workflow and reducing manual handling risks. The chemical industry also benefits from these systems, as they efficiently convey stone powder for manufacturing processes, ensuring compliance with safety and quality standards.
Key Features and Advantages of HeadPowder's Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. offers conveying systems designed to meet the demanding requirements of stone powder handling. These systems are characterized by high efficiency, low maintenance, and durability, which are crucial for long-term operational success. The company’s engineering team focuses on integrating advanced materials and components to enhance performance and reduce downtime. Additionally, the systems are equipped with monitoring and control features that allow for real-time adjustments, ensuring optimal operation under varying conditions.
Conclusion: Enhancing Operational Efficiency with Advanced Conveying Technology
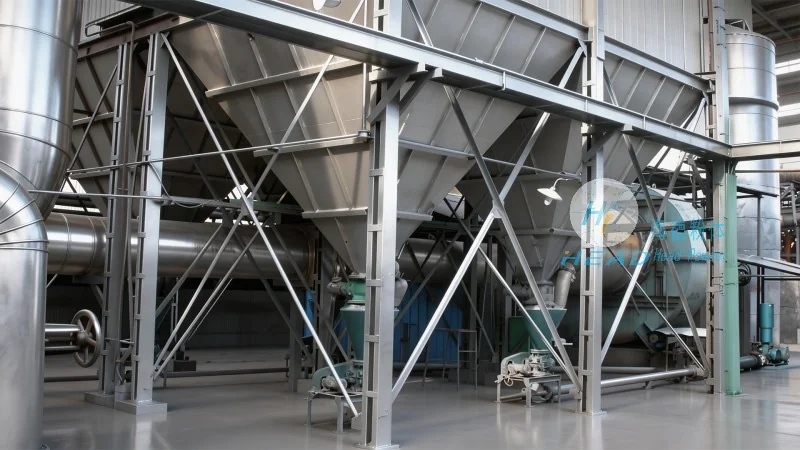
As industries continue to rely on stone powder as a vital component, the importance of reliable conveying systems cannot be overstated. HeadPowder's stone powder granular material conveying system equipment provides a robust solution that combines technical innovation with practical application. By understanding the principles and characteristics of these systems, businesses can improve their material handling processes, reduce costs, and enhance overall productivity. With a strong presence in Shandong, China, HeadPowder remains committed to delivering high-quality engineering solutions that meet the evolving needs of the industry.




