Principle and Working Scene Characteristics of Manganese Sulfate Material Handling System Equipment
Release time:2026-09-19 14:01:31
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
For industrial operations that involve the handling and transportation of manganese sulfate, an efficient and reliable material handling system is crucial. This article explores the underlying principles of the Manganese Sulfate Material Handling System Equipment, as provided by Shandong HeadPowder Engineering Co., Ltd., and highlights the key working scene characteristics that make it an ideal solution for various industrial applications.
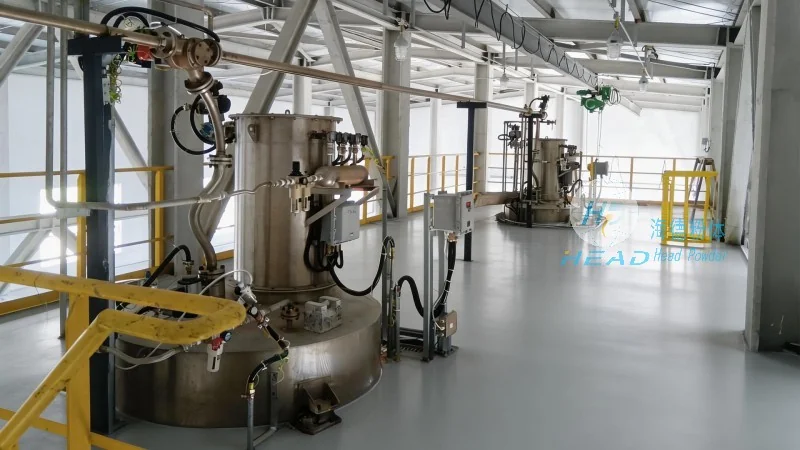
Overview of Manganese Sulfate Material Handling System Equipment
Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of advanced material handling systems tailored for the chemical industry. The Manganese Sulfate Material Handling System Equipment is engineered to address the unique challenges associated with transporting manganese sulfate, a critical raw material used in battery production, fertilizers, and other industrial processes. The system integrates multiple components, including conveyors, feeders, and control mechanisms, to ensure seamless material flow from storage to processing units.
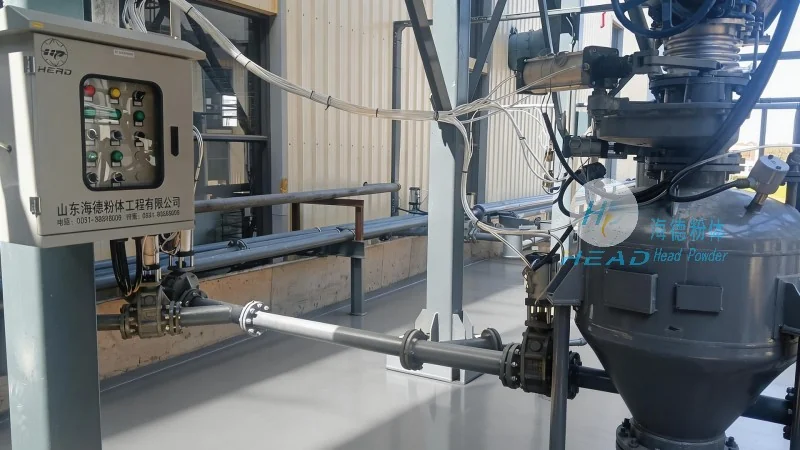
Principle of Operation
The core principle of the Manganese Sulfate Material Handling System Equipment is to provide a continuous and controlled movement of material through a series of mechanical and electrical components. The system operates based on the following key mechanisms:
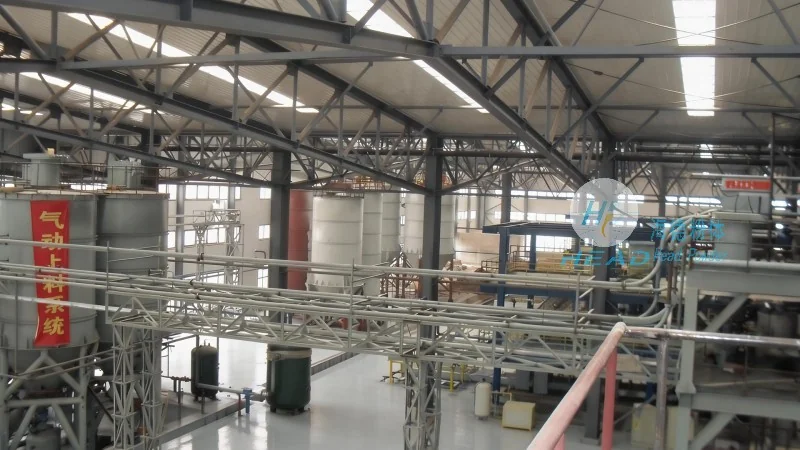
- Conveyor Systems: The equipment utilizes high-capacity conveyor belts or screw conveyors to transport manganese sulfate from storage silos or hoppers to processing areas. These conveyors are designed with durable materials to withstand the corrosive nature of manganese sulfate and ensure long-term performance.
- Feeding Mechanisms: Precise feeding devices, such as rotary valves or vibratory feeders, regulate the flow rate of manganese sulfate into the conveyor system. This ensures consistent material delivery, preventing overloading or underfeeding that could disrupt the processing line.
- Control Systems: Advanced control panels and sensors monitor the system's performance in real-time. These systems adjust conveyor speeds, feeding rates, and other parameters to maintain optimal material flow, enhancing efficiency and reducing downtime.
Working Scene Characteristics
The Manganese Sulfate Material Handling System Equipment is designed to operate effectively in diverse industrial environments, with several key characteristics that make it suitable for various applications:
- High Efficiency and Capacity: The system is engineered to handle large volumes of manganese sulfate, ensuring that production lines operate at maximum capacity without bottlenecks. This is particularly important in battery manufacturing plants where consistent raw material supply is critical.
- Corrosion Resistance: Given the chemical properties of manganese sulfate, the equipment is constructed with corrosion-resistant materials, such as stainless steel or specialized coatings. This ensures durability and longevity, reducing maintenance costs and extending the system's service life.
- Customization and Flexibility: Shandong HeadPowder Engineering Co., Ltd. offers customized solutions tailored to specific industrial needs. The system can be adapted to different production scales, conveyor lengths, and material types, making it versatile for various applications.
- Safety and Compliance: The equipment adheres to industrial safety standards and regulations. Features such as emergency stop buttons, overload protection, and proper ventilation systems ensure safe operation and compliance with environmental and occupational health guidelines.
Application Scenarios
The Manganese Sulfate Material Handling System Equipment is widely used in several industrial sectors, including:
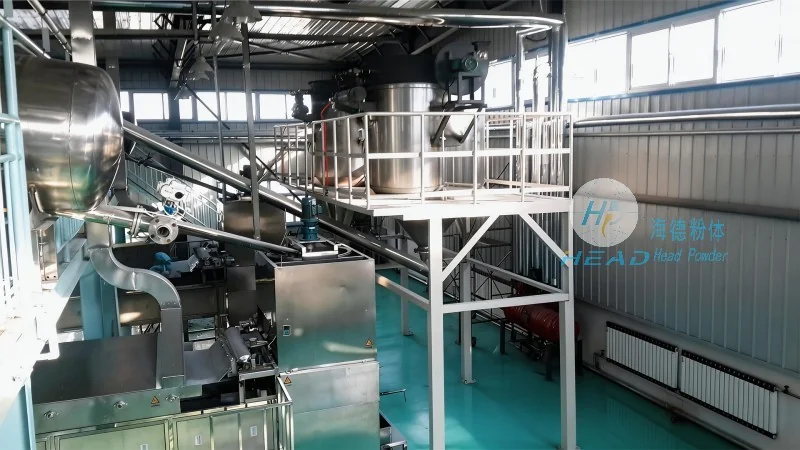
- Battery Manufacturing: In lithium-ion battery production, manganese sulfate is a key component. The system efficiently transports the raw material to the battery cell manufacturing lines, ensuring a steady supply and maintaining production efficiency.
- Fertilizer Production: Manganese sulfate is used as a micronutrient in agricultural fertilizers. The equipment facilitates the handling of this material from storage to blending and packaging units, supporting large-scale fertilizer production.
- Chemical Processing: In chemical plants, manganese sulfate is used in various processes, such as the production of other manganese compounds. The system ensures reliable material transport, enabling smooth operation of downstream chemical reactions.
Conclusion
Shandong HeadPowder Engineering Co., Ltd.'s Manganese Sulfate Material Handling System Equipment exemplifies advanced engineering and industrial design. By integrating efficient conveyor systems, precise feeding mechanisms, and advanced control technologies, the system ensures reliable and safe transportation of manganese sulfate in various industrial applications. With its corrosion resistance, high capacity, and customizable features, this equipment is a valuable asset for industries relying on manganese sulfate as a critical raw material. For businesses seeking to optimize their material handling processes, the Manganese Sulfate Material Handling System Equipment from Shandong HeadPowder Engineering Co., Ltd. offers a reliable and efficient solution.




