HeadPowder, a leading engineering company based in Shandong, China, specializes in providing advanced pneumatic conveying systems tailored for the handling of sodium bicarbonate. This article explores the key aspects of our pneumatic conveying solutions, highlighting the technical advantages, operational efficiency, and practical applications that make our systems ideal for various industrial sectors.
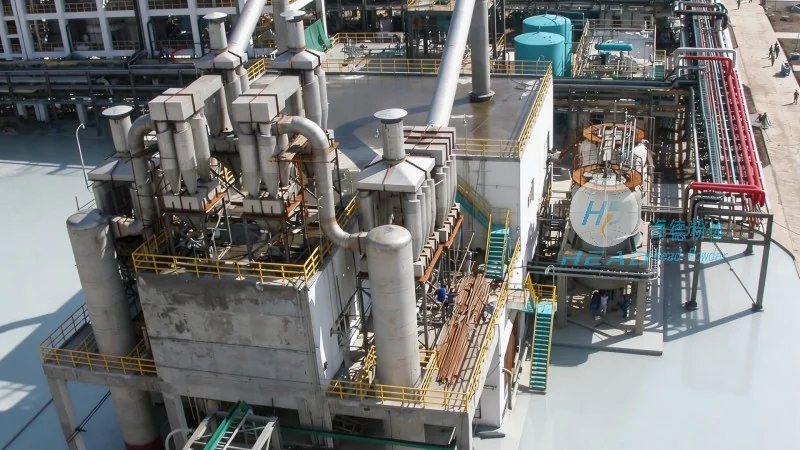
Understanding Pneumatic Conveying for Sodium Bicarbonate
Sodium bicarbonate, commonly known as baking soda, is a widely used chemical in industries such as food processing, pharmaceuticals, and chemical manufacturing. Traditional handling methods, like manual or mechanical conveying, often face challenges like dust generation, material degradation, and inefficiencies in material flow. Pneumatic conveying offers a solution by using air to transport the material, ensuring a clean, dust-free, and efficient process. Our systems are designed to handle sodium bicarbonate in bulk, ensuring minimal product loss and maintaining product quality throughout the conveying process.
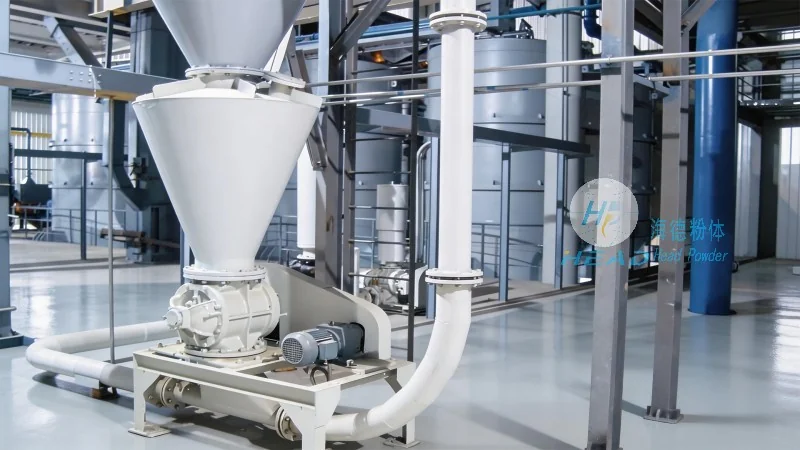
Key Features of Our Pneumatic Conveying Systems
HeadPowder's pneumatic conveying solutions for sodium bicarbonate are engineered with precision to meet the unique requirements of each application. The systems are equipped with high-efficiency air movers, such as rotary lobe blowers or positive displacement blowers, which provide consistent air pressure and flow rates. The conveying lines are constructed from materials resistant to chemical corrosion, such as stainless steel or specialized polymers, ensuring durability and longevity. Additionally, our systems incorporate advanced control mechanisms, allowing for real-time monitoring and adjustment of conveying parameters to optimize performance and reduce energy consumption.
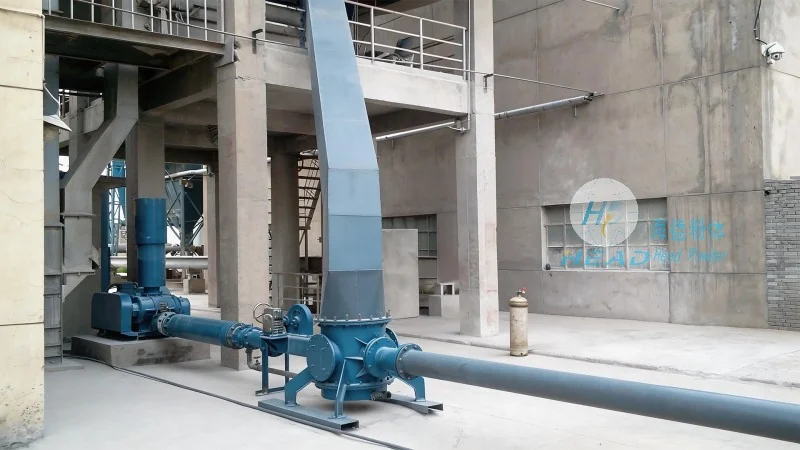
Benefits of Implementing Pneumatic Conveying for Sodium Bicarbonate
Adopting pneumatic conveying for sodium bicarbonate handling brings numerous benefits to industrial operations. Firstly, it significantly reduces dust and contamination risks, which is crucial for maintaining product purity and meeting regulatory standards. Secondly, the systems enhance operational efficiency by enabling continuous material flow, reducing downtime, and improving overall productivity. Thirdly, the use of air as the conveying medium minimizes material degradation, preserving the quality and characteristics of sodium bicarbonate. Furthermore, our systems are designed for easy integration into existing production lines, requiring minimal modifications and offering a cost-effective solution for upgrading material handling processes.
Customized Solutions for Diverse Applications
At HeadPowder, we understand that each industrial application has distinct requirements. Therefore, our pneumatic conveying solutions are customizable to suit various needs. Whether it's a short-distance conveying within a facility or long-distance transport between production sites, our systems can be configured to handle different flow rates, pressures, and material characteristics. We work closely with clients to assess their specific needs, from material analysis to system design and installation, ensuring that the final solution is optimized for their operational environment. Our team of experienced engineers provides comprehensive support, from initial consultation to post-installation maintenance, ensuring that clients achieve maximum value from their investment.
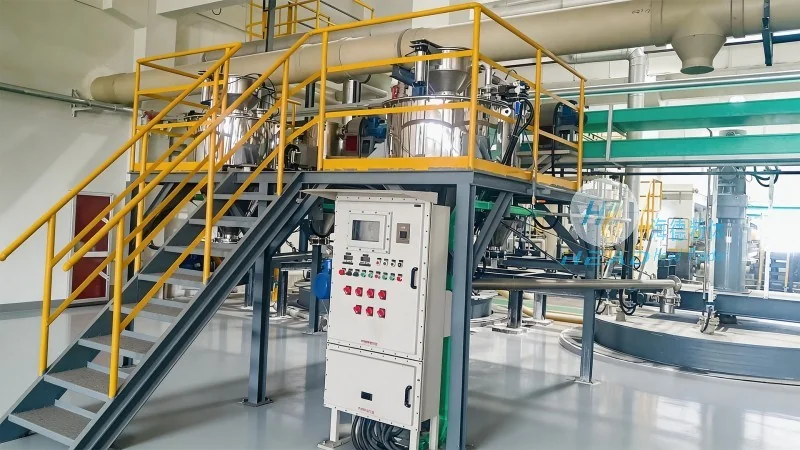
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is committed to delivering high-quality pneumatic conveying solutions for sodium bicarbonate. Our expertise in engineering and material handling ensures that our systems are reliable, efficient, and tailored to meet the demands of modern industrial applications. By leveraging advanced technology and a customer-centric approach, we help industries enhance their material handling processes, improve product quality, and achieve operational excellence. For businesses seeking to optimize their sodium bicarbonate handling operations, HeadPowder offers a comprehensive range of solutions designed to meet the highest standards of performance and reliability.




