HeadPowder, a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and supply of advanced automatic weighing and powder material conveying systems. Based in Shandong, China, the company has established itself as a reliable partner for industries requiring precise and efficient powder processing solutions. This article delves into the fundamental principles and operational characteristics of such systems, highlighting their role in modern industrial applications.
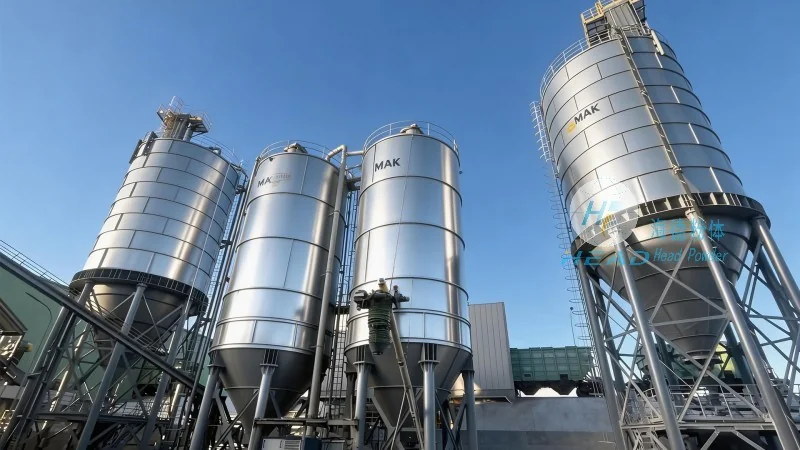
The Core Principle of the Automatic Weighing and Powder Material Conveying System
The automatic weighing and powder material conveying system operates on a sophisticated integration of weighing technology, material handling mechanisms, and control systems. At its heart, the system utilizes high-precision load cells and digital weighing indicators to measure the mass of powders with exceptional accuracy. This is complemented by a series of conveyor components, such as screw conveyors, pneumatic conveying lines, or bucket elevators, which transport the material from storage to processing points. The control unit, often equipped with programmable logic controllers (PLCs) or advanced software interfaces, coordinates the weighing and conveying processes, ensuring that the material is dispensed in precise quantities as per the set parameters.
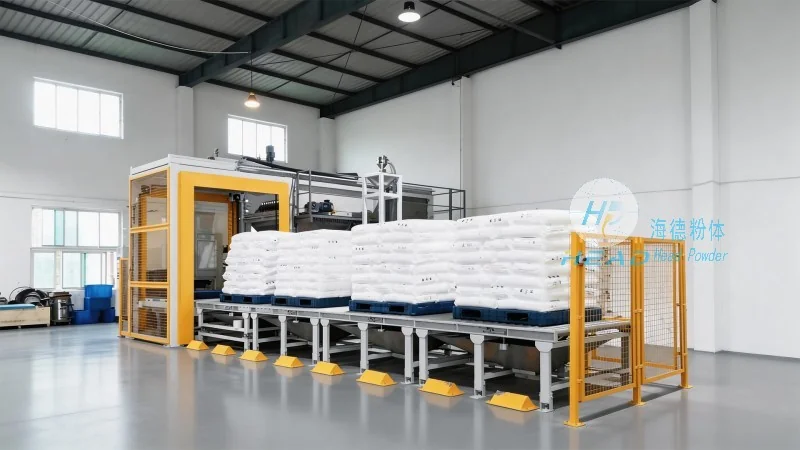
Key Working Scene Characteristics
The working scene characteristics of the automatic weighing and powder material conveying system are tailored to meet the diverse demands of industrial environments. These systems are designed for high-speed, continuous operation, making them ideal for applications in pharmaceuticals, food processing, chemical manufacturing, and other sectors where consistency and reliability are paramount. The modular design allows for customization to accommodate different powder types, particle sizes, and processing requirements, ensuring adaptability across various production lines.
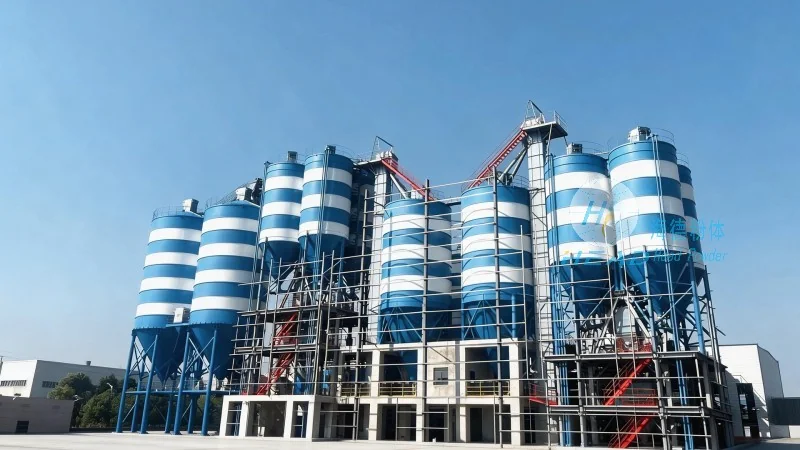
Application Scenarios and Operational Advantages
In pharmaceutical manufacturing, for instance, the system ensures that active pharmaceutical ingredients (APIs) are weighed and mixed with excipients to meet stringent regulatory standards. The precise control over dosage reduces waste and enhances product quality. Similarly, in the food industry, the system maintains hygiene standards while delivering accurate measurements for ingredients like flour, sugar, or spices. The operational advantages also include improved safety, as automated systems minimize human exposure to hazardous powders and reduce the risk of contamination. Additionally, the integration of real-time monitoring and data logging capabilities enables better process control and traceability, supporting quality management systems (QMS) and compliance with industry regulations.
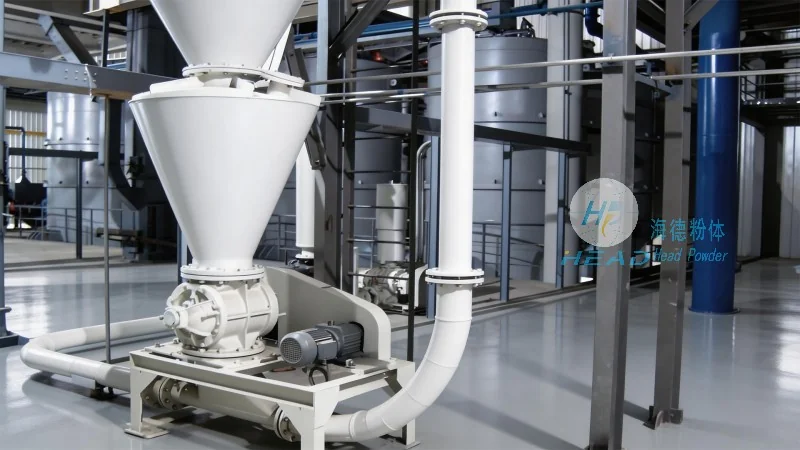
Technical Specifications and Customization Options
HeadPowder’s automatic weighing and powder material conveying systems are built with robust components that withstand the rigors of continuous operation. The load cells are typically rated for high accuracy, with resolutions down to 0.1% of the maximum capacity, ensuring minimal measurement errors. The conveying mechanisms are engineered to handle a wide range of powder properties, including abrasive, corrosive, or fine powders, through the use of specialized materials and sealing systems. Customization options are available to match specific operational needs, such as varying conveyor speeds, multiple weighing stations, or integration with existing production lines. The systems are also designed for easy maintenance, with accessible components and diagnostic tools that help in quick troubleshooting and downtime reduction.




