Long-distance powder handling systems represent a critical technology in modern industrial processes, enabling the efficient and reliable transport of bulk materials over extended distances. These systems are essential for industries ranging from mining and construction to pharmaceuticals and food processing, where the safe and efficient movement of powders is paramount to operational success. The core of such systems lies in their ability to handle materials that are often challenging to transport, including fine powders, granules, and bulk solids, with minimal degradation and loss.
Core Principles of Long-Distance Powder Handling Systems
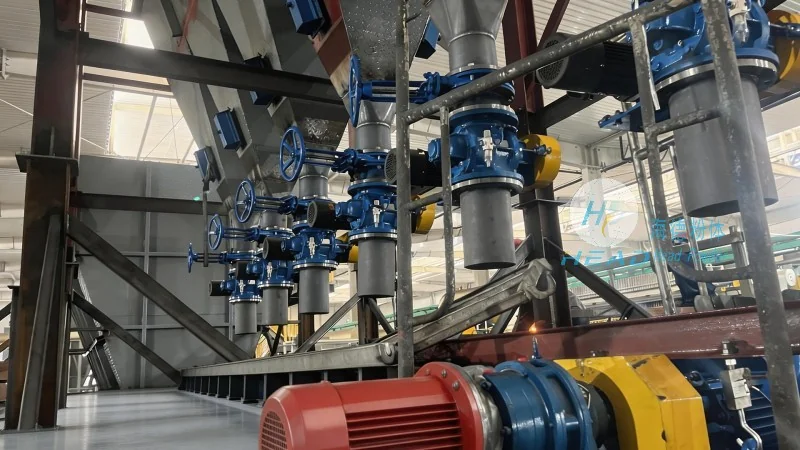
The fundamental principle behind long-distance powder handling systems is the conversion of mechanical energy into the force required to move bulk materials through a pipeline. This is typically achieved through positive displacement or pressure-driven mechanisms, which ensure that the material is continuously propelled forward without the need for constant external force application. Key components of these systems include feeders, conveyors, and control systems, each playing a vital role in maintaining the integrity and flow of the material. The system's design often incorporates features such as variable speed drives, which allow for precise control over the material flow rate, and pressure sensors that monitor system performance and prevent overloading or blockages.
Key Components and Their Functions
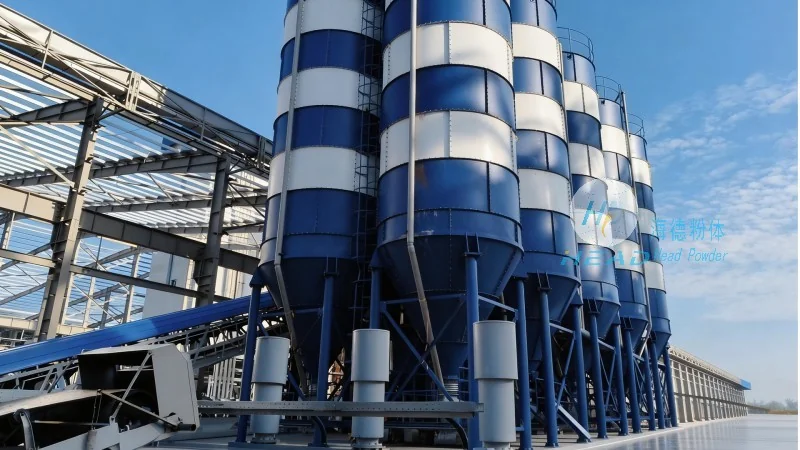
At the heart of a long-distance powder handling system are several critical components that work in concert to ensure optimal performance. The feeder, often a rotary or vibratory type, is responsible for uniformly feeding the material into the conveyor system, preventing clumping and ensuring a steady flow. The conveyor itself, which may be a pneumatic or mechanical system, is designed to transport the material through the pipeline. Pneumatic systems use compressed air to create a flow of material, while mechanical systems rely on screw, belt, or bucket conveyors. The control system, equipped with sensors and automation software, monitors parameters such as pressure, flow rate, and temperature, adjusting the system's operation in real-time to maintain efficiency and safety.
Working Scenarios and Industry Applications
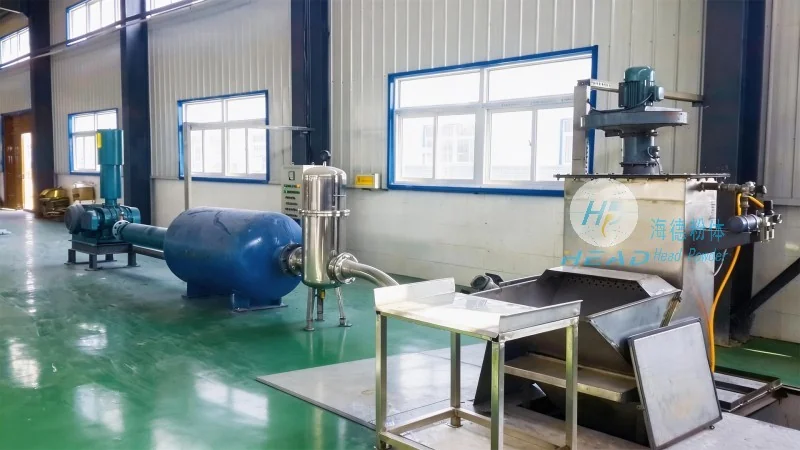
Long-distance powder handling systems are employed in a wide array of industrial applications, each requiring specific system configurations to meet operational demands. In the mining industry, these systems are used to transport ore from extraction sites to processing facilities, often over distances of several kilometers. The systems must be robust enough to handle abrasive materials and withstand harsh environmental conditions. In the construction sector, they are utilized for transporting cement, sand, and other bulk materials to job sites, improving logistics efficiency and reducing material handling costs. The pharmaceutical and food industries also rely on these systems for the transport of powders, where strict hygiene and contamination control are essential. These applications demand systems that are easy to clean, maintain, and comply with regulatory standards.
Advantages and Challenges in System Operation
Implementing long-distance powder handling systems offers several advantages, including increased operational efficiency, reduced labor costs, and improved safety by minimizing manual handling of bulk materials. However, these systems also present challenges that must be addressed to ensure reliable operation. One of the primary challenges is the potential for material blockages or clogging in the pipeline, which can be caused by moisture, agglomeration, or foreign particles. To mitigate this, systems often include features such as air knives, vibration devices, and cleaning mechanisms. Another challenge is the need for regular maintenance and system calibration to ensure consistent performance. Companies specializing in this technology, such as Shandong HeadPowder Engineering Co., Ltd., provide comprehensive solutions that address these challenges through advanced design and quality control.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
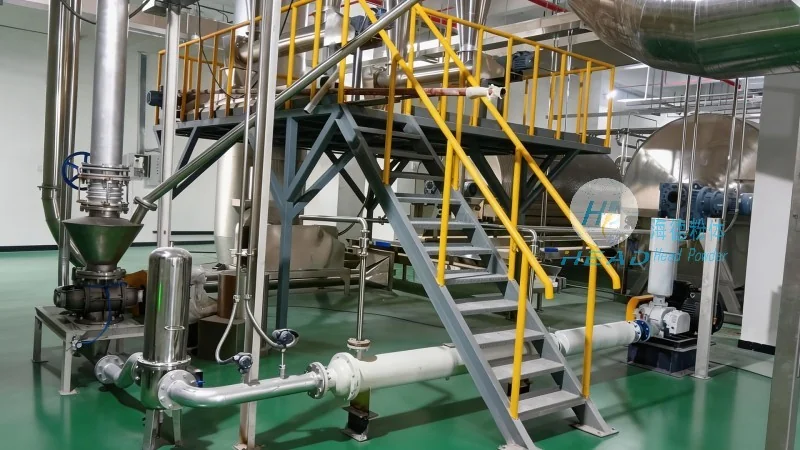
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of long-distance powder handling systems. With a focus on innovation and customer-centric solutions, the company has established itself as a trusted partner in the industrial sector. HeadPowder's systems are designed to meet the diverse needs of various industries, offering customizable solutions that enhance operational efficiency and reduce costs. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to develop cutting-edge technology. By combining advanced engineering with practical application, HeadPowder ensures that its systems are not only efficient but also reliable and durable, meeting the highest standards of industrial performance.




