Understanding the working principle and features of nitrogen-protected powder pneumatic conveying systems is crucial for industries that handle sensitive powders, as these systems ensure material integrity and operational efficiency. This article explores the core mechanisms and key attributes of such systems, providing insights into their design and functionality.
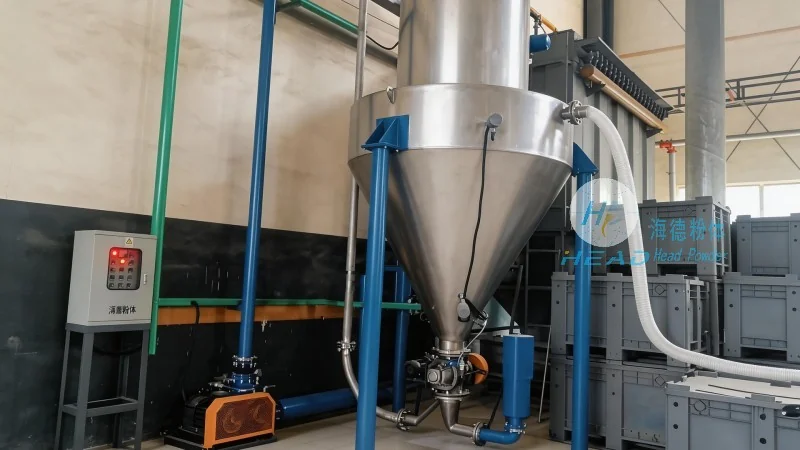
Introduction to Nitrogen-Protected Powder Pneumatic Conveying
HeadPowder, a leading manufacturer based in Shandong, China, specializes in developing advanced pneumatic conveying solutions tailored for industries requiring strict environmental control. The nitrogen-protected powder pneumatic conveying line is a critical equipment for transporting powders in a controlled atmosphere, preventing oxidation, moisture absorption, or contamination. This system integrates nitrogen gas as a protective medium to maintain the quality of the conveyed material throughout the process.
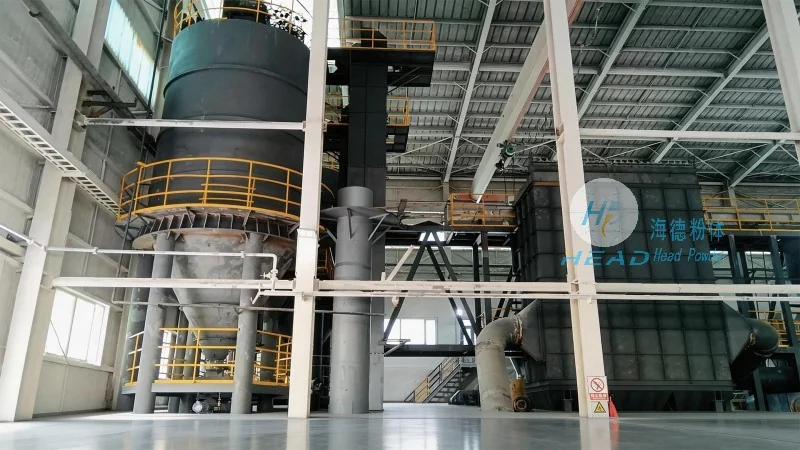
Working Principle of Nitrogen-Protected Powder Pneumatic Conveying
The fundamental working principle of a nitrogen-protected powder pneumatic conveying system involves the use of compressed nitrogen gas to create a positive pressure environment within the conveying line. The process begins with the powder being fed into a hopper or feeder, where it is then drawn into the conveying line by the nitrogen gas flow. The nitrogen gas, typically supplied at a pressure of 0.5 to 1.0 MPa, acts as a carrier medium, transporting the powder particles through the pipeline. Key components include the feeding device, conveying pipeline, gas distributor, and discharge equipment. The system operates by creating a pressure differential between the feeding point and the discharge point, ensuring continuous and stable material transport. The nitrogen gas not only transports the powder but also isolates it from external air, maintaining a dry and inert environment that preserves the material's properties.
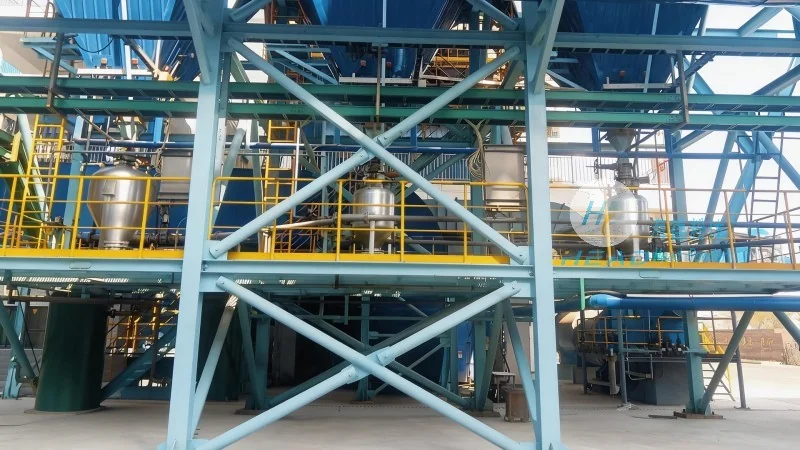
Key Features of Nitrogen-Protected Powder Pneumatic Conveying Systems
Several distinct features make nitrogen-protected powder pneumatic conveying systems ideal for sensitive applications. Firstly, the use of nitrogen gas provides excellent protection against oxidation and moisture, which is vital for powders like pharmaceuticals, food additives, and chemical intermediates. Secondly, the system offers high conveying efficiency, with the ability to transport powders over long distances (up to several hundred meters) with minimal pressure drop. Thirdly, the design allows for easy integration with existing production lines, reducing installation complexity and downtime. Additionally, the system is equipped with safety features such as pressure relief valves and gas leak detectors to ensure operational safety. The modular construction of these systems enables customization based on specific material characteristics and process requirements, making them versatile for various industrial applications.
Applications and Benefits
Nitrogen-protected powder pneumatic conveying systems are widely used in industries where material purity and process reliability are paramount. In the pharmaceutical industry, these systems ensure that active pharmaceutical ingredients (APIs) are transported without contamination or degradation. In the food industry, they maintain the freshness and quality of food powders, preventing spoilage and maintaining flavor integrity. In chemical manufacturing, the systems protect sensitive chemicals from atmospheric exposure, enhancing product stability and safety. The benefits of using such systems include improved product quality, reduced material loss, enhanced process control, and increased operational safety. Furthermore, the energy efficiency of modern nitrogen-protected systems, with optimized gas usage and minimal pressure losses, contributes to cost savings and environmental sustainability.
Conclusion
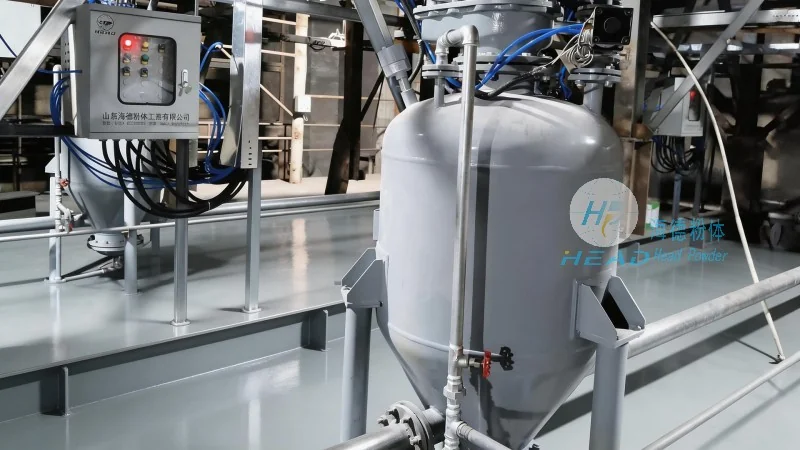
HeadPowder's nitrogen-protected powder pneumatic conveying systems represent a sophisticated solution for industries requiring precise control over powder handling. By leveraging nitrogen gas as a protective medium, these systems ensure the integrity of sensitive materials while delivering high conveying efficiency and operational reliability. With a strong presence in Shandong, China, HeadPowder continues to innovate and provide tailored solutions that meet the evolving needs of various industries. The combination of advanced technology and robust design makes these systems a preferred choice for businesses seeking to enhance their material handling processes and maintain product quality.




