HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced material handling solutions. The air-driven conveying system for nickel sulfate crystalline powder is a critical component in industrial processes that require efficient and reliable transport of this specific chemical. This system is engineered to handle the unique properties of nickel sulfate, ensuring optimal performance in various applications.
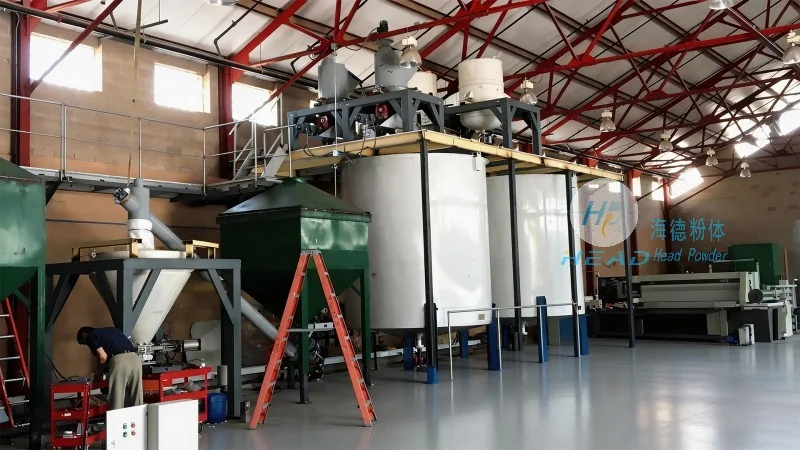
Company Overview: HeadPowder Engineering
HeadPowder Engineering Co., Ltd. is a professional enterprise dedicated to providing high-quality material handling equipment. With a focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the chemical and industrial sectors. The company’s headquarters is located in Shandong, China, where it leverages local resources and expertise to develop cutting-edge solutions for its clients. HeadPowder’s commitment to quality and reliability is reflected in its products, which are designed to meet the stringent requirements of modern industrial operations.
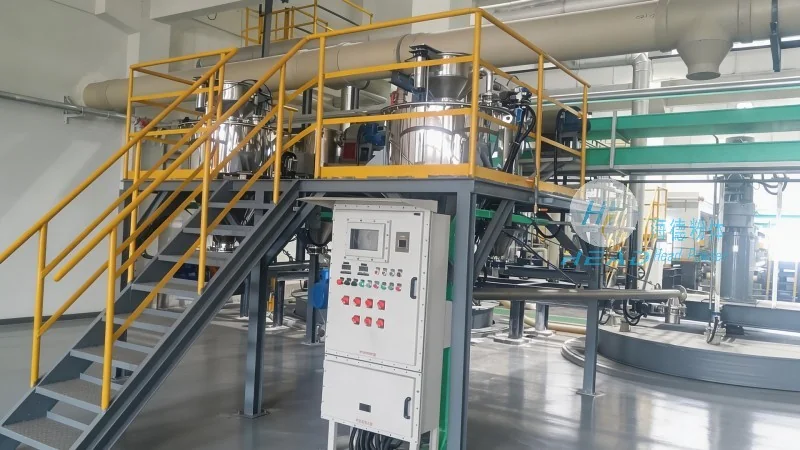
Understanding the Air-Driven Conveying System
The air-driven conveying system for nickel sulfate crystalline powder is a pneumatic system that utilizes compressed air to transport dry powders through a network of pipes. This method is particularly suitable for materials like nickel sulfate, which are prone to dust generation and require controlled handling to prevent contamination and loss. The system operates by creating a pressure differential between the inlet and outlet of the conveying line, allowing the powder to be drawn or pushed through the system. This approach eliminates the need for mechanical components like belts or buckets, reducing maintenance costs and improving overall efficiency.
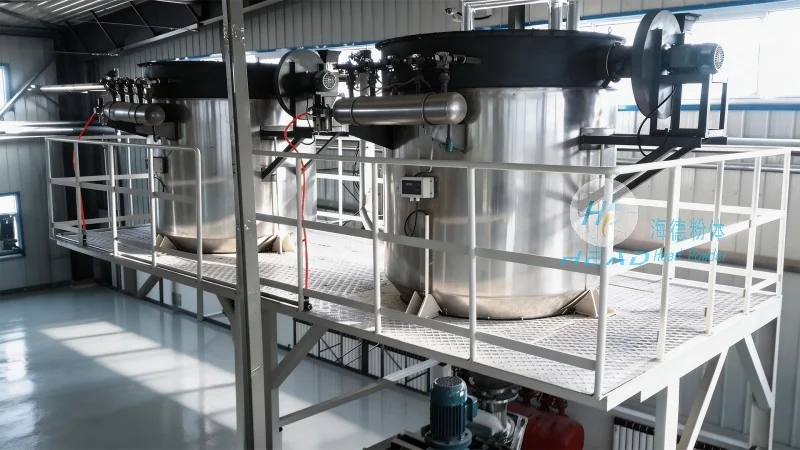
Working Principle of the System
The working principle of the air-driven conveying system involves several key steps. First, the nickel sulfate crystalline powder is fed into the inlet hopper of the system. The powder then falls into the conveying line, where it is mixed with the compressed air. The air, under pressure, propels the powder through the pipeline. The system uses a combination of positive and negative pressure to control the flow rate and ensure consistent delivery. The design of the system includes features such as pulse jets and cyclone separators to maintain the quality of the powder and prevent blockages. The control system monitors the pressure and flow rates, adjusting them as needed to maintain optimal performance. This automated control ensures that the system operates efficiently and safely, minimizing downtime and maximizing productivity.
Key Features of the Air-Driven Conveying System
The air-driven conveying system for nickel sulfate crystalline powder offers several advantages over traditional mechanical conveying methods. One of the primary features is its ability to handle fine powders without causing agglomeration or segregation. The system’s design minimizes the risk of dust exposure, which is crucial for maintaining a safe working environment. Another key feature is its flexibility, as the system can be easily integrated into existing production lines. The compact design of the equipment allows for installation in limited spaces, making it suitable for various industrial settings. Additionally, the system is energy-efficient, as it uses compressed air, which is a cost-effective and readily available resource. The low maintenance requirements of the system further contribute to its cost-effectiveness, as it reduces the need for frequent repairs and replacements.
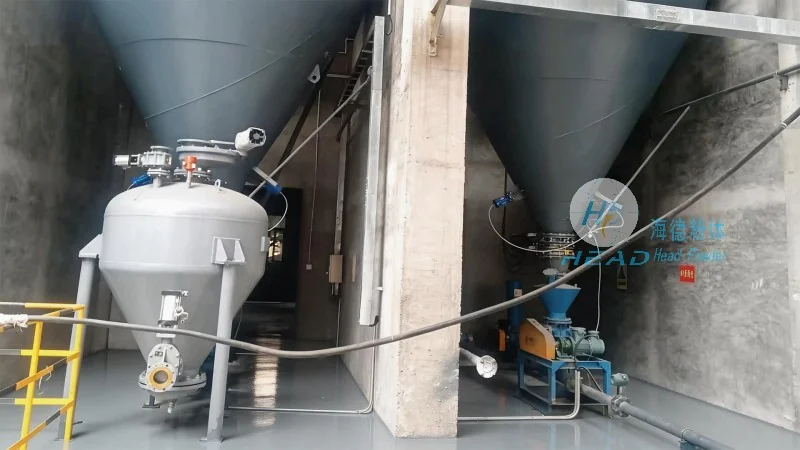
Application and Benefits
The air-driven conveying system is widely used in the chemical industry, particularly in the production of nickel sulfate. It is also applicable in other industries where fine powders need to be transported, such as pharmaceuticals and food processing. The system’s ability to maintain the purity of the powder is a significant benefit, as it prevents contamination from external sources. This is especially important in the production of high-purity chemicals, where even small amounts of impurities can affect the quality of the final product. The system also improves safety by reducing the need for manual handling of powders, which can be hazardous. Furthermore, the system enhances productivity by providing a continuous and reliable flow of material, which helps to streamline production processes and reduce bottlenecks.




