Pharmaceutical pneumatic conveying systems represent a critical technology in the pharmaceutical industry, offering a reliable and advanced method for transporting bulk materials. This approach not only enhances operational efficiency but also aligns with modern environmental standards, making it a preferred choice for manufacturers seeking to optimize their material handling processes while minimizing ecological impact.
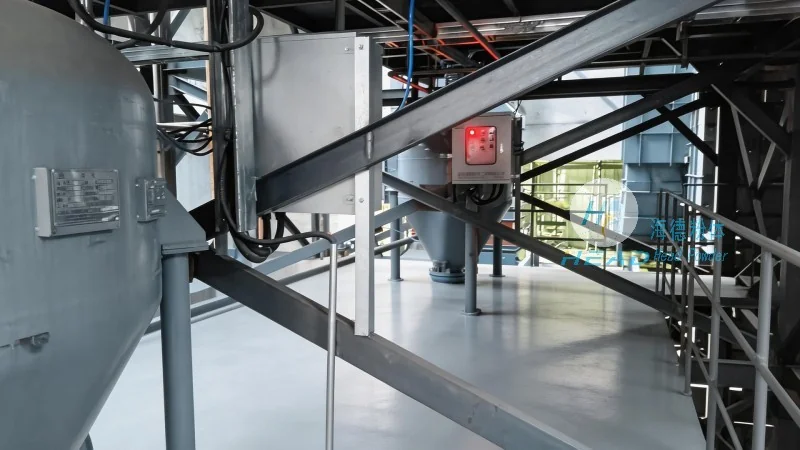
About HeadPowder: Leading the Way in Pharmaceutical Pneumatic Conveying
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a prominent provider of specialized engineering solutions tailored for the pharmaceutical sector. With headquarters located in Shandong, China, the company has established itself as a trusted partner in delivering high-quality pneumatic conveying systems that meet stringent industry requirements. HeadPowder’s commitment to innovation and precision engineering ensures that their products are designed to enhance productivity and safety in pharmaceutical manufacturing environments.
Key Features and Benefits of Pharmaceutical Pneumatic Conveying Systems
Pharmaceutical pneumatic conveying systems utilize air to transport powders and granules, eliminating the need for mechanical components like belts or chains. This design significantly reduces the risk of contamination and cross-contamination, which is paramount in pharmaceutical applications where product purity and safety are non-negotiable. The systems are engineered to handle a wide range of materials, including sensitive powders and active pharmaceutical ingredients (APIs), ensuring that each particle is transported with minimal degradation or loss.
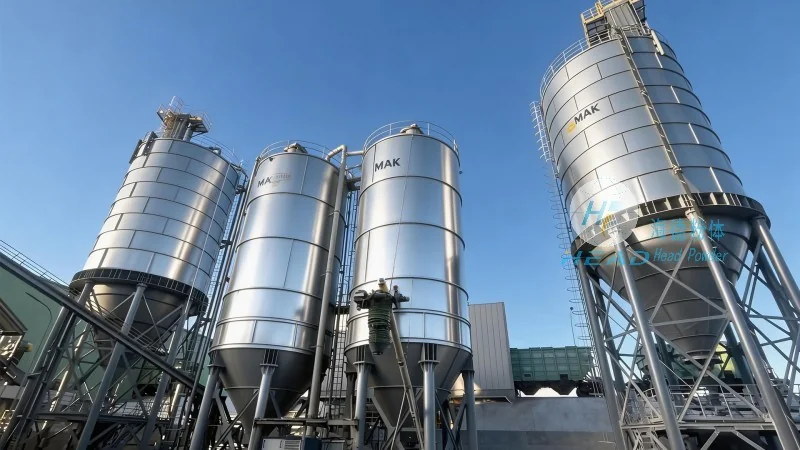
One of the most significant advantages of pneumatic conveying is its efficiency in terms of speed and throughput. These systems can process large volumes of material in a short period, improving overall production rates and reducing downtime. Additionally, the enclosed design of the conveying lines prevents dust and particles from escaping into the environment, contributing to a cleaner and safer working environment. This not only protects the health of employees but also helps in maintaining compliance with regulatory standards related to occupational health and safety.
Environmental Sustainability in Pharmaceutical Material Handling
From an environmental perspective, pharmaceutical pneumatic conveying systems offer substantial benefits. By using air as the primary transport medium, these systems eliminate the need for traditional bulk handling methods that often involve trucks or forklifts, which can contribute to air pollution and carbon emissions. The enclosed nature of the conveying lines also prevents dust from being released into the atmosphere, reducing the impact on local air quality. Furthermore, the energy efficiency of modern pneumatic conveying systems, particularly those equipped with advanced control technologies, helps in reducing overall operational costs while minimizing the carbon footprint of the manufacturing process.
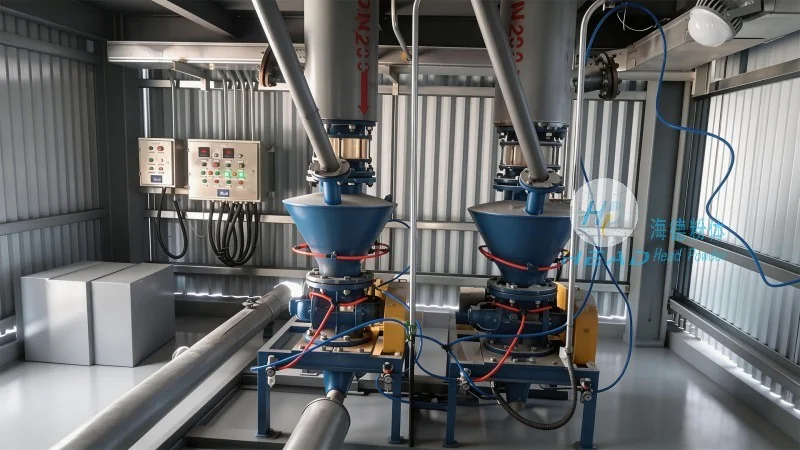
Applications in Pharmaceutical Manufacturing
Pharmaceutical pneumatic conveying systems are widely used in various stages of pharmaceutical production, from raw material handling to final product packaging. They are particularly effective in processes such as blending, mixing, and packaging, where the need for precise control over material flow is critical. The systems can be integrated into existing production lines, allowing for seamless transitions between different stages of manufacturing. This integration capability ensures that the overall production workflow remains smooth and efficient, with minimal disruptions.
Conclusion: Choosing HeadPowder for Your Pharmaceutical Conveying Needs
For pharmaceutical manufacturers seeking a reliable, efficient, and environmentally friendly material handling solution, HeadPowder offers a comprehensive range of pneumatic conveying systems. With a focus on quality, innovation, and customer satisfaction, the company provides tailored solutions that meet the unique needs of each client. By choosing HeadPowder, businesses can enhance their operational performance, ensure product safety, and contribute to a more sustainable future in the pharmaceutical industry.




