Working Principle and Features of Industrial Salt Material Handling Systems
Release time:2026-09-17 18:01:22
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
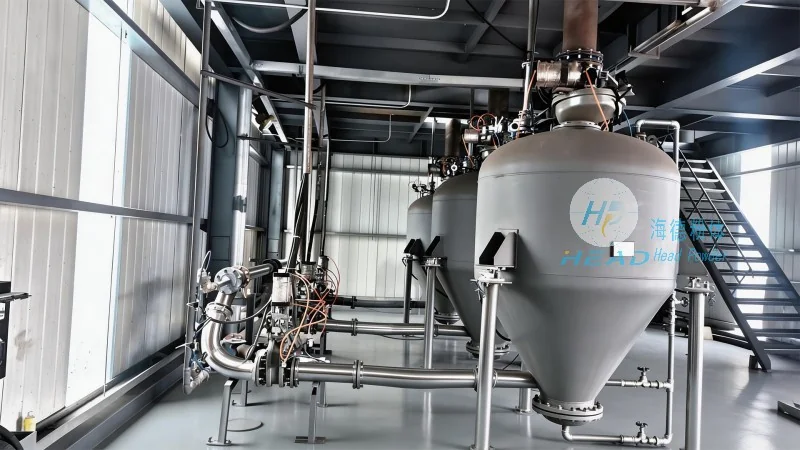
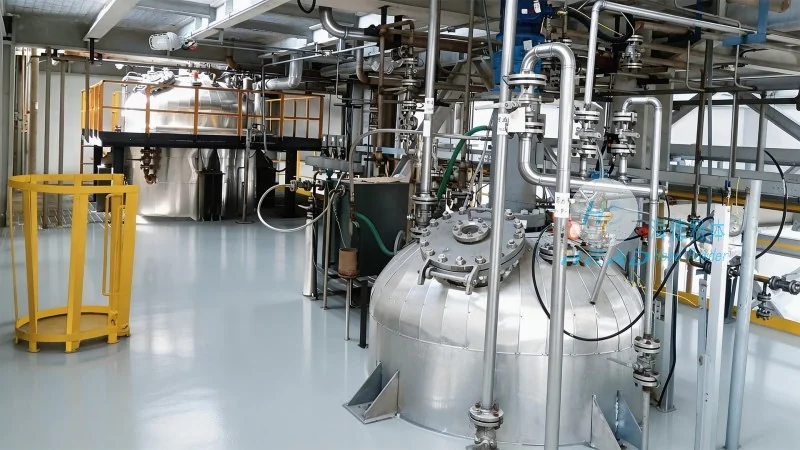
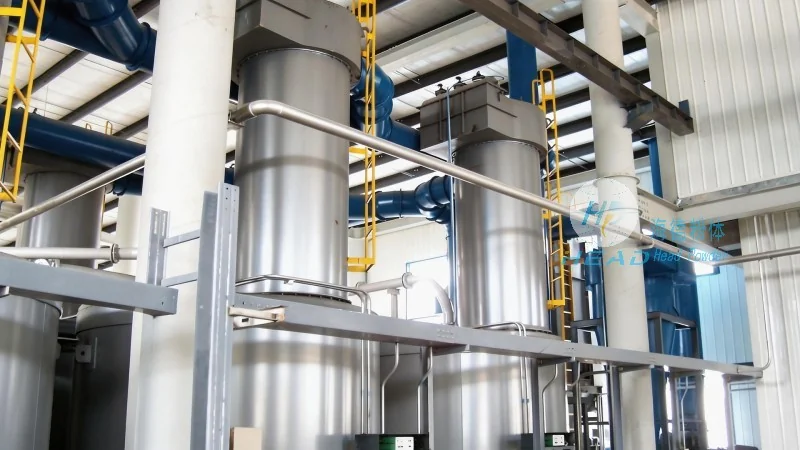
Industrial salt material handling systems are engineered to efficiently transport bulk industrial salt from storage silos or hoppers to processing or packaging facilities. The core working principle involves a coordinated set of mechanical components that ensure the smooth movement of the salt through the system. Typically, the process begins with the industrial salt stored in a large storage container, such as a silo or hopper. From this storage point, a conveyor system—often a belt conveyor or screw conveyor—takes over the task of transporting the salt. These conveyors are driven by electric motors that rotate rollers or screws, pulling the salt along the designated path. In some systems, additional components like vibrating feeders or bucket elevators are integrated to regulate the flow and maintain consistent movement. A central control unit monitors key parameters like flow rate, pressure, and temperature, allowing for real-time adjustments to optimize performance. This integrated approach ensures that the industrial salt is handled safely, efficiently, and with minimal downtime, aligning with the operational needs of industrial salt processing facilities.
Key Features of Industrial Salt Material Handling Systems
Industrial salt material handling systems from Shandong HeadPowder Engineering Co., Ltd. are designed with several critical features that enhance their performance and longevity. One primary feature is the use of corrosion-resistant materials in the construction of conveyor components. Given that industrial salt is a corrosive substance, the system incorporates materials like stainless steel or specialized coatings to prevent degradation over time. Another notable feature is adjustable speed control, which enables operators to modify the conveyor speed based on processing requirements. This flexibility allows the system to handle varying loads and production rates without compromising efficiency. Safety features, including emergency stop buttons and overload protection, are also integrated to prevent accidents and equipment damage. The modular design of the systems facilitates easy maintenance and upgrades, reducing overall ownership costs. By combining these features, the industrial salt material handling systems provide consistent performance, durability, and reliability, making them a trusted solution for industrial salt handling applications.
Efficiency and Reliability in Industrial Salt Processing
The industrial salt material handling systems are optimized for high efficiency and reliability, essential for industrial operations. The systems are engineered to handle large volumes of industrial salt with minimal energy consumption, thereby reducing operational costs. Advanced control systems provide real-time monitoring of key parameters such as flow rate and temperature, allowing for immediate adjustments to maintain optimal performance. Robust components, including durable conveyor belts and high-efficiency motors, are used to withstand harsh conditions, ensuring long-term operation. Proactive maintenance schedules and diagnostic tools help identify potential issues before they escalate, minimizing downtime. The combination of these elements results in a system that is both efficient and reliable, delivering consistent throughput and reducing the total cost of ownership. For industrial salt processing facilities, these systems represent a reliable investment that meets the demanding requirements of modern industrial operations.




