Understanding the working principle and characteristics of fertilizer granular material conveying is crucial for optimizing material handling processes in agricultural and industrial applications. This article provides a detailed overview of the mechanisms involved and the key attributes that define effective conveying systems for fertilizer granules.
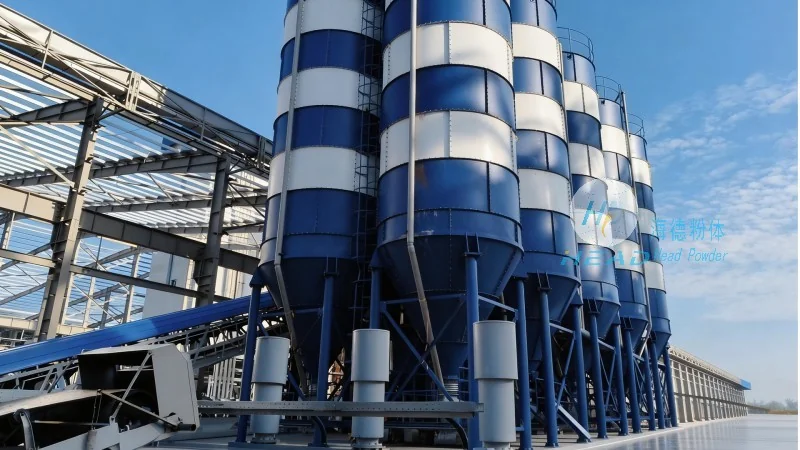
Working Principle of Fertilizer Granular Material Conveying
The process of conveying fertilizer granular materials typically involves several interconnected components designed to move bulk materials from one location to another efficiently. A common approach is the use of mechanical conveying systems, such as screw conveyors or belt conveyors, which rely on mechanical force to transport the material. In screw conveyors, a rotating helical screw inside a trough pushes the granules forward, ensuring consistent and controlled movement. This method is particularly effective for handling dry, free-flowing granular fertilizers, as it minimizes material degradation and maintains product integrity.
Another widely used method is pneumatic conveying, which utilizes air or gas to transport the material through a pipeline. This system consists of a blower, a hopper for material storage, and a pipeline network. The material is drawn into the pipeline by the air flow, and the pressure or vacuum created facilitates movement. Pneumatic conveying offers advantages like high capacity, flexibility in layout, and the ability to transport materials over long distances without the need for multiple transfer points. However, it requires careful control of air pressure and flow rates to prevent material segregation or blockages.
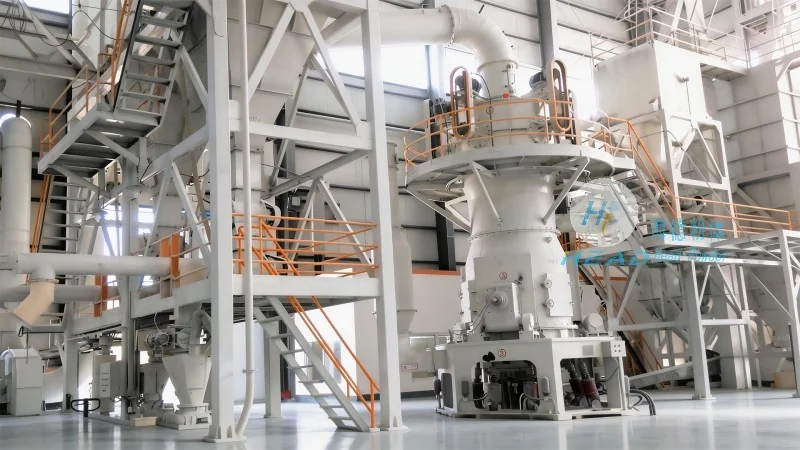
Hybrid systems, combining mechanical and pneumatic elements, are also employed in some applications. For instance, a screw conveyor may be used to feed material into a pneumatic conveying line, leveraging the strengths of both methods. This approach enhances efficiency by ensuring smooth material transfer from the initial loading point to the final discharge location.
Key Characteristics of Fertilizer Granular Material Conveying Systems
Effective fertilizer granular material conveying systems exhibit several distinct characteristics that contribute to their performance and reliability. One of the primary characteristics is high efficiency, which is achieved through optimized equipment design and operational parameters. Systems are engineered to minimize energy consumption while maximizing material throughput, making them suitable for large-scale agricultural operations.
Another important characteristic is environmental friendliness. Modern conveying systems often incorporate dust control measures, such as sealed hoppers and enclosed pipelines, to reduce airborne dust and minimize environmental impact. This is particularly critical in fertilizer handling, as dust can be a health hazard and contribute to air pollution. Additionally, some systems use low-noise components to reduce noise pollution, aligning with industrial standards for sustainable operations.
Adaptability is a third key characteristic. Fertilizer granular material conveying systems are designed to handle a wide range of granule sizes and types, from fine powders to coarse pellets. This flexibility allows them to accommodate different fertilizer formulations and production processes. Furthermore, systems can be customized to fit specific plant layouts, with modular components that can be easily reconfigured or expanded as production needs change.
Reliability and durability are also critical attributes. The equipment used in conveying systems, such as screw conveyors and pneumatic pipelines, is constructed from materials resistant to corrosion and wear, ensuring long service life. Regular maintenance and quality control measures are implemented to minimize downtime and ensure consistent performance. This reliability is essential for maintaining production schedules and meeting delivery commitments in agricultural supply chains.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized engineering solutions for material handling, particularly in the fertilizer industry. With a strong focus on innovation and customer-centric design, HeadPowder has established itself as a trusted partner for businesses seeking efficient and reliable conveying systems. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to develop cutting-edge technologies tailored to the needs of the agricultural sector.
HeadPowder's product portfolio includes a range of conveying equipment designed to meet the unique challenges of fertilizer granular material handling. These systems are engineered to enhance productivity, reduce operational costs, and ensure compliance with environmental regulations. The company's commitment to quality is reflected in its adherence to international standards and rigorous testing protocols, ensuring that each system meets the highest performance benchmarks.
Through continuous research and development, HeadPowder stays at the forefront of material handling technology, introducing new solutions that address emerging industry needs. The company's team of experienced engineers and technicians works closely with clients to understand their specific requirements, providing tailored solutions that optimize material flow and improve overall operational efficiency. This customer-focused approach has earned HeadPowder a reputation for excellence in the fertilizer conveying market.




