HeadPowder, a leading enterprise in the field of material handling solutions, specializes in the design, manufacturing, and implementation of systems tailored for the transportation of molybdenum oxide. This article delves into the working principles and distinctive features of such systems, providing an in-depth understanding of their functionality and advantages.
Working Principle of Molybdenum Oxide Material Handling Systems
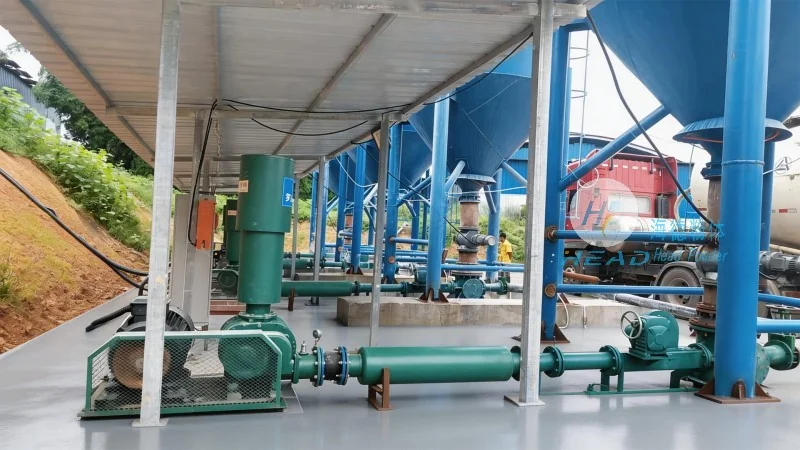
The core working principle of molybdenum oxide material handling systems revolves around the integration of advanced mechanical and control technologies to ensure efficient, safe, and reliable transportation of molybdenum oxide. These systems typically consist of several key components, including feeders, conveyors, storage silos, and control units. The process begins with the molybdenum oxide being fed into the system through a hopper or feeder, which regulates the flow rate to maintain consistent material movement. Subsequently, the material is transferred through conveyor belts, screw conveyors, or pneumatic systems, depending on the specific application and material characteristics. The control unit plays a crucial role in monitoring and adjusting the system parameters, such as speed, pressure, and temperature, to optimize performance and prevent issues like clogging or material degradation. Advanced sensors and automation technologies are often incorporated to enhance precision and safety, ensuring that the material is handled with minimal risk of contamination or damage.
Key Features of Molybdenum Oxide Material Handling Systems
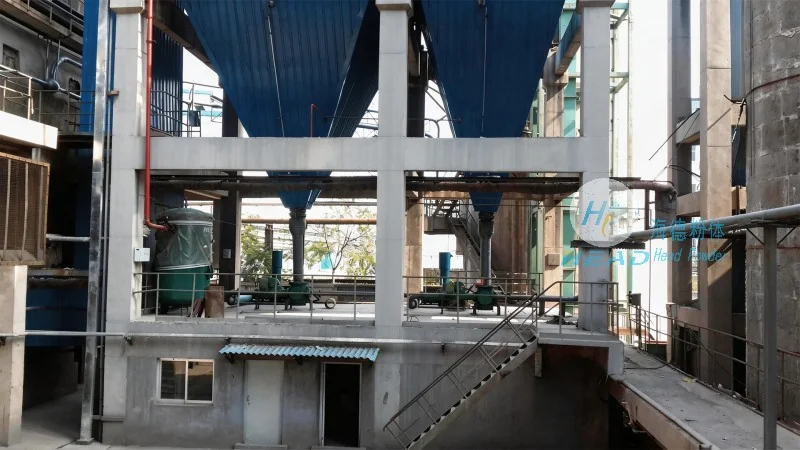
Molybdenum oxide material handling systems exhibit several notable features that make them suitable for industrial applications. Firstly, they are designed with high durability and corrosion resistance, as molybdenum oxide is a reactive material that requires specialized equipment to handle. The components, such as conveyors and storage vessels, are often constructed from stainless steel or other corrosion-resistant materials to prevent material degradation and ensure long-term operational reliability. Secondly, these systems are equipped with advanced control and monitoring capabilities, allowing for real-time tracking of material flow and system performance. This enables operators to quickly identify and address any issues, reducing downtime and improving overall efficiency. Thirdly, the systems are engineered for safety, incorporating features like overfill protection, emergency stop mechanisms, and dust suppression systems to minimize the risk of accidents and environmental contamination. Additionally, the modular design of many systems allows for easy customization and scalability, enabling businesses to adapt the system to changing production needs without significant modifications. The integration of energy-efficient technologies, such as variable frequency drives (VFDs), also contributes to reduced operational costs and environmental impact.
Application Scenarios and Benefits
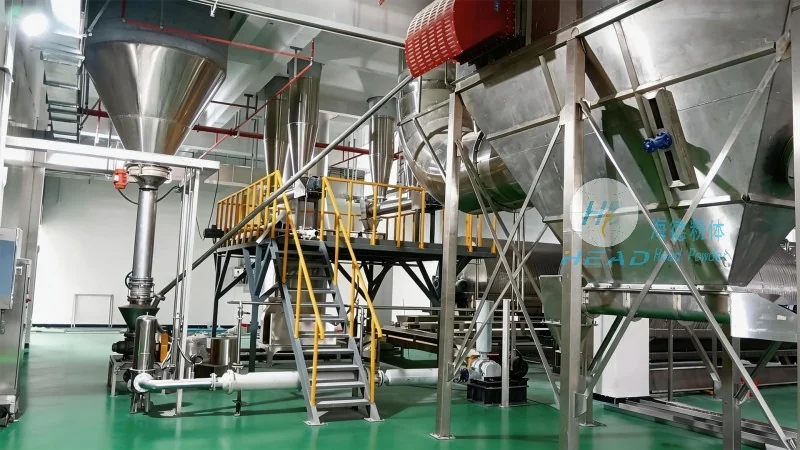
The applications of molybdenum oxide material handling systems span various industries, including chemical manufacturing, mining, and metallurgy. In chemical plants, these systems are used to transport molybdenum oxide for the production of molybdenum compounds, such as molybdenum disulfide and molybdenum trioxide. In mining operations, they facilitate the handling of molybdenum ore and its processing into oxide form. The benefits of implementing such systems include improved production efficiency, reduced labor costs, and enhanced safety for personnel. By automating the material handling process, businesses can achieve consistent material flow, minimize human error, and ensure compliance with safety regulations. Furthermore, the reliability of these systems contributes to higher product quality and reduced waste, as precise control over the material handling process prevents contamination and material loss. The scalability of the systems also allows companies to expand their operations as demand grows, without the need for extensive reconfiguration.
Company Profile and Expertise
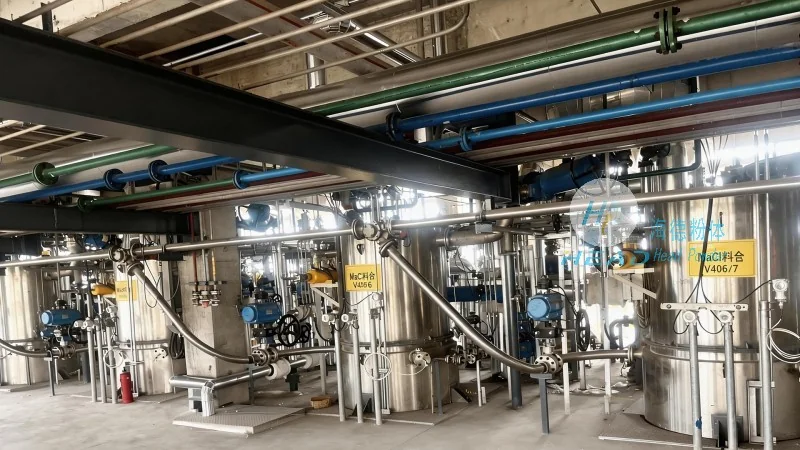
HeadPowder Engineering, based in Shandong, China, is a reputable manufacturer specializing in material handling solutions for various industrial applications. With years of experience in the industry, the company has developed a deep understanding of the unique challenges associated with handling molybdenum oxide and other specialized materials. The company's team of engineers and technicians is dedicated to designing and manufacturing high-quality systems that meet the specific needs of clients. HeadPowder's commitment to quality and innovation has earned it a strong reputation in the market, with clients relying on their expertise to optimize material handling processes. The company's facilities in Shandong are equipped with advanced manufacturing equipment and testing capabilities, ensuring that each system is thoroughly tested before delivery. This rigorous quality control process ensures that the systems perform reliably and meet the highest standards of safety and efficiency. HeadPowder's customer-centric approach involves working closely with clients to understand their requirements and provide tailored solutions that enhance their operational performance.




