High-pressure dense-phase powder conveyors are advanced industrial equipment designed for efficient and reliable transportation of bulk powders. This article provides an in-depth exploration of their working principle and key features, highlighting the technology's significance in modern material handling processes.
Company Introduction
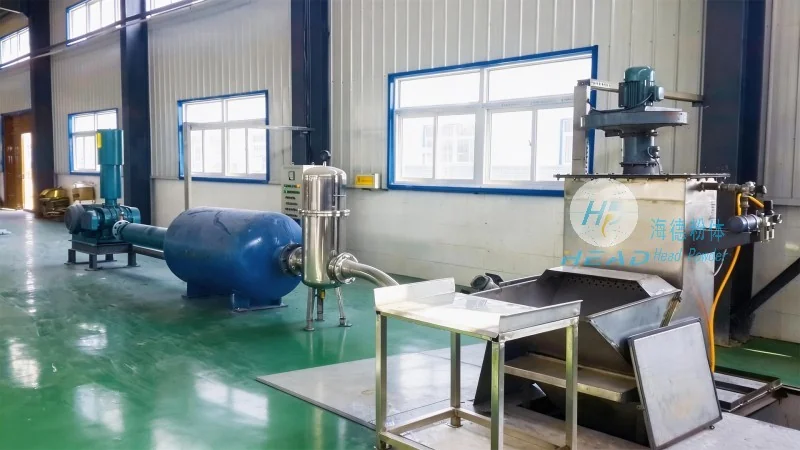
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer specializing in powder handling solutions. With a base in Shandong, China, the company focuses on delivering high-quality equipment tailored to the needs of various industries. HeadPowder's expertise lies in the design, development, and implementation of efficient powder transport systems, ensuring optimal performance and durability for clients worldwide.
Working Principle of High-Pressure Dense-Phase Powder Conveyors
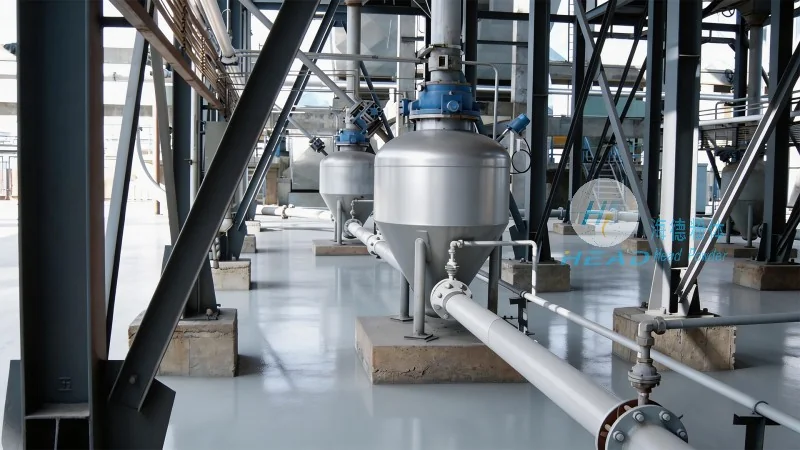
The operation of high-pressure dense-phase powder conveyors is based on a unique pneumatic conveying method that ensures the powder is transported in a dense phase, minimizing particle segregation and degradation. The system typically consists of a positive displacement blower or compressor that generates high-pressure air, which is then mixed with the powder in a hopper or feeder. As the air and powder mixture moves through the pipeline, the high pressure ensures that the powder particles are suspended in the air stream, forming a dense, homogenous flow. This dense-phase transport reduces the risk of material degradation, such as caking or agglomeration, and improves the overall efficiency of the conveying process. The process begins with the powder being fed into the system from a storage silo or hopper. The feeder, often a rotary valve or screw feeder, controls the flow rate of the powder into the pipeline. Simultaneously, the high-pressure air is introduced into the system, creating a mixture of air and powder. The mixture then travels through the pipeline, which may include bends, elbows, and other components, to reach the destination silo or processing unit. The pressure maintained throughout the system ensures that the powder remains in a dense phase, preventing it from settling or clogging the pipeline. The system also includes a pressure regulator and control valves to maintain consistent pressure and flow rates, ensuring smooth operation and preventing over-pressurization or under-pressurization that could affect performance.
Key Features of High-Pressure Dense-Phase Powder Conveyors
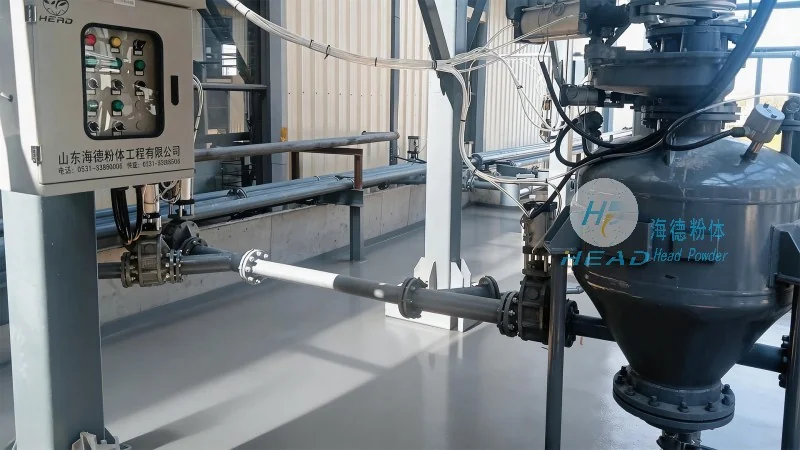
High-pressure dense-phase powder conveyors offer several advantages that make them ideal for transporting sensitive or abrasive powders. One of the primary features is the ability to maintain a dense phase, which reduces the risk of material degradation and ensures consistent product quality. The high-pressure operation also minimizes the risk of dust emissions, as the powder is contained within the pipeline and the system is designed to operate under positive pressure. Another key feature is the flexibility in conveying distances and heights, as the system can handle long pipelines and vertical lifts without significant loss of performance. The equipment is also designed for easy maintenance and cleaning, with features such as removable pipe sections and self-cleaning mechanisms that help prevent clogging and ensure long-term reliability. Additionally, the system can be integrated with other processing equipment, such as mixers or classifiers, to form a complete material handling system. The control systems are typically equipped with advanced sensors and monitoring tools that allow for real-time tracking of flow rates, pressure, and temperature, enabling operators to adjust the system parameters as needed to optimize performance. The durability of the components, such as the blower, pipeline, and valves, is another important feature, as they are constructed from materials resistant to corrosion and wear, ensuring long service life even in harsh operating conditions. The energy efficiency of the system is also a notable advantage, as the high-pressure operation minimizes the need for additional equipment and reduces energy consumption compared to other conveying methods.
Applications and Benefits
High-pressure dense-phase powder conveyors are widely used in various industries, including chemical, pharmaceutical, food, and mining. The technology is particularly suitable for transporting sensitive powders, such as pharmaceuticals or food ingredients, where product quality and purity are critical. The system's ability to maintain a dense phase ensures that the powder remains intact and free from contamination, making it ideal for applications where product integrity is paramount. In the chemical industry, the conveyors are used to transport raw materials and finished products, improving the efficiency of production lines and reducing downtime. The mining industry benefits from the system's ability to handle abrasive and heavy powders, such as ores and minerals, while minimizing the risk of equipment wear and tear. The food industry uses the conveyors for transporting ingredients like flour, sugar, and spices, ensuring that the products remain fresh and free from contamination. The benefits of using high-pressure dense-phase powder conveyors include increased production efficiency, reduced labor costs, and improved product quality. The system's ability to handle long distances and vertical lifts reduces the need for multiple transfer points, streamlining the material handling process and minimizing the risk of material loss or contamination. Additionally, the system's low maintenance requirements and long service life reduce operational costs and improve overall profitability for businesses.
Conclusion
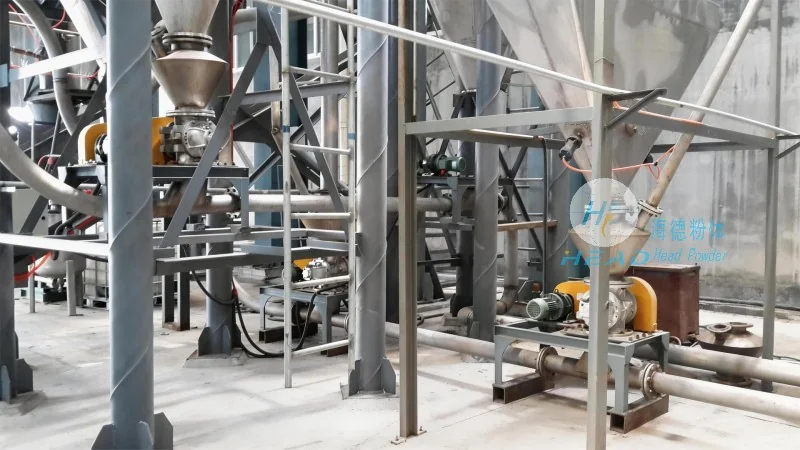
High-pressure dense-phase powder conveyors represent a significant advancement in powder handling technology, offering efficient, reliable, and cost-effective solutions for transporting bulk powders. The working principle, based on dense-phase pneumatic conveying, ensures minimal material degradation and consistent product quality. The key features, including high-pressure operation, flexibility, and durability, make the system suitable for a wide range of applications. HeadPowder, as a leading manufacturer, provides high-quality equipment that meets the needs of various industries, ensuring optimal performance and long-term reliability. By understanding the working principle and features of these conveyors, businesses can make informed decisions about implementing this technology to improve their material handling processes and enhance overall productivity.




