Ammonia fertilizer, as a crucial component in modern agricultural production, requires efficient and reliable transportation systems to ensure timely delivery to farms and processing facilities. The ammonia fertilizer pneumatic conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., offers an advanced solution for handling this specialized material with precision and safety. This system integrates cutting-edge technology to address the unique challenges associated with ammonia fertilizer, such as its corrosive nature and the need for controlled pressure and flow management.
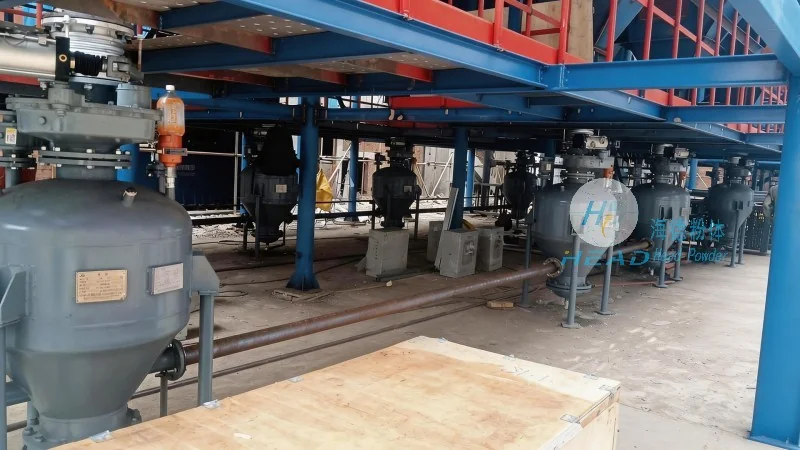
Working Principle of the Ammonia Fertilizer Pneumatic Conveying System
The working principle of the ammonia fertilizer pneumatic conveying system is based on the principle of air-assisted material transport. The system utilizes a series of components, including a hopper, rotary valve, air compressor, and conveying pipeline, to create a pressurized air flow that propels the ammonia fertilizer particles through the system. The hopper stores the ammonia fertilizer, and the rotary valve controls the flow of material into the conveying line. The air compressor generates the necessary pressure, which is then introduced into the pipeline via a venturi or pressure regulator. As the air flows through the pipeline, it entrains the fertilizer particles, forming a slurry-like mixture that is transported to the destination. The system can operate in both positive and negative pressure modes, depending on the application requirements. The positive pressure mode is typically used for long-distance or high-rise conveying, while the negative pressure mode is suitable for short-distance or horizontal transport. The control system monitors and adjusts the air pressure and flow rate in real-time to maintain optimal conveying efficiency and prevent material blockages or system failures.
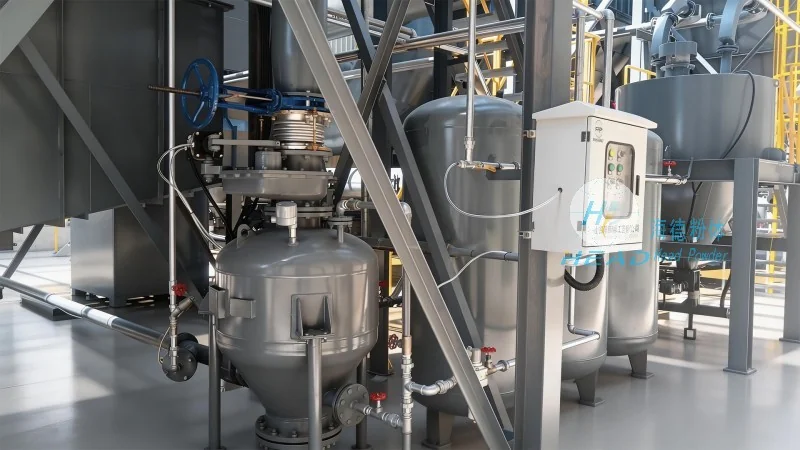
Key Features of the Ammonia Fertilizer Pneumatic Conveying System
Key features of the ammonia fertilizer pneumatic conveying system include high conveying efficiency, which allows for the transport of large quantities of ammonia fertilizer over significant distances with minimal energy consumption. The system is designed with corrosion-resistant materials, such as stainless steel and special coatings, to withstand the chemical properties of ammonia fertilizer and prevent equipment degradation. Safety is a top priority, with features like pressure relief valves, emergency shut-off mechanisms, and leak detection systems to ensure safe operation. The system also offers flexibility in terms of conveying capacity and speed, allowing it to adapt to varying production demands. Additionally, the modular design enables easy maintenance and replacement of components, reducing downtime and operational costs. The integration of advanced sensors and control technology provides real-time monitoring of system performance, enabling proactive maintenance and troubleshooting.
Technical Specifications and Application Scope
Technical specifications of the ammonia fertilizer pneumatic conveying system vary based on the specific application requirements. The system can handle different particle sizes and moisture contents of ammonia fertilizer, with typical conveying capacities ranging from 10 to 200 tons per hour. The maximum conveying distance can reach up to 500 meters, depending on the pipeline layout and pressure settings. The system operates under pressures ranging from 0.5 to 2.0 bar, with adjustable flow rates to match the production rate. Applications include transporting ammonia fertilizer from storage silos to blending facilities, from production lines to packaging units, and from farms to distribution centers. The system is also suitable for handling other corrosive materials, such as chemicals and powders, making it a versatile solution for various industrial sectors.
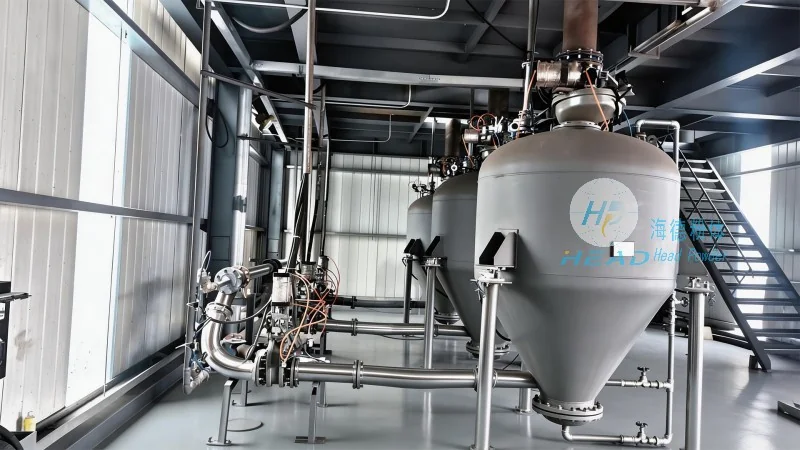
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of pneumatic conveying systems, specializes in providing customized solutions for the fertilizer and chemical industries. With a strong focus on research and development, the company has developed advanced technologies to enhance the efficiency and safety of material handling processes. The company's team of experienced engineers and technicians ensures that each system is designed and manufactured to meet the specific needs of clients, with attention to detail and quality control at every stage. HeadPowder's commitment to innovation and customer satisfaction has established it as a trusted partner in the industry, delivering reliable and efficient solutions for ammonia fertilizer transportation and other material handling applications. The company's facilities are located in Shandong, China, where it maintains a state-of-the-art production and testing center to ensure the highest standards of product quality.




