Soil pneumatic conveying systems represent a sophisticated approach to material handling, particularly in the context of transporting earthy materials like soil, sand, and other granular or fine particulate substances. These systems are engineered to move bulk materials through a network of pipes using compressed air or other gas streams, offering a dust-free, efficient, and flexible solution compared to traditional mechanical conveying methods. Understanding the working principle and key features of such equipment is crucial for industries that rely on consistent and reliable soil transportation, including construction, mining, and environmental remediation sectors.
Introduction to Soil Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, specializes in the design, manufacturing, and implementation of advanced soil pneumatic conveying systems. With a strong presence in China, particularly in Shandong province, the company has established itself as a leading provider of equipment tailored to the unique demands of soil and bulk material handling. The systems developed by HeadPowder are built on a foundation of robust engineering principles, ensuring durability, efficiency, and compliance with industry standards.
The Working Principle of Soil Pneumatic Conveying Equipment
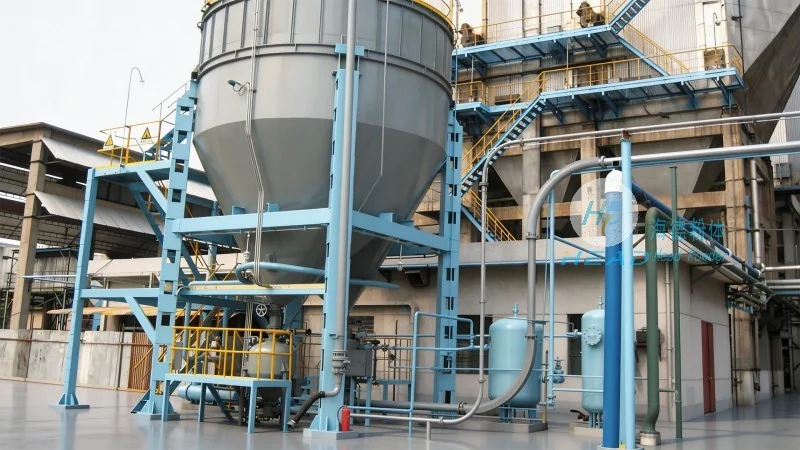
The core mechanism of soil pneumatic conveying systems revolves around the use of air pressure to transport materials. In a typical setup, the system comprises a hopper or feed hopper where the soil is loaded. A compressor then generates a high-pressure air stream that is introduced into the conveying line. As the air flows through the pipe, it creates a low-pressure zone that draws the soil particles into the air stream, forming a dense mixture known as a "pneumatic slurry." This mixture is then propelled through the pipeline to the discharge point, where the air is separated from the material, often using a cyclone separator or other air filtration equipment. The separated soil is collected in a receiving hopper or container, while the air is either recirculated or vented to the atmosphere, depending on the system design.
Key Features and Advantages of Soil Pneumatic Conveying Systems
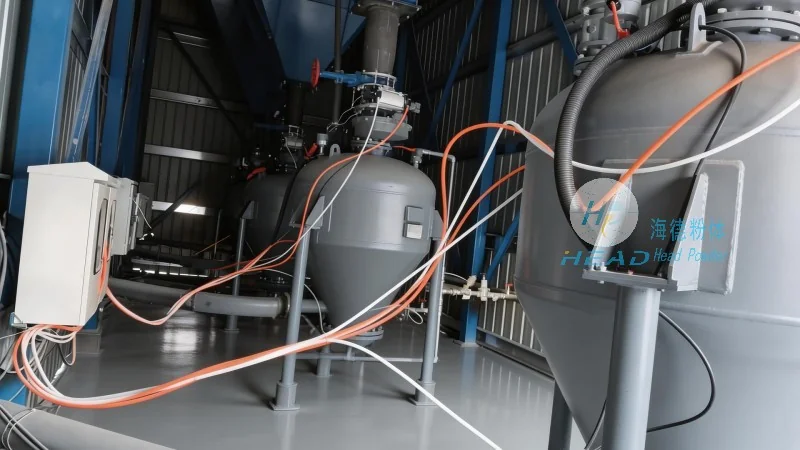
Soil pneumatic conveying systems, as offered by HeadPowder, exhibit several distinct features that make them advantageous for various applications. Firstly, they provide a dust-free operation, which is critical for maintaining air quality and worker safety in environments where fine soil particles are present. Unlike mechanical conveyors, which can generate significant dust and require additional dust control measures, pneumatic systems minimize airborne particulates, contributing to a cleaner working environment. Secondly, these systems offer high efficiency and flexibility in material transport. They can handle a wide range of soil types, from dry sand to moist clay, and can transport materials over long distances with minimal loss or degradation. The ability to adjust air pressure and flow rates allows for precise control over the conveying rate, ensuring optimal performance under varying load conditions.
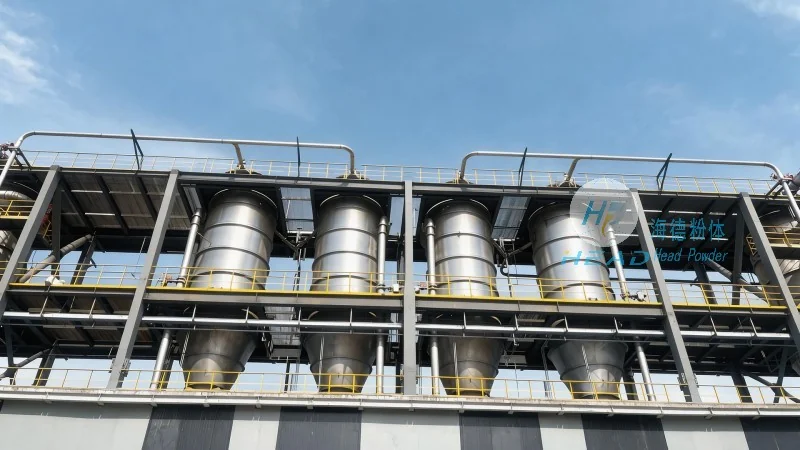
Another notable feature is the system's reliability and low maintenance requirements. Pneumatic conveying equipment typically has fewer moving parts compared to mechanical systems, reducing the likelihood of mechanical failures and the need for frequent maintenance. This translates into lower operational costs and increased uptime for users. Additionally, the systems are designed for easy integration into existing material handling workflows, allowing for seamless incorporation into construction sites, mining operations, or environmental remediation projects without significant disruptions.
Applications and Industry Impact
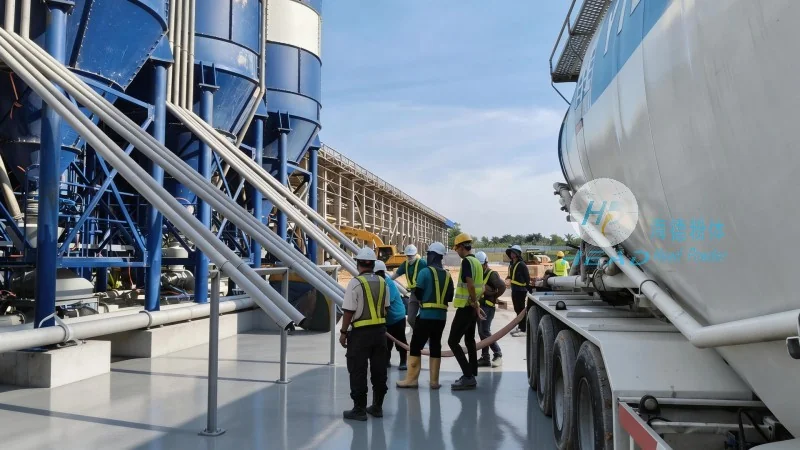
The versatility of soil pneumatic conveying systems makes them suitable for a variety of applications across different industries. In construction, they are widely used for transporting soil from excavation sites to disposal or reclamation areas, enabling efficient site management and material reuse. In mining operations, these systems facilitate the movement of earth materials from extraction sites to processing facilities, improving operational efficiency and reducing the environmental impact of material handling. Environmental remediation projects also benefit from these systems, as they allow for the safe and controlled transport of contaminated soil to treatment or disposal sites, ensuring compliance with environmental regulations.
By leveraging the advanced technology and engineering expertise of Shandong HeadPowder Engineering Co., Ltd., users can achieve reliable, efficient, and cost-effective soil transportation solutions. The company's commitment to quality and innovation ensures that their pneumatic conveying systems meet the highest standards of performance and durability, making them a trusted choice for industries that demand precision and reliability in material handling operations.




