

What is a Small Bag Loading Powder Pneumatic Conveying Machine? And What Are Its Design Principles?
For industrial applications requiring efficient and reliable powder handling, the small bag loading powder pneumatic conveying machine has emerged as a critical solution. This equipment is designed to transport bulk powders from storage bags or containers into processing systems, offering a seamless integration of material handling and process automation. In this article, we will explore the fundamental aspects of this technology, focusing on its operational design and the underlying principles that enable its effective performance.
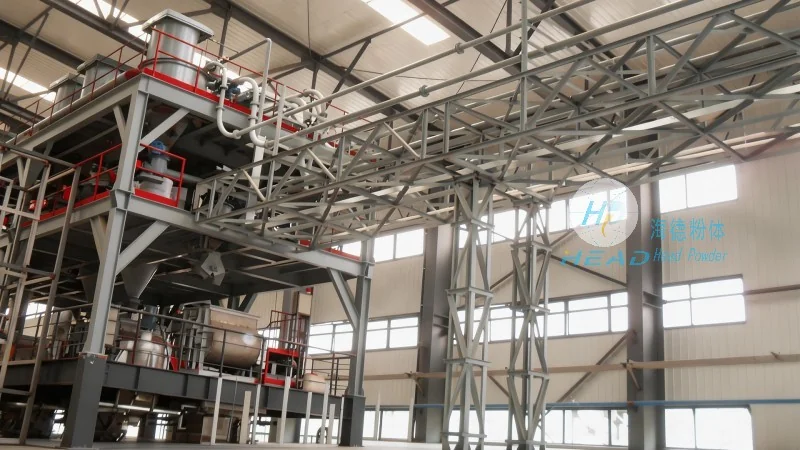
Understanding the Core Function of Small Bag Loading Powder Pneumatic Conveying Machines
The primary purpose of a small bag loading powder pneumatic conveying machine is to facilitate the transfer of dry powders from sealed bags or bulk containers into downstream processes such as mixing, blending, or packaging. Unlike traditional mechanical conveyors, this system utilizes compressed air to create a flow of material, eliminating the need for physical contact and reducing the risk of contamination or product degradation. The process typically involves the following steps: first, the compressed air is introduced into the bag or container, creating a pressure differential that forces the powder into a conveying line. The air then transports the powder through a network of pipes to the target destination, where it is discharged into the processing equipment. This method not only enhances operational efficiency but also ensures a consistent and controlled flow of material, which is essential for maintaining product quality and process stability.
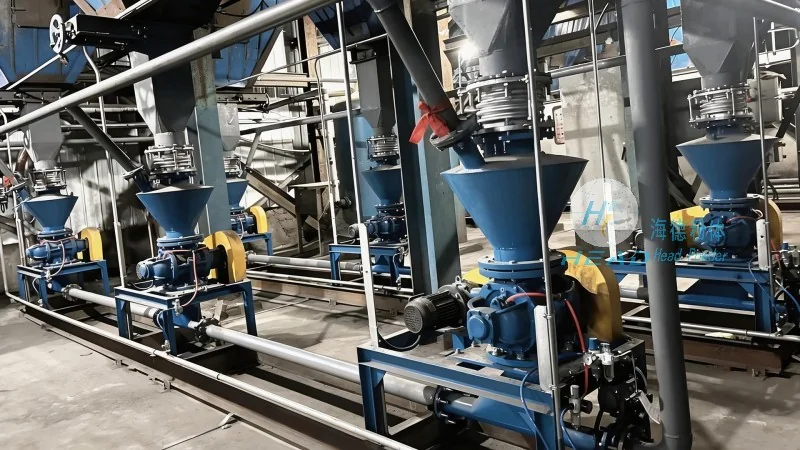
Key Design Principles Behind Small Bag Loading Powder Pneumatic Conveying Systems
The design of small bag loading powder pneumatic conveying machines is governed by several key principles that ensure optimal performance and reliability. One of the most critical factors is the selection of appropriate air pressure and flow rates, which directly impact the conveying capacity and efficiency of the system. Engineers must consider the particle size, density, and moisture content of the powder being handled, as these characteristics influence the air requirements for effective transport. Additionally, the system's design incorporates features such as airlocks, filters, and pressure regulators to maintain consistent air quality and prevent material blockages. The use of flexible hoses and robust piping materials is also essential to accommodate the dynamic nature of powder flow and to minimize wear and tear over time. Furthermore, the integration of safety features, such as pressure relief valves and dust collection systems, is a standard practice to ensure compliance with industrial safety regulations and to protect personnel and equipment from potential hazards.
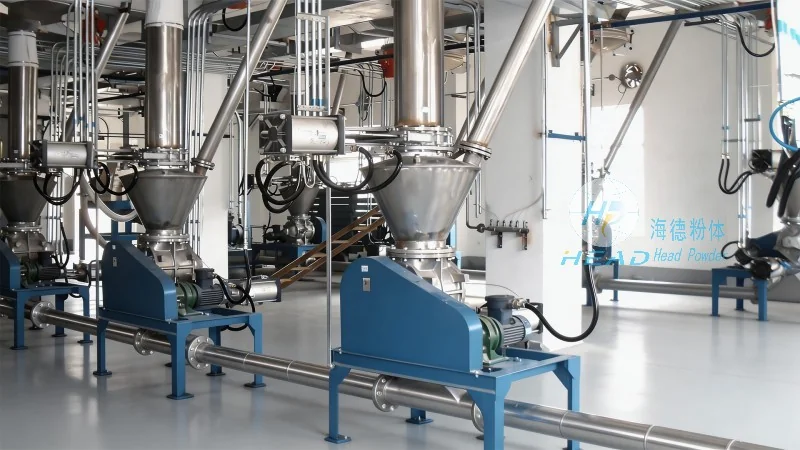
How Small Bag Loading Powder Pneumatic Conveying Machines Enhance Industrial Efficiency
By leveraging pneumatic technology, small bag loading powder conveying systems offer significant advantages over traditional methods. The ability to handle a wide range of powder types, from fine powders to coarse granules, makes this equipment versatile for various industrial applications. The automated nature of the process reduces labor costs and minimizes human error, leading to improved productivity and consistency in production. Moreover, the compact design of these machines allows for easy installation in existing facilities, making them a cost-effective solution for upgrading or expanding material handling capabilities. The system's ability to maintain a clean and controlled environment also contributes to better product quality and reduces the risk of cross-contamination, which is particularly important in industries such as pharmaceuticals, food processing, and chemical manufacturing.
Applications and Industries Benefiting from Small Bag Loading Powder Pneumatic Conveying Machines
The versatility of small bag loading powder pneumatic conveying machines makes them suitable for a wide array of industries. In the pharmaceutical sector, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that the final product meets stringent quality standards. The food industry benefits from the hygienic design of these machines, which prevents contamination and maintains the integrity of food powders. Similarly, in the chemical industry, the ability to handle corrosive or reactive powders safely is crucial, and the pneumatic conveying system provides an effective solution. Other industries that benefit include ceramics, plastics, and agricultural products, where efficient powder handling is essential for production efficiency and cost reduction.
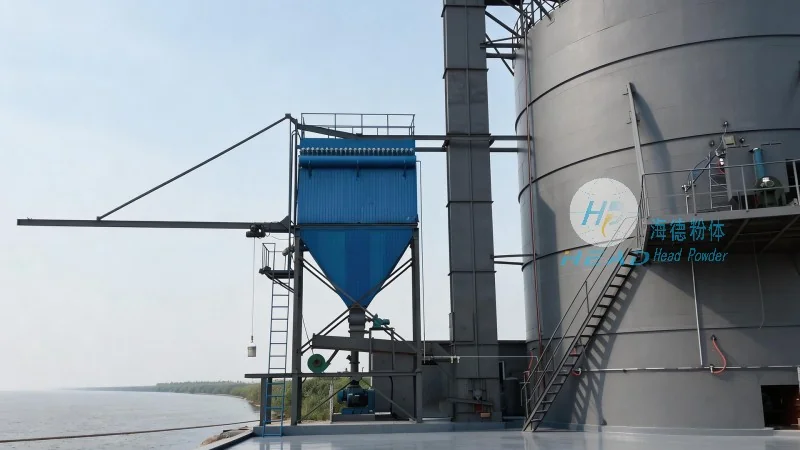
Conclusion: The Role of Small Bag Loading Powder Pneumatic Conveying Machines in Modern Manufacturing
In conclusion, small bag loading powder pneumatic conveying machines represent a sophisticated and efficient solution for the challenges of bulk powder handling in modern industrial settings. By combining advanced pneumatic technology with robust design principles, these systems offer a reliable and cost-effective method for transporting powders from storage to processing. The integration of safety features, adaptability to various powder types, and the ability to enhance overall production efficiency make them an indispensable asset for industries seeking to optimize their material handling processes. As manufacturing continues to evolve, the importance of such equipment in maintaining operational excellence and product quality will only grow, underscoring its critical role in the future of industrial production.