For industries dealing with bulk powder handling, efficient and reliable material transport is crucial. One advanced solution that has gained significant traction is the negative pressure dilute phase powder conveying system. This technology offers a robust method for transporting powders over long distances with minimal pressure drop and energy consumption. In this article, we will explore what these systems are and delve into their core design principles, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field.
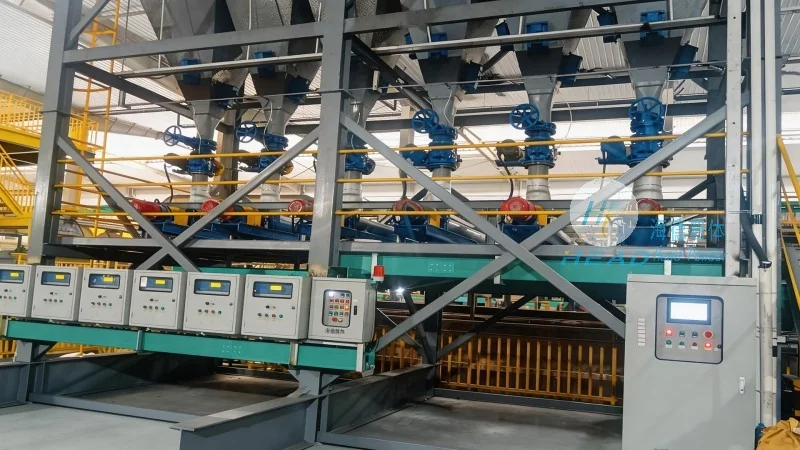
Introduction to Negative Pressure Dilute Phase Powder Conveying
The negative pressure dilute phase powder conveying system operates by creating a vacuum or negative pressure in the conveying line. This approach allows for the transport of powders in a dilute state, meaning the material is dispersed in a gas stream rather than being compacted or compressed. This method is particularly effective for handling fine powders, as it minimizes particle agglomeration and ensures consistent flow characteristics. The system typically consists of a suction hopper, a conveying pipe, a rotary airlock valve, and a dust collector, among other components. Each component plays a critical role in the overall efficiency and performance of the system.
Key Design Principles of Negative Pressure Dilute Phase Systems
The design of a negative pressure dilute phase powder conveying system is governed by several key principles that ensure optimal performance and reliability. First, the system must maintain a consistent negative pressure throughout the conveying line to prevent material backflow and ensure continuous transport. This is achieved through the use of a powerful vacuum pump or fan that generates the necessary suction force. Second, the conveying velocity must be carefully controlled to prevent particle deposition or blockage in the pipe. The velocity is typically maintained at a level that keeps the powder particles suspended in the gas stream without causing excessive wear on the system components. Third, the system design must consider the specific properties of the powder being conveyed, such as particle size, density, and moisture content. These properties influence the selection of the gas type (often air or a mixture of air and inert gas) and the required pressure drop across the system. Additionally, the system must incorporate proper filtration and dust collection mechanisms to comply with environmental regulations and maintain air quality.
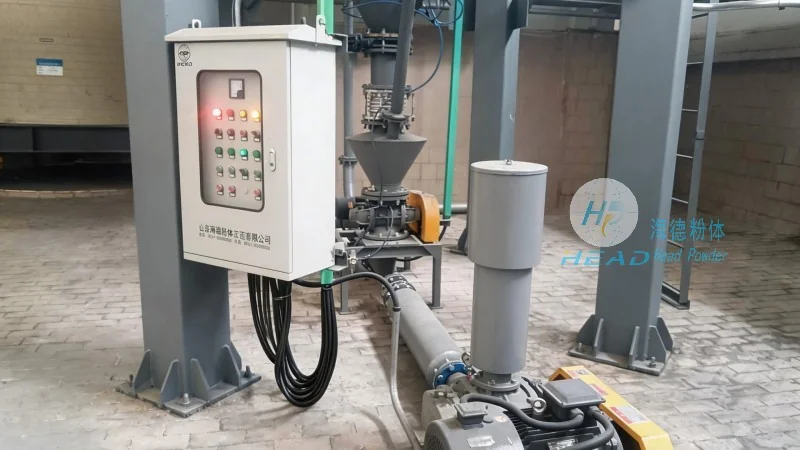
Components and Their Functions in the System
Each component of a negative pressure dilute phase powder conveying system is meticulously designed to contribute to the overall functionality. The suction hopper is the entry point where the powder is loaded and drawn into the system under vacuum. It is equipped with a feeding mechanism, such as a rotary valve or a screw feeder, to control the flow rate and prevent material bridging. The conveying pipe is usually made of corrosion-resistant materials like stainless steel or plastic, depending on the powder's chemical properties. The pipe diameter and length are optimized to minimize pressure loss while maintaining the required conveying velocity. The rotary airlock valve, located at the discharge end, acts as a seal to prevent air from entering the system and to control the discharge rate of the powder. This valve is designed to handle the negative pressure environment without leaking. Finally, the dust collector or filter system is essential for capturing any fine particles that may escape during the conveying process, ensuring compliance with air quality standards and protecting the environment.
Advantages of Negative Pressure Dilute Phase Conveying
Compared to other powder conveying methods, negative pressure dilute phase systems offer several advantages that make them a preferred choice for many industries. One of the primary benefits is the ability to transport powders over long distances with minimal energy consumption. The vacuum-based operation reduces the need for high-pressure pumps, resulting in lower operational costs. Additionally, the system is highly flexible, allowing for changes in the conveying route or material type without significant modifications. The dilute phase operation also minimizes the risk of material degradation or contamination, as the powder is not subjected to high pressures or temperatures. Furthermore, the system is relatively simple to install and maintain, with fewer moving parts compared to positive pressure systems. This simplicity translates to lower maintenance costs and increased system reliability over time.
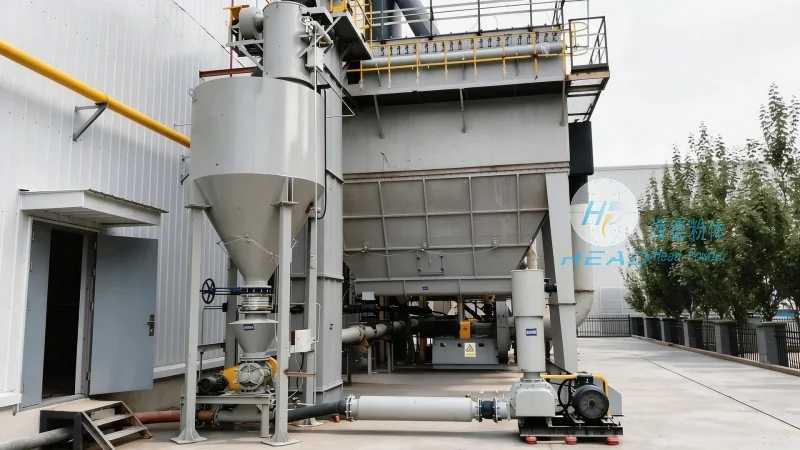
Applications and Industries
The negative pressure dilute phase powder conveying system is widely used in various industries where bulk powder handling is essential. In the pharmaceutical industry, these systems are used to transport raw materials and finished products with high precision and minimal contamination. The food industry utilizes them for conveying ingredients like flour, sugar, and spices, ensuring hygienic and efficient processing. The chemical industry relies on these systems for transporting powders such as catalysts, pigments, and specialty chemicals. Additionally, the mining and mineral processing industries use negative pressure systems to transport ore and other bulk materials from processing plants to storage or further processing facilities. The versatility of these systems makes them suitable for a wide range of applications, from small-scale laboratory operations to large-scale industrial production.
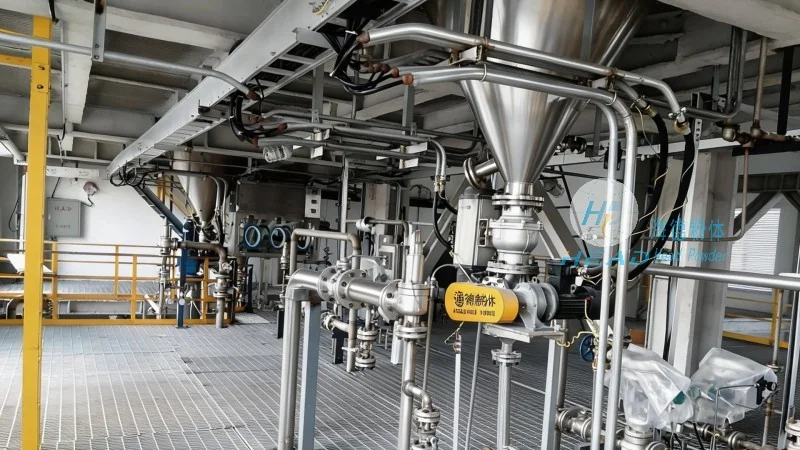
Role of Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of negative pressure dilute phase powder conveying systems. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for industries seeking reliable and efficient powder handling solutions. HeadPowder specializes in designing and manufacturing customized systems tailored to the specific needs of each client. The company's team of experienced engineers and technicians works closely with clients to understand their operational requirements and provide tailored solutions that meet their unique challenges. The company's facilities are equipped with advanced technology and stringent quality control measures to ensure that every system meets the highest standards of performance and durability. HeadPowder's products are known for their durability, efficiency, and low maintenance requirements, making them a preferred choice for industries that demand high reliability and cost-effectiveness.
Conclusion
Negative pressure dilute phase powder conveying systems represent a sophisticated and efficient solution for bulk powder transport. By understanding the design principles and components of these systems, industries can make informed decisions about their material handling needs. The expertise of companies like Shandong HeadPowder Engineering Co., Ltd. plays a crucial role in ensuring that these systems are designed and implemented effectively, delivering optimal performance and reliability. As industries continue to evolve and demand more efficient processing methods, negative pressure dilute phase systems will remain a vital component in the future of bulk material handling.




