Barley, a vital cereal grain used in brewing, animal feed, and various food products, requires efficient and reliable transportation methods to move from fields to processing facilities. The choice of transportation method depends on factors such as grain volume, distance, infrastructure availability, and cost-effectiveness. This article explores the primary methods used for barley transportation, highlighting their advantages and practical applications.
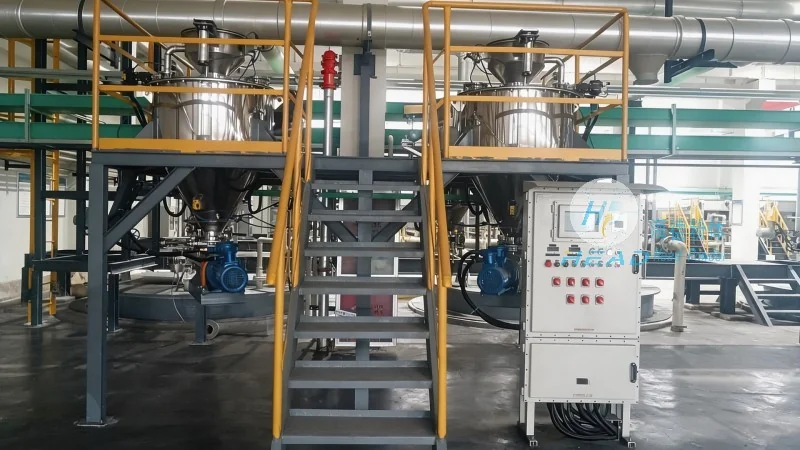
Understanding Barley Transportation: Key Methods and Considerations
Barley, a vital cereal grain used in brewing, animal feed, and various food products, requires efficient and reliable transportation methods to move from fields to processing facilities. The choice of transportation method depends on factors such as grain volume, distance, infrastructure availability, and cost-effectiveness. This article explores the primary methods used for barley transportation, highlighting their advantages and practical applications.
1. Mechanical Conveying Systems: Traditional and Robust Solutions
Mechanical conveying systems are among the most common methods for transporting barley. These systems utilize machinery like belt conveyors, screw conveyors, and bucket elevators to move grain vertically or horizontally. Belt conveyors, for instance, are ideal for long-distance horizontal transport, capable of handling large volumes of barley with minimal maintenance. Screw conveyors, on the other hand, excel in vertical or inclined transport, ensuring consistent flow and preventing grain spillage. These mechanical systems are particularly suitable for on-farm or short-distance transport, providing a cost-effective solution for farmers and small-scale processors.
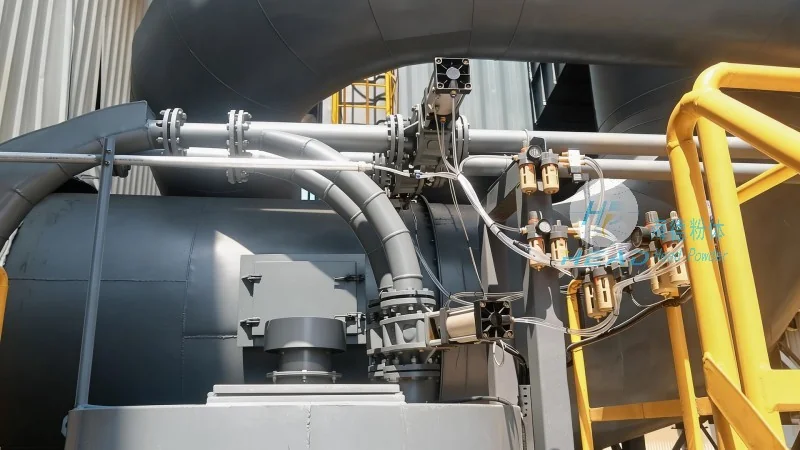
2. Gravity-Based Transport: Utilizing Natural Forces for Efficiency
Gravity-based transport methods leverage the natural weight of barley to move it between elevations or storage facilities. Chutes and hoppers are commonly used in this approach, allowing grain to flow downward under gravity. This method is simple, low-cost, and requires minimal energy, making it ideal for transporting barley from storage silos to processing lines. However, gravity systems are limited by the vertical drop and the need for proper slope design to ensure smooth flow. They are most effective when the grain is dry and free-flowing, avoiding issues like clogging or segregation.
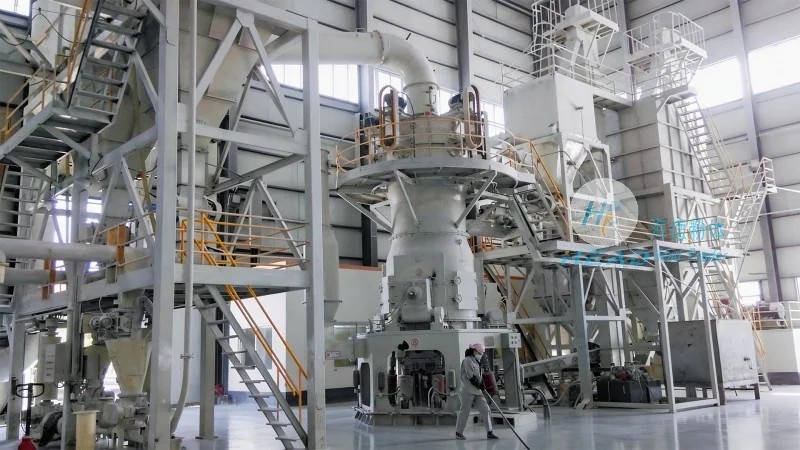
3. Pneumatic Conveying: High-Speed and Flexible Transport
Pneumatic conveying systems use air pressure to transport barley through pipes, offering a high-speed and flexible solution for both short and long distances. These systems can be categorized into positive and negative pressure types. Positive pressure systems blow air into the pipe, pushing the grain forward, while negative pressure systems create a vacuum to draw the grain. Pneumatic conveyors are particularly useful for transporting barley in processing plants, as they can handle fine or dusty grains without causing contamination. They are also suitable for transporting grain over obstacles or in complex layouts, making them a versatile choice for modern food and beverage operations.
4. Hydraulic Conveying: Heavy-Duty and Continuous Flow
Hydraulic conveying systems use water or a liquid medium to transport barley, providing a continuous and high-capacity flow. These systems are typically used in large-scale operations, such as grain elevators and processing plants, where high volumes of barley need to be moved efficiently. Hydraulic conveyors can handle wet or sticky barley, preventing clogging and ensuring consistent throughput. However, they require significant infrastructure and maintenance, as the system involves pumps, pipes, and water treatment facilities. This method is most effective when the processing facility has access to a reliable water supply and the necessary equipment for managing the liquid medium.
Shandong HeadPowder Engineering Co., Ltd.: Expertise in Barley Handling Solutions
For businesses seeking reliable and efficient barley transportation solutions, Shandong HeadPowder Engineering Co., Ltd. offers specialized equipment and systems tailored to specific needs. With years of experience in the grain handling industry, HeadPowder provides a range of mechanical, pneumatic, and hydraulic conveying systems designed to optimize barley transport. The company’s products are engineered to ensure minimal grain loss, maintain grain quality, and comply with industry standards. HeadPowder’s team of experts works closely with clients to assess their unique requirements, from on-farm storage to industrial processing, ensuring the most suitable transportation method is implemented. Based in Shandong, China, HeadPowder leverages local expertise and resources to deliver high-quality, cost-effective solutions for barley handling and transportation.




