HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of pneumatic conveying systems tailored for the safe and efficient bulk handling of sodium hydroxide. This article explores the application of pneumatic conveying technology in managing sodium hydroxide, a critical chemical widely used in various industrial processes.
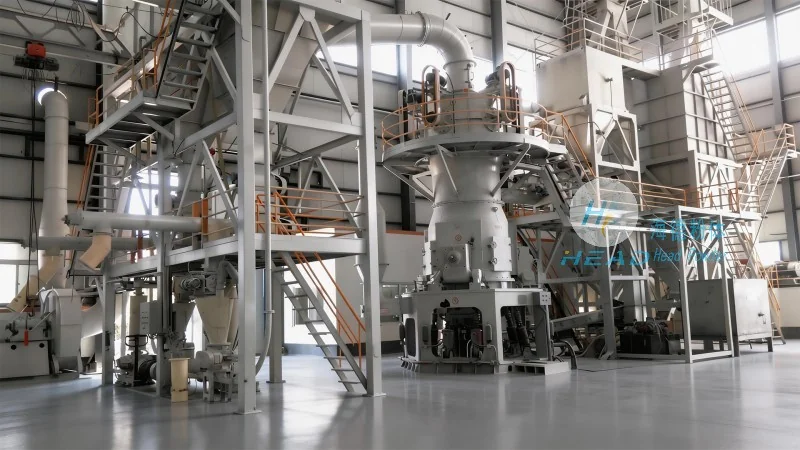
Understanding Sodium Hydroxide and Its Handling Challenges
Sodium hydroxide, commonly known as caustic soda, is a strong alkaline chemical with diverse industrial applications, including chemical manufacturing, paper production, and water treatment. Its bulk handling requires specialized equipment due to its reactive nature and potential hazards during transportation. Traditional methods like belt conveyors or trucks may pose risks such as dust exposure, material degradation, or spillage, making pneumatic conveying an ideal solution for safe and efficient transport.
Pneumatic Conveying Technology for Sodium Hydroxide
HeadPowder’s pneumatic conveying systems utilize air or gas to transport sodium hydroxide from storage silos to processing units. These systems are engineered to handle the chemical’s properties, ensuring minimal exposure to the environment and personnel. The technology offers several advantages, including reduced labor costs, improved safety, and enhanced material quality. By using positive or negative pressure systems, the equipment can transport sodium hydroxide over long distances with minimal maintenance requirements.
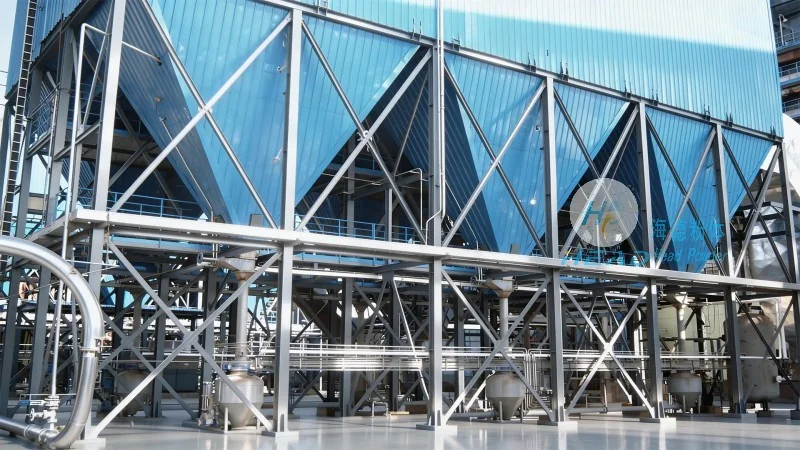
Key Features of HeadPowder’s Pneumatic Conveying Solutions
HeadPowder’s solutions are designed with precision to meet the unique demands of sodium hydroxide handling. Key features include corrosion-resistant materials, such as stainless steel, to withstand the chemical’s alkaline properties. The systems are equipped with advanced control mechanisms that monitor pressure, flow rates, and temperature, ensuring optimal performance and safety. Additionally, the company’s expertise in system integration allows for seamless integration with existing industrial infrastructure, minimizing downtime during installation.
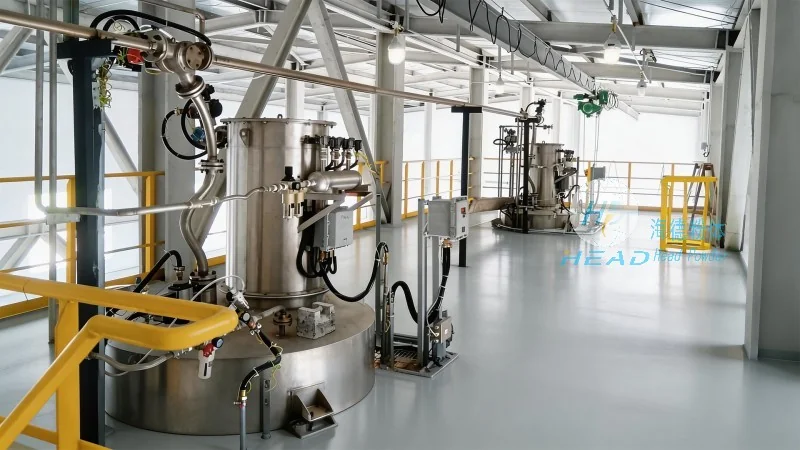
Applications and Benefits in Industrial Settings
In industrial settings, pneumatic conveying systems from HeadPowder enhance operational efficiency and safety. For example, in chemical plants, the technology enables the continuous transfer of sodium hydroxide from storage to reactors, reducing batch processing times and improving production throughput. The systems also contribute to environmental compliance by minimizing dust emissions and preventing material contamination. Furthermore, the low maintenance requirements of pneumatic conveying systems result in long-term cost savings for businesses.
Customization and Reliability
HeadPowder understands that each industrial application has unique requirements. Therefore, the company offers customized pneumatic conveying solutions tailored to specific needs, such as varying flow rates, distance, and material characteristics. The systems are built with high-quality components and undergo rigorous testing to ensure reliability and durability. With a strong focus on customer satisfaction, HeadPowder provides comprehensive support, including installation, training, and maintenance services, ensuring that clients can operate the systems efficiently and safely.




