For industrial applications involving the transport of fine powders, such as microparticle powders, efficient and reliable pneumatic conveying systems are essential. The design of such systems requires careful consideration of material properties, flow dynamics, and operational requirements to ensure optimal performance and minimal maintenance. This article provides an overview of the key components and design principles involved in the development of microparticle powder pneumatic conveying equipment, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. in this field.
Key Components of Microparticle Powder Pneumatic Conveying Systems
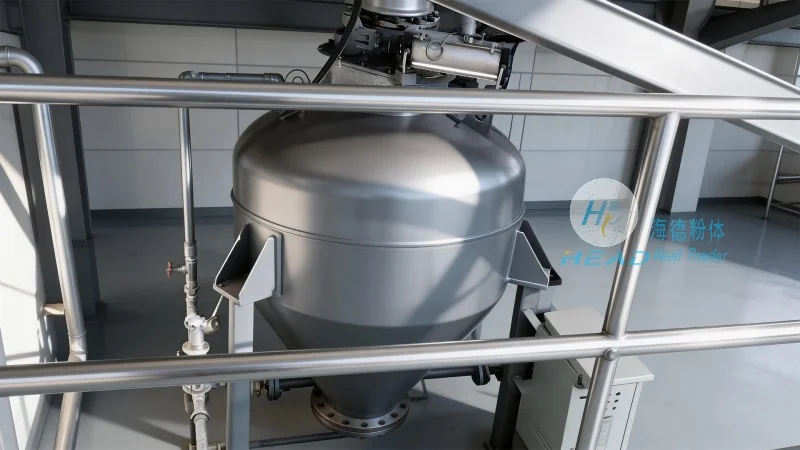
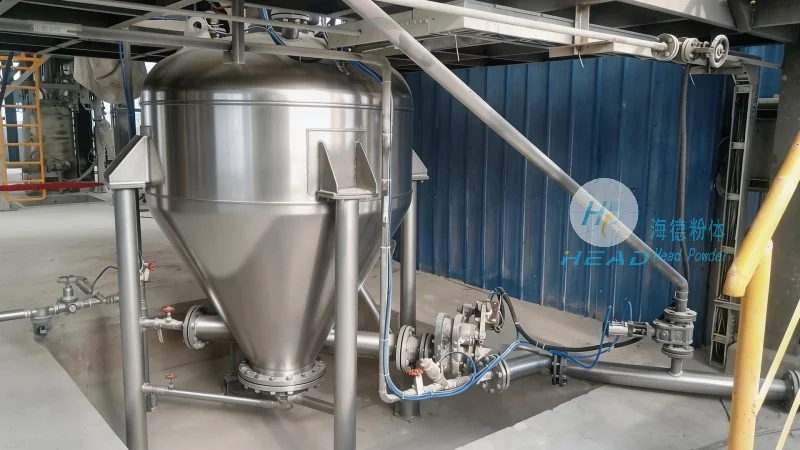
The core components of a microparticle powder pneumatic conveying system typically include a feeding mechanism, a conveying line, a separation unit, and a control system. The feeding mechanism is responsible for introducing the microparticle powder into the system, often using a rotary valve or a pressure feeder to maintain consistent flow rates. The conveying line, which may be made of stainless steel or other corrosion-resistant materials, transports the powder through the system under pressure. The separation unit, such as a cyclone or a bag filter, separates the powder from the air stream, ensuring that the powder is collected efficiently and the air is discharged safely. The control system monitors and regulates the pressure, flow rate, and other parameters to maintain stable operation.
Design Considerations for Microparticle Powder Handling
When designing a pneumatic conveying system for microparticle powders, several factors must be taken into account to prevent issues like blockages, agglomeration, and material degradation. The particle size, density, and moisture content of the microparticle powder are critical parameters that influence the choice of conveying method (e.g., dilute phase or dense phase) and the system's pressure requirements. For example, fine powders with high moisture content may require a dense phase system to avoid segregation and ensure uniform flow. Additionally, the system's design must consider the potential for particle attrition and wear on the conveying components, which can affect the overall lifespan and efficiency of the equipment.
Application Examples and Performance Metrics
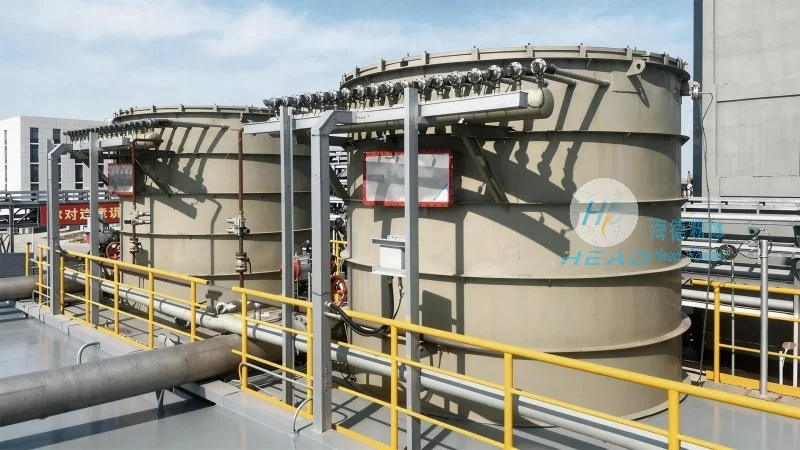
Microparticle powder pneumatic conveying systems are widely used in various industries, including pharmaceuticals, food processing, and chemical manufacturing. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high purity requirements, where contamination and particle size control are paramount. In food processing, they are used to convey ingredients like sugar, flour, and spices, where hygiene and product quality are critical. The performance of a pneumatic conveying system is typically evaluated based on metrics such as conveying capacity, pressure drop, and material recovery rate. A well-designed system should achieve high conveying efficiency while minimizing energy consumption and wear on components.
Expertise of Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design and manufacturing of advanced pneumatic conveying systems for microparticle powders. With years of experience in the industry, the company has developed a deep understanding of the unique challenges associated with handling fine powders and has developed innovative solutions to address them. The company's team of engineers and technicians work closely with clients to understand their specific requirements and provide customized solutions that meet their operational needs. By leveraging advanced design software and rigorous testing protocols, headpowder ensures that its pneumatic conveying systems are reliable, efficient, and compliant with industry standards.
Conclusion and Future Directions
The design of microparticle powder pneumatic conveying systems is a complex but essential process that requires a combination of technical expertise and practical experience. As industries continue to demand higher efficiency and reliability in powder handling, the importance of well-designed pneumatic conveying systems will only grow. Shandong HeadPowder Engineering Co., Ltd. remains committed to advancing the technology and providing high-quality solutions to meet the evolving needs of its clients. By focusing on innovation, quality, and customer satisfaction, the company is positioned to continue leading the industry in the development of advanced microparticle powder pneumatic conveying equipment.




